
CNC Machining 303 Stainless Steel for Precision Parts
Submit your drawing for CNC machining of 303 stainless steel, with DFM review, critical-dimension planning, and inspection requirements aligned before production.
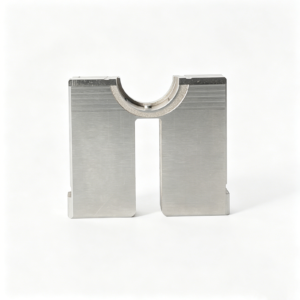
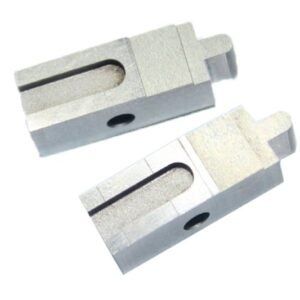
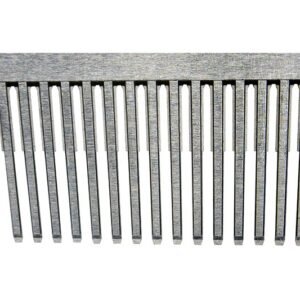
Representative Precision Components and Tooling Features





Related Drawing-Based Components




Why Choose CNC Machining 303 Stainless Steel
Use drawing-led process planning to balance chip control, feature access, critical dimensions, and inspection requirements before production.
Predictable Chip Control
303 stainless steel supports shorter chip formation, helping planners evaluate turning, milling, drilling, and thread-cutting routes around part geometry.
Feature Access Review
SUUXIANG reviews tool access, internal features, thin sections, and datum relationships to identify practical machining and fixturing considerations early.
Critical Dimension Planning
Drawings should identify critical dimensions, tolerance relationships, surface requirements, and functional interfaces so the process route can be evaluated responsibly.
EDM and Grinding Strategy
Where geometry or finish requirements warrant it, CNC operations can be coordinated with wire EDM, sinker EDM, or precision grinding.
Inspection Alignment
Agree inspection methods, reporting needs, and revision status before production so final documentation aligns with the order and verified plan.
Material Fit Discussion
Confirm corrosion exposure, mating conditions, welding needs, and application demands before selecting 303 stainless steel for a drawing-driven component.
303 Stainless Steel Part Families
Assess configurable CNC, mold, connector, and die-component families from drawings before process, inspection, and delivery requirements are committed.

CNC Machining Services
Precision CNC machining services for drawing-based custom parts, assessed around 303 stainless steel grade, critical dimensions, datum strategy, tool access, surface requirements, quantity, and inspection needs before quotation.
Upload a Drawing
CNC Milling
Custom CNC milling services for prismatic and contoured 303 stainless steel parts. Drawing review considers feature access, clamping strategy, corner geometry, tolerance stack, finishing allowance, and inspection points.
Upload a Drawing
CNC Turning
Precision CNC turning services for rotational 303 stainless steel components such as shafts, bushings, sleeves, threaded features, and locating elements. Quotations should define datums, concentricity, runout, surface finish, and mating requirements.
Upload a Drawing
5-Axis Machining
5-axis CNC machining for 303 stainless steel parts with angled features, compound surfaces, or limited tool access. Process planning evaluates setup reduction, tool reach, feature orientation, tolerance relationships, and inspection access.
Upload a Drawing
Swiss & Micro Machining
Swiss machining and micro machining for small 303 stainless steel turned parts with fine diameters, long length-to-diameter ratios, cross features, or tight functional interfaces. Review includes material form, deburring, handling, measurement, and lot requirements.
Upload a Drawing
Wire & Sinker EDM
Wire EDM and sinker EDM services for hardened or complex tooling features where conventional tool access is limited. Planning addresses wire path or electrode strategy, corner conditions, EDM allowance, recast-layer expectations, and finishing operations.
Upload a Drawing
Precision Grinding
Precision surface and profile grinding for 303 stainless steel parts requiring controlled flatness, parallelism, profile form, or surface condition. The drawing review confirms grinding stock, heat-treatment sequence, datum surfaces, and inspection method.
Upload a Drawing
Mold Core & Cavity Inserts
Precision mold core and cavity inserts produced from drawings for injection and related tooling applications. Review focuses on steel selection, cooling or vent features, shutoff geometry, EDM needs, fitting interfaces, and critical molded-part dimensions.
Upload a Drawing
Ejector & Ejection Components
Ejector pins, sleeves, and ejection components assessed for fit, stroke, guidance, hardness, wear conditions, lubrication, and mating surfaces. Drawings should identify critical diameters, clearances, and any surface or heat-treatment requirements.
Upload a Drawing
Core Pins, Guide & Locating Components
Core pins, guide pins, bushes, and locating components for repeatable mold alignment and functional positioning. Evaluation considers datum relationships, fit class, wear surfaces, retention method, material condition, and replacement or matching-part needs.
Upload a Drawing
Slides, Lifters, Gates & Mold Accessories
Mold slides, lifters, gates, and accessories manufactured as configurable tooling components rather than assumed catalog items. Drawings should clarify travel, shutoffs, sliding interfaces, cooling, wear treatment, assembly references, and fitting expectations.
Upload a Drawing
Connector Mold Components
Precision connector mold components for terminal cavities, inserts, pins, guides, and related tooling features. Process review emphasizes pitch, positional tolerances, fine details, EDM strategy, mating relationships, polishing needs, and inspection evidence.
Upload a Drawing
Stamping Die Components
Precision stamping die components including punches, dies, inserts, guide elements, and wear components. A viable process route depends on strip or forming context, cutting edges, clearance, material and hardness, grinding stock, and assembly datums.
Upload a Drawing
Injection, MIM, CIM & Overmolding Tooling
Injection, MIM, CIM, and overmolding tooling components assessed within verified production scope. Share molded-part geometry, material behavior, gate or runner requirements, insert interfaces, shrinkage assumptions, and quality priorities for informed DFM discussion.
Upload a Drawing
Machining Materials
CNC machining materials are selected against drawing requirements, application loads, corrosion exposure, machinability, heat-treatment sequence, and inspection needs. 303 stainless steel requirements should specify the applicable material standard, condition, and traceability expectations.
Upload a Drawing
Surface Finishes & Heat Treatment
Surface finishing and heat treatment are planned around functional surfaces, corrosion resistance, wear, dimensional change, and post-process inspection. Specify the required finish, treatment standard, masking or protected areas, and any hardness or appearance criteria.
Upload a Drawing
Quality, Metrology & Documentation
Precision inspection, metrology, and quality documentation aligned with the drawing and agreed inspection plan. Define critical dimensions, measurement method, sampling or reporting expectations, material records, revision level, and traceability requirements before production.
Upload a Drawing
Prototyping & Low-Volume Production
Rapid prototyping and low-volume manufacturing for drawing-driven parts where design validation, process learning, or controlled replenishment is needed. Submit quantity, revision status, material, critical features, delivery target, and required inspection documentation.
Upload a DrawingMaterials for CNC Machining 303 Stainless Steel

303 Stainless Steel
A free-machining austenitic grade suited to intricate turned and milled parts, fasteners, shafts, and fittings. Its sulfur addition supports chip control, while corrosion exposure and required material condition should be reviewed against the drawing.

304 Stainless Steel
A broadly used austenitic grade for parts requiring balanced corrosion resistance and general mechanical performance. For complex geometry, the drawing review should account for machining access, work-hardening behavior, finish requirements, and inspection datums.

316 Stainless Steel
An austenitic option often considered where the application requires stronger corrosion resistance than standard indoor-service grades. Its selection should be supported by the operating environment, specified condition, critical dimensions, and a feasible machining and inspection plan.

416 Stainless Steel
A martensitic stainless option for selected components where machinability and heat-treatment requirements influence material choice. Confirm the required hardness, pre- or post-machining heat-treatment sequence, grinding allowance, and dimensional reporting before production planning.
CNC Machining 303 Stainless Steel: Process Routes Evaluated

CNC Milling
CNC milling develops flats, pockets, profiles, holes, and datum features in 303 stainless steel. Tool access, clamping, wall geometry, and surface requirements are reviewed before selecting a machining sequence for the drawing.

CNC Turning
CNC turning supports rotational features such as shafts, threaded forms, bores, and stepped diameters. The route is assessed against datum relationships, runout requirements, stock condition, and any secondary milling or inspection needs.


EDM Processing
Wire EDM and sinker EDM are considered for narrow profiles, internal corners, difficult access, and precision mold-component geometry. Electrode or wire-path strategy, EDM allowance, and downstream finishing requirements are defined from the drawing.

Grinding And Inspection
Precision grinding, fitting, and inspection are planned when size, flatness, surface, or mating relationships require controlled finishing. The inspection method, critical dimensions, reporting needs, and revision status are aligned with the agreed order requirements.
CNC Machining 303 Stainless Steel: Tooling Accessories and Functional Features

Precision Core Pins
Core pins can support molding, locating, or ejector functions when diameter, engagement length, surface condition, and mating relationships are defined. Review should confirm machining access, grinding needs, and inspection points before production.

Guide Elements
Guide pins, bushes, and related alignment features help control repeatable movement between tooling components. Their fit, datum reference, lubrication provisions, and wear expectations should be stated so the process route can be evaluated.

Locating Features
Dowel holes, reference shoulders, keys, and locating faces establish repeatable assembly position. Dimension these features from functional datums and identify critical relationships, allowing machining and inspection planning to follow the intended assembly logic.

Threaded Interfaces
Tapped holes, threaded bores, and screw interfaces can be incorporated where the drawing identifies thread standard, class, depth, and mating purpose. Tool access, burr control, and any gauging requirement should be reviewed with the part.

Part Markings
Part numbers, revision marks, or orientation identifiers may be added when the drawing and production route support them. Define content, location, marking method, and cosmetic restrictions to protect traceability without compromising functional surfaces.
CNC Machining 303 Stainless Steel at SUUXIANG
SUUXIANG is the international-facing brand of Dongguan SuuXiang Precision Mold Co., Ltd., established in 2010 in Chang’an Town, Dongguan, Guangdong, China. Founded by XiaoCheng Huang, the company helps global engineering and sourcing teams turn drawings, models, material requirements, and inspection expectations into custom precision-manufacturing work.
Our practical scope combines CNC milling and turning, multi-axis machining, EDM, precision grinding, fitting, and inspection for custom machined parts, mold components, connector tooling, and die components. For cnc machining 303 stainless steel, process planning begins with the drawing rather than a generic material assumption.
What distinguishes SUUXIANG is a disciplined drawing-led workflow: DFM review, critical-dimension and datum discussion, machining-access assessment, revision control, and inspection planning before production commitments. Each project is evaluated against its own material, quantity, surface, delivery, and documentation requirements so the manufacturing route and final evidence remain aligned.

CNC Machining 303 Stainless Steel for Critical Dimensions
DFM and Datum Review
Before quoting cnc machining 303 stainless steel parts, SUUXIANG reviews drawing intent, datums, tolerance stack, tool access, surface requirements, and mating conditions. This identifies features that need a defined machining sequence or measurement approach before production commitments are made.
- Confirm critical-to-quality dimensions and datum relationships
- Review blind features, thin walls, threads, and tool access
- Clarify material condition, quantity, and functional interfaces
- Align inspection requirements with drawing revision

CNC Process Planning
A capable process route is selected from the part geometry and order requirements rather than assumed from material alone. CNC milling, turning, multi-axis machining, or micro-machining may be considered alongside fixture strategy, stock allowance, and chip-control needs for 303 stainless steel.
- Match turning or milling strategy to feature geometry
- Plan workholding to protect critical datums
- Sequence roughing and finishing around dimensional priorities
- Identify features requiring secondary operations

EDM and Grinding Strategy
Where geometry or finish requirements exceed practical cutter access, SUUXIANG evaluates wire EDM, sinker EDM, and precision grinding as controlled secondary processes. Electrode design, wire path, grinding stock, and heat-treatment sequence should be reviewed against the drawing and functional surfaces.
- Assess inaccessible internal corners and narrow slots
- Define electrode or wire-EDM requirements early
- Preserve grinding allowance on precision surfaces
- Review process order after heat treatment when specified

Inspection and Revision Control
Inspection planning follows the approved drawing, identified critical dimensions, and agreed reporting requirements. During cnc machining 303 stainless steel production, SUUXIANG keeps revision information and delivery coordination visible so the final documentation corresponds to the order and verified inspection plan.
- Set inspection methods for critical dimensions
- Record drawing revision and order-specific requirements
- Confirm reporting needs before production release
- Coordinate delivery against the agreed project information

CNC Machining 303 Stainless Steel: Drawing-Led Control
Compare a documented engineering workflow with the risks of a generic quote-only sourcing path.
← Swipe left or right to view →
CNC Machining 303 Stainless Steel: Drawing to Inspected Parts
A drawing-led sequence that keeps material, critical dimensions, process decisions, inspection requirements, and delivery coordination visible before production proceeds.
Review RFQ Package
Review drawings, models, material callouts, quantity, application context, target date, and inspection needs; clarify critical dimensions, datums, surface requirements, and revision status before quotation.
Plan Process Route
Confirm 303 stainless steel sourcing requirements and develop the CNC machining 303 stainless steel route, including tool access, machining sequence, EDM needs, grinding allowance, and inspection checkpoints.
Machine Critical Features
Produce applicable features through CNC milling, turning, multi-axis machining, wire EDM, sinker EDM, or precision grinding, following the approved drawing and controlled revision information.
Inspect and Document
Verify dimensions and specified surface requirements against the agreed inspection plan, record applicable results, and resolve any drawing or measurement questions before final release.
Pack and Coordinate Delivery
Protect finished parts for shipment, align packing and documentation with the order, and coordinate delivery details so receiving teams can identify the correct revision and requirements.
How to Work With SUUXIANG
Move from files and requirements to a reviewed production plan, inspected parts, and coordinated delivery.
Submit Your Files
Send the 2D drawing, 3D model when available, 303 material specification, quantity, delivery target, critical dimensions, surface requirements, and inspection expectations.
Review DFM Details
Confirm datum strategy, tolerance stack, tool access, machining route, EDM or grinding needs, heat-treatment sequence, and any application constraints before quotation.
Approve the Production Plan
Review the quotation, revision status, quality requirements, and sample or first-article expectations where needed before releasing cnc machining 303 stainless steel parts.
Coordinate Production and Delivery
SUUXIANG manages the agreed machining, inspection, documentation, revision communication, and delivery coordination against the approved drawing and verified inspection plan.
Certification and Quality Documentation
Customer References Published Upon Authorization
SUUXIANG publishes customer outcomes only after the customer’s wording, project details, and measurable results are authorized for public use.
Customer names, delivery metrics, tolerance results, and inspection claims are published only when substantiated and cleared for release.
Drawing-driven machining outcomes require applicable order records, inspection evidence, and customer authorization before public publication.
CNC Machining 303 Stainless Steel FAQ
Practical answers for engineering, quality, and sourcing teams preparing a drawing-led 303 stainless steel RFQ.
What files should I send for cnc machining 303 stainless steel?
Can cnc machining 303 stainless steel support prototypes and low-volume production?
How long does cnc machining 303 stainless steel take?
Is 303 stainless steel the right choice for my part?
Do I need to specify heat treatment for 303 stainless steel?
What inspection reports can I request?
Can you ship 303 stainless steel parts internationally?
How are payment terms and intellectual property handled for custom parts?
Complete Guide to cnc machining 303 stainless steel
A practical decision framework for selecting 303, defining DFM and inspection requirements, qualifying CNC suppliers, controlling cost, and avoiding material, tolerance, corrosion, documentation, and launch mistakes in drawing-based production.
1. What Is cnc machining 303 stainless steel?
AISI 303 is a free-machining austenitic stainless steel grade. CNC machining of 303 stainless steel uses programmed milling, turning, drilling, and threading operations to convert specified bar or billet stock into drawing-controlled precision parts.
Sulfur improves chip breakage during cutting. Shorter, more manageable chips can simplify machining of intricate turned-and-milled geometries such as shafts, threaded fittings, connector components, and mold-related hardware, where tool access, thread quality, and chip evacuation affect the process route.
304 and 316 are comparison grades buyers should review before releasing a drawing. The sulfur that makes 303 easier to machine can reduce corrosion resistance relative to 304 and 316, so material selection must consider the service environment alongside cycle-time and manufacturability priorities. Confirm the specified material condition, critical dimensions, surface requirements, and inspection method in the RFQ.
2. Why 303 Became a Machining Grade
303 stainless steel is an austenitic free-machining grade formulated with sulfur to improve chip breakage relative to 304; that same addition can reduce corrosion resistance.
Free-machining stainless grades address a production problem: long, continuous chips can complicate turning, drilling, and thread cutting. Shorter, more controllable chips can reduce tool entanglement and make CNC cycles more predictable, but the specified service environment must still govern grade selection.
Turned geometries and repeated internal or external threads are where this rationale remains practical. For CNC machining of 303 stainless steel, the drawing should define thread standard, datum relationships, surface condition, and any corrosion exposure before machinability is treated as the deciding criterion.
3. Types of cnc machining 303 stainless steel
303 stainless steel supports several CNC routes because its chip-breaking behavior suits turned and milled features. Route selection should follow drawing geometry, feature access, batch size, datum control, and inspection requirements—not a generic machine preference.
CNC And Swiss Turning
CNC turning suits rotational shafts, bushings, threaded fittings, and connector shells; runout and chuck distortion are key risks. Swiss-type turning suits long, small-diameter pins, where guide-bushing support limits deflection and inspection must confirm concentricity.
Three-Axis Milling
3-axis milling suits prismatic plates, pockets, slots, and mold inserts accessible from indexed setups. Two or more setups can create datum-transfer risk, so fixture faces and probing references should be defined before machining.
Multi-Axis And Mill-Turn
4/5-axis milling suits angled holes, compound contours, and features requiring fewer reclamps; collision clearance and tool reach require review. Mill-turn suits parts combining turned diameters with cross-holes, flats, or milled drive features.
Secondary Feature Control
Secondary threading, tapping, reaming, and deburring address functional threads and safe edge conditions after primary machining. Thread gauges, burr limits, and access for tools or inspection should be specified on the drawing.
4. Materials for cnc machining 303 stainless steel
303, 304, and 316/316L are austenitic choices with different chip control, corrosion limits, and total-cost consequences. Select the grade from the service environment and downstream fabrication requirements.
| Grade | Machinability | Corrosion Exposure | Cost Driver | Typical Use |
|---|---|---|---|---|
| 303 | Best chip control | Mild exposure | Lower cycle time | Threads, shafts, fittings |
| 304 | Moderate; work-hardens | General exposure | More tool time | General components |
| 316/316L | Most demanding | Chloride exposure | Alloy and machining cost | Marine or chemical parts |
Grade Selection
303 contains sulfur for improved chip breaking; it suits threaded, turned, and heavily machined components. 304 is a balanced general-purpose choice, while 316/316L better suits chloride exposure.
303 is generally avoided where welding is required because sulfur can reduce weld quality. Confirm the weld procedure and corrosion duty before substituting 303.
Stock Form And Documentation
Bar is usually efficient for turned parts; plate and billet suit milled geometries or larger starting envelopes. Stock form changes material yield, setup strategy, and cost.
Each RFQ should state the applicable material standard, condition, heat or lot traceability, and required mill certificate. Match documentation to the purchase order and inspection plan.
Decision Evidence
303’s sulfur addition improves machining but can reduce corrosion resistance relative to 304; 316 is commonly considered where chloride exposure is a concern.
Chromium content contributes to stainless corrosion resistance, while material condition affects mechanical properties. Confirm the applicable material standard, service environment, and acceptance requirements in the RFQ.
5. Finishes and Part Customization Options
Finish callouts should state the surface, measurement method, and functional reason—not merely a visual label. For cnc machining 303 stainless steel, separate sealing, sliding, electrical, and cosmetic surfaces before routing.
| Option | Primary Purpose | Drawing Control |
|---|---|---|
| Bead blasting | Uniform cosmetic texture | Media, coverage, masking |
| Passivation | Post-process corrosion support | Specification and acceptance test |
| Laser marking | Identification and traceability | Location, content, legibility |
Functional Finishes
Ra values belong on the drawing face or feature, with cutoff and direction where function depends on texture. Passivation or electropolishing requires evaluation against the service environment and a defined acceptance method.
- Specify bead blast media and target appearance.
- Specify polishing direction on mating surfaces.
- Keep functional surfaces protected during finishing.
Edges And Features
0.2–0.5 mm edge breaks are common only when compatible with the design; call out exceptions at sharp sealing edges or datums. Dimension threads, inserts, keyways, flats, holes, and mating interfaces from stated datums, including class, depth, positional tolerance, and engagement requirements.
Cosmetic Approval And Marking
First-article samples should establish the approved cosmetic standard when color, blast uniformity, polish, or laser-mark contrast matters. Serialized marking needs location, character height, data format, and permanence requirement linked to the inspection record.
6. cnc machining 303 stainless steel Quality Controls
A robust cnc machining 303 stainless steel order defines acceptance before material is cut. The drawing review should connect functional geometry, datum references, feature access, and a practical measurement method.
Datums And GD&T
Three datum features are often sufficient to establish repeatable setup and inspection alignment. Identify critical-to-function dimensions, interpret GD&T relative to those datums, and review tolerance stack-up across mating features before release.
Threads, Edges And Finish
Go/no-go thread gauges should match the specified thread standard and class; do not rely on visual thread checks. State burr limits, edge-break requirements, and surface-roughness callouts by functional surface, including locations inaccessible to a probe or stylus.
Inspection And Traceability
A first-article report should verify agreed critical features before continuing production. In-process checks should target dimensions affected by tool wear or re-clamping, while final inspection follows the approved plan and order revision.
Each material lot should remain traceable to supplied documentation when the order requires it. A nonconformance should be recorded, contained, dispositioned with customer input where needed, and linked to the affected revision and inspection evidence.
7. How to Choose a 303 CNC Manufacturer
303 stainless requires more than a price comparison because sulfur-bearing chemistry changes corrosion-risk decisions. Qualify the supplier’s evidence, controls, and response to drawing uncertainty before release.
Review DFM And Process Fit
Ask for drawing-review feedback before quotation, including datum conflicts, tool access, thread strategy, and burr control.
Require the proposed milling, turning, EDM, grinding, and inspection route to match critical features.
- Identify ambiguous dimensions and acceptance criteria
- Confirm machining sequence and clamping datum
- Escalate corrosion exposure before material release
Verify Material And Quality Evidence
Request material identification and traceability evidence tied to the purchase requirement, not a generic material statement.
Define CTQ dimensions, gages, sampling, first-article approval, and the report format before production.
- Material certificate or agreed traceability record
- First-article inspection plan
- Surface and corrosion-risk review
Control Delivery And Changes
Set a written revision baseline for the drawing, model, quantity, packaging, and delivery milestone.
Ask how changes are acknowledged, capacity is scheduled, parts are protected in transit, and delays are communicated.
- Revision-controlled acknowledgement
- Realistic lead-time breakdown
- Protective packaging for finished surfaces
8. Common cnc machining 303 stainless steel Mistakes
Preventable specification gaps routinely cost more than a 303 machining cycle-time advantage. Close them during drawing review, before a purchase order freezes material, tolerances, inspection, and quote scope.
Match The Service Environment
303 contains sulfur for machinability, which reduces corrosion resistance versus 304 and 316. Do not release it for chloride or aggressive exposure without an application-specific material review; select and document the required grade instead.
Specify Material Condition
303, 304, and 316 are not interchangeable because alloying and condition affect corrosion behavior and mechanical properties. State the governing material specification, condition, heat-treatment requirement, and traceability evidence on the order.
Control Functional Features
2D drawings should identify critical dimensions, datums, thread class, surface requirement, and burr-sensitive mating edges. Applying tight tolerances everywhere increases inspection and machining cost; assign tolerances and deburring requirements only where function demands them.
Align CAD And Quote Scope
Released CAD without a manufacturability review can hide tool-access, thread, or edge-break conflicts. Before PO release, compare like-for-like quotes covering revision, material, quantity, finishing, inspection report, packaging, and delivery terms.
9. Steps to Launch a 303 CNC Part
A controlled launch for cnc machining 303 stainless steel begins before pricing: define the part’s function, acceptance criteria, and release authority. Separate prototype learning from repeat-production controls so a drawing change does not silently alter an approved process.
Build The Quote Package
First, provide a revision-controlled 2D drawing, 3D CAD model, quantity, 303 material callout, finish, and requested delivery date. Identify critical dimensions, datums, threads, surface requirements, mating context, required quality records, and packaging expectations.
Close The DFM Review
Next, review tool access, tolerances, inspection methods, deburring, and any feature requiring turning, milling, EDM, or grinding. Confirm the approved material form and finish before releasing a purchase order; clarify unresolved notes through a documented revision.
Approve And Control Production
For low volumes, approve a prototype or first article against the agreed inspection plan before a pilot build. For repeat orders, freeze the approved drawing, inspection criteria, packaging, and delivery schedule; route every revision through impact review and written authorization.
10. cnc machining 303 stainless steel Pricing & Cost
1-piece and prototype orders concentrate programming, workholding, first-article inspection, and material-cutoff cost into few parts. For cnc machining 303 stainless steel, stock form, part envelope, tool access, cycle time, thread count, finish, and expected yield must be defined before a cost comparison is meaningful.
10-piece, 50-piece, and repeat-release quotes normally redistribute setup cost, but they do not erase costs from tight tolerances, extra inspection, or documentation. Comparable quotations require the identical revision-controlled drawing, material condition, quantity, acceptance criteria, reporting scope, and requested delivery date.
| Quantity tier | Primary unit-cost drivers | Lead-time variables |
|---|---|---|
| 1–5 | Setup, fixtures, stock cutoff, first article | Material availability; programming queue |
| 6–50 | Cycle time, threads, tolerance zones | Tooling needs; inspection sampling |
| 51–250 | Yield, tool life, finish operations | Batch size; outside processing |
| Repeat releases | Revision stability, documentation, order cadence | Forecast accuracy; delivery schedule |
Start Your CNC Machining 303 Stainless Steel RFQ
Upload your drawing with material, quantity, critical dimensions, inspection expectations, and target delivery date for a disciplined manufacturing review.