
CNC Machining 440C Stainless Steel, From Drawing to Inspected Parts
SUUXIANG plans CNC machining of 440C stainless steel with DFM, EDM, grinding, and inspection aligned to the drawing’s critical dimensions.
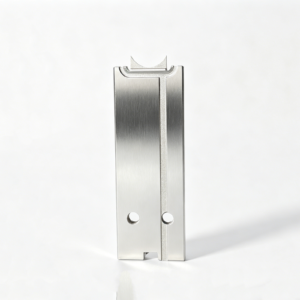
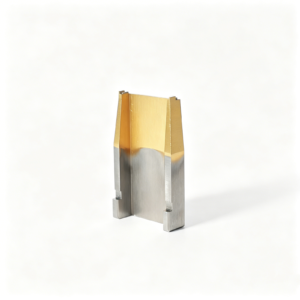
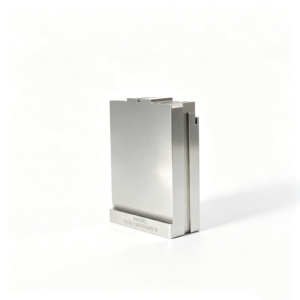
Representative Tooling Components for 440C Drawing Review





Related Configurable Component Families and Quotation







Why CNC Machining 440C Stainless Steel Needs a Controlled Route
SUUXIANG aligns drawing review, heat-treatment sequence, EDM and grinding allowances, inspection planning, and revision control before production commitments.
Drawing-Led DFM Review
Review critical dimensions, datums, thin sections, tool access, and tolerance stack before selecting a practical manufacturing route.
Heat-Treat Sequence
Plan machining stock and finishing stages around the specified heat-treatment condition, helping manage dimensional movement and final-feature access.
EDM Strategy
Assess wire paths, electrode needs, corner geometry, and inaccessible features early so EDM supports the required part definition.
Grinding Allowance Control
Define grinding stock, reference surfaces, and finishing order where hardened surfaces or critical geometry need a controlled final operation.
Inspection Plan Alignment
Match critical characteristics, datum references, measurement methods, and requested reporting to the order before final inspection.
Revision Visibility
Keep drawing revisions, process decisions, and delivery information visible to reduce ambiguity across engineering, quality, and procurement teams.
Precision Machining for Tooling and Components
Drawing-driven process planning for configurable mold, connector, die and custom component requirements.

CNC Machining Services
Precision CNC machining services planned from drawings, critical dimensions, material requirements and inspection needs. Process routes may combine milling, turning, EDM, grinding and fitting according to feature access, tolerance strategy and the verified production scope.
Upload a Drawing
CNC Milling
Custom CNC milling services for prismatic parts, mold plates, inserts, pockets, contours and datum features. Drawing review considers cutter access, corner radii, workholding, machining allowance and the relationship between machined surfaces and downstream EDM or grinding.
Upload a Drawing
CNC Turning
Precision CNC turning services for shafts, pins, bushings, sleeves, collars and rotational features. Requirements should define datums, concentricity or runout priorities, thread details, material condition, surface requirements and any secondary milling, EDM or grinding operations.
Upload a Drawing
5-Axis Machining
5-axis CNC machining supports multi-face features, complex contours and angled geometry where fewer setups can protect datum relationships. Feasibility depends on tool access, fixture strategy, material condition, feature depth, tolerance priorities and inspection method.
Upload a Drawing
Swiss & Micro Machining
Swiss machining and micro machining support small, slender and detail-intensive components such as pins, miniature shafts and connector-related features. Quote review should identify diameter-to-length relationships, tolerances, material, burr limits, surface needs and inspection approach.
Upload a Drawing
Wire & Sinker EDM
Wire EDM and sinker EDM services address hardened materials, internal profiles, sharp corners, narrow slots and features with limited cutting-tool access. Planning considers wire path or electrode strategy, flushing, recast-layer requirements, EDM allowance and finishing operations.
Upload a Drawing
Precision Grinding
Precision surface and profile grinding provides controlled flatness, parallelism, profile accuracy and final stock removal where required. The drawing review should establish datum surfaces, grinding stock, heat-treatment sequence, surface specification and the inspection method for critical features.
Upload a Drawing
Mold Core & Cavity Inserts
Precision mold core and cavity inserts are manufactured as configurable components from approved drawings and models. Process planning addresses steel selection, heat treatment, cooling or vent features, shutoff geometry, EDM access, grinding stock, fitting requirements and inspection priorities.
Upload a Drawing
Ejector & Ejection Components
Ejector pins, sleeves and ejection components are produced to drawing-defined geometry, material condition and movement requirements. A review should clarify fit relationships, guidance, lubrication or venting features, hardness, surface condition, burr control and mating-component dimensions.
Upload a Drawing
Core Pins, Guide & Locating Components
Core pins, guide pins and locating components require careful control of datum relationships, fit, wear surfaces and mating geometry. Manufacturing planning considers material, heat treatment, grinding sequence, concentricity, lead-in details and inspection of functional dimensions.
Upload a Drawing
Slides, Lifters, Gates & Mold Accessories
Mold slides, lifters, gates and accessories are supplied as drawing-based component families rather than assumed standard inventory. Review focuses on travel and interference conditions, wear interfaces, shutoff faces, cooling or venting needs, fitting stock and assembly references.
Upload a Drawing
Connector Mold Components
Precision connector mold components support terminal, housing and insert-molding tooling where small features and alignment are critical. Feasibility review addresses cavity detail, pin geometry, material, EDM strategy, polishing or grinding requirements, mating parts and inspection evidence.
Upload a Drawing
Stamping Die Components
Precision stamping die components include punches, dies, inserts, guides and related wear parts manufactured to customer drawings. Process planning considers tool steel, heat treatment, cutting-edge geometry, clearance relationships, surface condition, grinding allowance and inspection criteria.
Upload a Drawing
Injection, MIM, CIM & Overmolding Tooling
Injection, MIM, CIM and overmolding tooling work is evaluated within SUUXIANG’s verified production scope. Drawings should identify molding material, shrinkage assumptions, parting and shutoff requirements, gates, inserts, thermal conditions, critical dimensions and required documentation.
Upload a Drawing
Machining Materials
CNC machining materials are reviewed against the drawing, application, heat-treatment condition, corrosion or wear requirements and material traceability needs. Final material selection and availability should be confirmed before production commitments are made.
Upload a Drawing
Surface Finishes & Heat Treatment
Surface finishing and heat treatment are specified according to functional requirements such as wear, corrosion resistance, friction, appearance or dimensional stability. Review should define treatment sequence, masking needs, finish callouts, post-treatment stock and verification requirements.
Upload a Drawing
Quality, Metrology & Documentation
Precision inspection, metrology and quality documentation are planned around critical dimensions, datums, tolerances and customer reporting needs. The required evidence may include inspection records, material information, revision identification and order-specific traceability documentation.
Upload a Drawing
Prototyping & Low-Volume Production
Rapid prototyping and low-volume manufacturing support drawing-based validation, tooling development and controlled production quantities. An effective RFQ includes drawings or models, material, quantity, critical features, inspection expectations, revision status and target delivery date.
Upload a DrawingCNC Machining 440C Stainless Steel: Material Options

440C Stainless Steel
A high-carbon martensitic stainless option for wear-focused mold inserts, bearing-related parts, valve features and precision tooling. Review heat-treatment sequence, distortion risk, machining allowance and final grinding requirements against critical dimensions.

420 Stainless Steel
A martensitic stainless option for mold components and corrosion-conscious tooling where hardness and polishability must be balanced. Specify material condition, heat treatment, surface requirement and any EDM or grinding stock in the drawing package.

410 Stainless Steel
A martensitic stainless choice for mechanical parts, fixtures and tooling components requiring moderate corrosion resistance with heat-treatable strength. Drawing review should confirm operating load, hardness target, thread details and post-treatment finishing needs.

17-4 PH Stainless
A precipitation-hardening stainless option for precision components where strength, corrosion resistance and dimensional stability are application priorities. Confirm required condition, machining stage, aging sequence, datums and inspection method before production planning.

304 Stainless Steel
An austenitic stainless option for corrosion-resistant brackets, housings, fittings and custom machined parts. Its non-hardenable condition changes the process route, so tool access, wall stiffness, surface finish and functional environment require drawing-based review.
CNC Machining 440C Stainless Steel: Supported Processes

CNC Milling
Milling develops pockets, contours, faces and accessible features before or after heat treatment, with tool access, workholding rigidity and machining allowance reviewed against the drawing’s critical dimensions.

Precision Turning
Turning supports concentric diameters, shoulders, bores and rotational features. The route considers datum relationships, stock condition, chip control and whether final size requires subsequent grinding or hard finishing.

Wire EDM
Wire EDM is considered for narrow slots, internal profiles, sharp-corner requirements and hardened sections where conventional tool access is limited. Wire path, start-hole location, finish allowance and datum strategy are reviewed first.

Sinker EDM
Sinker EDM forms deep cavities, fine details and features requiring a controlled electrode approach. Electrode design, flushing, surface requirement and downstream polishing or fitting needs guide the process plan.

Precision Grinding
Grinding brings controlled finishing to selected diameters, flats and datum surfaces after machining or heat treatment. Required stock, part stability, surface specification and inspection method determine whether grinding is appropriate.

Fitting & Inspection
Fitting and inspection confirm functional relationships, critical dimensions and documented requirements against the agreed plan. Measurement methods, reporting needs and revision status should be defined before production begins.
CNC Machining 440C Stainless Steel Tooling Accessories

Guide Locating Elements
Guide pins, bushings, locating blocks and datum features can be machined to the drawing-defined fit, alignment and wear requirements of mold or connector tooling assemblies.

Ejection Components
Ejector pins, sleeves, blades and related ejection features are configured around stroke, clearance, bearing length and mating-component conditions supplied with the tooling design.

Slides and Lifters
Slides, lifters, wear interfaces and angled motion components can be evaluated for machining access, heat-treatment sequence, grinding stock and critical contact surfaces before production.

Gate Insert Features
Gate inserts, runner details and localized flow-control features are produced from drawing data, with EDM strategy, edge condition and interface dimensions reviewed against the mold design.

Mold Accessory Details
Stops, retainers, spacers, support elements and custom mounting details can accompany CNC machining 440C stainless steel components when material, tolerances and inspection requirements are defined.
About SUUXIANG Precision Manufacturing
SUUXIANG is the sole public-facing brand of Dongguan SuuXiang Precision Mold Co., Ltd., established in 2010 in Chang’an Town, Dongguan, Guangdong, China. Founded by XiaoCheng Huang, the company helps customers translate drawings, models, material requirements, and quality expectations into inspected custom parts, precision mold components, connector tooling, and die components.
For cnc machining 440c stainless steel and other drawing-based projects, our planning connects CNC milling and turning, multi-axis machining, EDM, grinding, fitting, and inspection as the part requires. Before quotation or production commitments, we review critical dimensions, datums, machining access, heat-treatment sequence, grinding allowance, and inspection needs.
Our difference is disciplined project communication rather than generic quoting. SUUXIANG keeps revision, process, and delivery requirements visible while aligning inspection documentation with the agreed order and verified plan. Upload a 2D drawing, 3D model when available, material, quantity, delivery target, and reporting requirements for a focused manufacturing review.

CNC Machining 440C Stainless Steel: Controlled Workflows
DFM and Datum Review
Before quotation, SUUXIANG reviews the drawing, model, critical dimensions, datums, wall conditions, tool access, and functional interfaces. This establishes a practical machining route for CNC machining 440C stainless steel and identifies information that should be resolved before production commitments.
- Confirm critical-to-quality dimensions and datum relationships
- Review deep features, radii, thin sections, and access limits
- Align material condition and heat-treatment requirements
- Clarify mating-part and application context when relevant

CNC and EDM Strategy
Feature geometry determines whether milling, turning, wire EDM, sinker EDM, or a combined route is appropriate. SUUXIANG plans the sequence around reachable surfaces, internal corners, electrode requirements, wire paths, and the dimensions that must remain stable through subsequent operations.
- Match process selection to geometry and tolerance requirements
- Define electrode and wire-EDM needs during drawing review
- Protect datum features through intermediate operations
- Keep process decisions tied to the approved revision

Grinding Allowance Planning
For parts requiring heat treatment and fine finishing, stock allocation must be considered before initial machining. SUUXIANG evaluates where grinding stock, clamping surfaces, and reference features are needed so the finishing route can address final dimensions without treating material movement as an afterthought.
- Plan finish stock on surfaces requiring grinding
- Consider heat-treatment sequence with the part geometry
- Preserve references for post-process setup and inspection
- Review thin or asymmetric features for process risk

Inspection and Revision Control
Inspection planning follows the drawing and agreed quality expectations, with attention to critical dimensions, inspection methods, surface requirements, and report needs. Revision status remains visible through production coordination so CNC machining 440C stainless steel parts are manufactured and documented to the correct order requirements.
- Define critical dimensions and appropriate inspection methods
- Align inspection records with order requirements
- Maintain clear drawing and revision identification
- Communicate open technical points before final release

CNC Machining 440C Stainless Steel: Drawing-Based Review
Compare the engineering evidence that helps control heat-treatment movement, finishing allowances, and revision risk before production.
← Swipe left or right to view →
CNC Machining 440C Stainless Steel: Drawing-to-Delivery Workflow
A drawing-led route that aligns DFM, process planning, critical dimensions, inspection requirements, and delivery coordination before production proceeds.
Review RFQ Package
We review the 2D drawing, 3D model, material condition, quantity, critical dimensions, surface requirements, inspection needs, application context, and target delivery date.
Confirm DFM Route
The team evaluates datum strategy, tool access, wall stability, heat-treatment sequence, machining allowance, and whether EDM or grinding is appropriate for critical features.
Machine Controlled Stock
CNC milling, turning, multi-axis machining, or micro-machining produce the planned geometry while preserving stock where subsequent heat treatment, EDM, or grinding requires it.
Finish Critical Features
Wire EDM, sinker EDM, precision grinding, and fitting are scheduled according to feature geometry, hardness condition, electrode strategy, wire path, and required surface outcome.
Inspect and Document
Inspection follows the agreed plan, focusing on critical dimensions, datums, surface requirements, and requested reporting, with revision information kept aligned to the order.
Pack and Coordinate Delivery
Accepted parts are prepared for shipment with order-matched documentation, protective packing appropriate to the component, and visible coordination of delivery information and revisions.
How CNC Machining 440C Stainless Steel Projects Work
Align requirements, process decisions, inspection expectations, and delivery coordination before production begins.
Submit Your Drawing Package
Provide 2D drawings, 3D models when available, material condition, heat-treatment requirements, quantity, critical dimensions, surface priorities, inspection needs, and target delivery date.
Align the Manufacturing Route
Review DFM, datums, machining access, EDM or grinding requirements, allowances, and inspection methods with SUUXIANG before quotation and production commitments are finalized.
Approve First-Article Evidence
For applicable projects, confirm samples or first-article results against the agreed drawing revision, critical dimensions, material requirements, and inspection plan before continuation.
Coordinate Production and Delivery
Proceed with controlled machining, EDM, grinding, fitting, and inspection while maintaining visible revision status, documentation requirements, and delivery coordination through final shipment.
Quality Documentation for CNC Machining 440C Stainless Steel
How SUUXIANG Handles Customer Feedback
Customer feedback for this CNC machining 440C stainless steel project will be published only after the customer authorizes the quoted outcome, drawing revision context, inspection evidence, and delivery information.
Approved customer feedback will identify the relevant manufacturing outcome, such as a documented dimensional result, revision-control improvement, or delivery milestone, without disclosing confidential drawings, part details, or unsupported performance claims.
SUUXIANG will publish testimonial details only when the customer confirms the wording, role, company attribution, and evidence behind any stated result for CNC machining 440C stainless steel parts.
CNC Machining 440C Stainless Steel FAQ
Practical answers for drawing-based sourcing, process planning, inspection, and delivery coordination.
What should I include in an RFQ for CNC machining of 440C stainless steel?
Is there a minimum order quantity for cnc machining 440C stainless steel parts?
Can I order a sample before production cnc machining 440C stainless steel parts?
Should 440C be machined before or after heat treatment?
How much EDM or grinding allowance is needed for a 440C part?
Can SUUXIANG provide inspection reports with my order?
How are drawings and design revisions handled?
How do payment and international shipping work for custom parts?
Complete Guide to cnc machining 440c stainless steel
Use this decision framework to specify 440C parts, manage heat-treatment distortion, evaluate CNC and finishing suppliers, compare cost drivers, and avoid quoting mistakes that compromise tolerance, hardness, wear life, or delivery.
1. What Is cnc machining 440c stainless steel?
440C is a high-carbon martensitic stainless grade machined by CNC milling, turning, drilling, and finish operations into drawing-defined parts. Buyers select cnc machining 440c stainless steel where high hardness and wear resistance matter, such as bearing-related, guiding, cutting, or mold-component features.
0.95–1.20% carbon and 16–18% chromium are published composition ranges for Type 440C; hardened and tempered material can approach Rockwell C 60 (https://www.spacematdb.com/spacemat/manudatasheets/440c.pdf). Its stainless behavior should not be read as broad corrosion immunity: 440C is generally chosen for wear performance first, while the actual exposure medium, finish, and heat-treatment condition require review.
3 process stages commonly control the route: machine annealed stock with allowance, heat treat to the specified condition, then hard-finish critical surfaces by grinding, EDM, or qualified hard machining. Choose 440C when hardness and wear life justify this sequence; compare other grades when corrosion exposure, toughness, weldability, or distortion risk is the governing requirement.
2. Evolution of cnc machining 440c stainless steel
440C contains 0.95–1.20% carbon and 16–18% chromium in a high-carbon martensitic stainless formulation. Its established role in bearing assemblies reflects the combination of heat-treated hardness and wear resistance that drove use in demanding moving or contact surfaces (https://www.spacematdb.com/spacemat/manudatasheets/440c.pdf).
CNC control shifted 440C work beyond straightforward turned bearing features by coordinating multi-axis milling, consistent tool paths, and repeatable datum-based setups. Carbide cutting in the softer condition, followed by heat treatment, lets engineers reserve grinding stock for dimensions most affected by distortion.
EDM and precision grinding expanded access to narrow slots, sharp internal geometry, difficult contours, and hardened finishing features; hard turning can also be evaluated for suitable rotational surfaces. For cnc machining 440c stainless steel, a legacy assumption that every hardened feature must be conventionally ground is therefore incomplete: the drawing review should define material condition, heat-treatment sequence, electrode or wire path, remaining stock, and inspection datum before selecting the route.
3. Types of cnc machining 440c stainless steel Parts
Five recurring families make cnc machining 440c stainless steel a drawing-review exercise, not a catalog choice. Geometry, hardened load path, finishing route, and final-tool access determine the feasible process plan.
Mold Cores And Inserts
440C cores commonly combine deep cavities, shutoffs, and small radii for abrasive molding duty. Soft machining, heat treatment, EDM, and grinding require stock and post-hardening access.
Bearing And Wear Components
440C races, bushings, and wear sleeves use rotational geometry under rolling or sliding contact. Hard turning or cylindrical grinding depends on concentricity, surface requirement, and thin-wall stiffness.
Connector Tooling Components
440C connector punches, core pins, and locating details carry repetitive alignment and wear loads. Wire EDM handles narrow slots; electrode strategy governs tiny internal corners.
Cutting And Valve Components
440C blades, seats, and needle-valve details require controlled edges or sealing lands. Grinding and polishing must preserve geometry while avoiding heat damage at thin sections.
Prototype And Low-Volume Parts
1-to-low-volume precision parts often combine flats, bores, threads, and mating datums. Revision-controlled inspection should focus on critical features before committing to a hardened finishing route.
4. 440C Material Condition and Alternatives
440C must be specified as a material-and-condition system, not merely a grade. Condition changes machining route, finishing allowance, distortion risk, and the inspection plan for cnc machining 440c stainless steel.
| Grade | Hardness | Corrosion | Toughness | Machinability | Typical Use |
|---|---|---|---|---|---|
| 440C | High | Moderate | Low | Moderate annealed | Wear components |
| 420 | Medium-high | Moderate | Moderate | Better | Mold parts |
| 17-4PH | High | Good | Good | Moderate | Structural tooling |
| D2 | Very high | Low | Low | Difficult | Die wear parts |
| 316 | Low | Very good | High | Moderate | Corrosive service |
State The Delivery Condition
Annealed 440C is normally selected for primary machining; hardened-and-tempered stock requires hard machining, EDM, or grinding. State target hardness, heat-treatment sequence, and any post-treatment stock on both drawing and PO.
Keep Material Traceable
Mill certificates should link the received heat or lot to the ordered grade and condition. Record certificate review, heat-treatment evidence where required, and part revision together; do not substitute an unverified equivalent.
Validate The Application
440C can reach about 60 HRC after heat treatment; final selection still needs application-specific validation. Source: https://www.spacematdb.com/spacemat/manudatasheets/440c.pdf
5. Finishes and Post-Processing for 440C
440C finishing should be specified by function: datum, Ra target, edge-break limit, and inspection method. ‘Polished’ alone does not define size, burr condition, friction, wear, or corrosion exposure.
| Operation | Primary Change | Does Not Guarantee |
|---|---|---|
| Grinding | Form and Ra | Edge radius |
| Hard turning | Accessible finish | EDM geometry |
| Passivation | Surface cleanliness | Wear resistance |
Precision Grinding
Precision grinding controls hardened critical diameters, flats, and sealing faces after heat treatment. Specify the datum, allowable stock removal, Ra, and measurement method.
Grinding can improve form and surface texture but may leave sharp edges. Call out a maximum edge break or controlled radius, not a cosmetic deburr note.
Hard Turning And EDM
Hard turning can finish accessible rotational features with fewer setups. Confirm roundness, runout, Ra, and tool-access limits against the drawing.
EDM creates complex hardened features without cutting-force distortion. Specify wire or electrode finish, recast-layer disposition where critical, and edge condition after EDM.
Polishing, Passivation, And Coatings
Polishing lowers roughness but can round edges and alter fits. Define the functional area and measurable roughness rather than requesting a mirror appearance.
Passivation removes surface contamination; it does not add hardness or repair heat-treat damage. Evaluate coatings against mating contact, adhesion, dimensional build, and service environment.
6. Quality Controls for cnc machining 440c stainless steel
440C quality control begins before cutting: the drawing must define functional datums, final material condition, and the inspection stage for every critical feature. For cnc machining 440c stainless steel, final acceptance should follow heat treatment and final finishing.
Define Functional Datums
Three datum references should locate a feature from its mating function, not from convenient raw edges. Identify primary, secondary, and tertiary datums on the drawing, then state whether dimensions apply before or after heat treatment.
- Mark critical-to-quality dimensions
- Specify datum-based measurement setup
- State final-process inspection condition
Plan Stock And Distortion
0.2–0.5 mm per side is a commonly cited pre-heat-treatment finishing allowance, but geometry and heat-treatment route require project review. Thin walls, unequal sections, and long unsupported features need distortion planning and enough grinding stock for final correction. Source: https://www.jcproto.com/new/440c-stainless-steel-machinability.html
Verify Final Condition
60 HRC is an approximate hardened-and-tempered 440C reference, not an acceptance criterion unless the order specifies it. Record hardness method, test location, surface-finish requirement, burr condition, and final dimensional results after grinding, EDM, or hard finishing. Source: https://www.spacematdb.com/spacemat/manudatasheets/440c.pdf
- Confirm hardness test locations
- Inspect edges for functional burrs
- Measure dimensions after final processing
7. How to Choose a 440C Machining Supplier
440C sourcing should test production control, not merely whether a shop can quote hardened stainless. A credible response connects the drawing, heat-treatment route, finishing allowance, inspection plan, and revision record.
Test The DFM Response
2D drawings should receive a DFM response identifying datums, thin sections, tool access, and critical dimensions.
1 review question matters: what stock remains for grinding after heat treatment, and who approves any route change?
- Request marked-up drawing feedback
- Ask for process-flow ownership
- Confirm revision-control method
Verify The Process Chain
440C requires evidence of experience with hardened martensitic stainless, controlled heat treatment, and distortion planning.
EDM and grinding capability should be tied to the part’s geometry, finish requirement, and final datum scheme.
- Heat-treatment certificate and lot link
- Grinding or EDM route
- Allowance and distortion plan
Audit Evidence And Communication
First articles should follow a defined inspection plan using suitable metrology and material traceability.
SUUXIANG can review drawings and coordinate CNC, EDM, grinding, fitting, and inspection within verified scope; request sample records, capacity timing, and an escalation contact.
- Material certificate
- First-article report
- Inspection-equipment list
- Capacity and lead-time basis
8. Common cnc machining 440c stainless steel Mistakes
440C is a high-carbon martensitic stainless steel, so its routing cannot be copied from 304. Resolve material condition, heat treatment, datums, and functional tolerances during drawing review before a supplier prices the job.
Treating 440C Like 304
440C’s carbide-rich structure changes cutting behavior and hard-finish options. Using 304-style assumptions can raise tool wear, cycle time, and quotation-to-production variance; request a process route tied to the specified condition.
Leaving Hardness Undefined
HRC and heat-treatment state determine distortion risk and the finishing method. State annealed, pre-hardened, or final target hardness with the drawing; otherwise, parts may arrive machinable but unsuitable for wear service.
Finishing Before Heat Treatment
0.2–0.5 mm per-side stock is often evaluated for post-heat-treatment finishing, subject to geometry and the approved route. Holding final size before heat treatment risks warp, undersize conditions, rework, or scrap.
Overconstraining Geometry And Corrosion
Small internal radii can force undersized cutters, long reach, EDM, and extra cost. Apply tight tolerances only to functional features, specify accessible corner radii, and assess the actual environment: 440C is not automatically marine-grade corrosion resistant.
9. From RFQ to First Article
Two controlled files start a credible RFQ: the revision-marked 2D drawing and native or neutral 3D model. Engineering, quality, procurement, and program ownership should be named before quotation feedback is released.
Define Material State
440C must be specified as annealed stock or a required final hardness range, with heat-treatment responsibility and certification needs stated. Procurement should also identify approved material equivalents before release.
Set Datums And CTQs
Three datum references are often more useful than a blanket tight-tolerance note. Engineering should mark critical dimensions, mating features, geometric controls, surface requirements, and measurement method where it affects acceptance.
Close DFM Before Cutting
One DFM review should resolve tool access, wire paths, EDM electrodes, heat-treatment movement, and grinding stock. Program teams should record decisions; quality should confirm that the proposed inspection plan measures the stated CTQs.
Approve First Article And Revisions
First-article approval should compare the agreed revision, material evidence, and inspection results against the purchase-order requirements. Repeat orders need a controlled drawing revision, approved deviation record, and written confirmation before any process change.
10. Pricing cnc machining 440c stainless steel
1-piece orders concentrate programming, setup, fixturing and first-article inspection in each part; figures below are indicative planning ranges, not SUUXIANG price or lead-time commitments. Final pricing for cnc machining 440c stainless steel requires the current drawing, model, material condition, quantity and inspection plan.
0.01 mm-class requirements can shift a route from finish milling to grinding, EDM or both, while hardened-condition work also changes tooling, stock allowance and heat-treatment coordination. Reduce total cost by keeping functional tolerances and surface requirements only on critical features, providing datum and mating-part context, selecting practical stock sizes, and batching identical revisions; do not remove inspection or post-process controls that protect function.
| Quantity tier | Indicative unit-cost driver | Typical planning lead time |
|---|---|---|
| 1–5 | Setup, fixture and first article dominate | 10–20 business days |
| 6–50 | Cycle time, stock yield, grinding or EDM | 15–30 business days |
| 51+ | Repeat fixture, inspection sampling, order volume | Quote-dependent |
Start Your CNC Machining 440C Stainless Steel Drawing Review
Upload your 2D drawing and 3D model, plus material, quantity, quality requirements, and target delivery date for a disciplined RFQ review.