
Mold Lifters Built From Your Controlled Drawings
Move from drawing review to inspected mold lifters with coordinated CNC machining, EDM, grinding, and revision-aware quality planning.
Representative Precision Tooling Components





Related Configurable Component Families





Why Source Mold Lifters Through SUUXIANG
A drawing-driven workflow for mold lifter components where manufacturability, critical dimensions, process planning, inspection, and revisions remain visible.
Drawing-First Review
Review drawings, models, application context, and undercut requirements before quotation to identify machining access, datums, and production questions.
Coordinated Process Routes
Plan CNC machining, wire or sinker EDM, grinding, fitting, and inspection around the component geometry and specified functional surfaces.
Critical Dimensions Planned
Align critical dimensions, tolerance stacks, datum references, grinding stock, and inspection methods with the drawing before production commitments.
Inspection Matched to Requirements
Define inspection expectations from the order and drawing, with measurement priorities focused on features that affect mold lifter function.
Revision Visibility
Keep drawing revisions, clarification points, quality expectations, and delivery coordination visible throughout the manufacturing workflow for better control.
Mold Lifters and Precision Tooling Components
Configure the process route around drawing requirements, critical dimensions, material condition, inspection needs, and production quantity.

CNC Machining Services
Precision CNC machining services for drawing-based parts requiring a defined route through milling, turning, EDM, grinding, fitting, and inspection. Submit the drawing, material, quantity, critical dimensions, and delivery requirements for a manufacturability review before quotation.
Upload a Drawing
CNC Milling
Custom CNC milling services for prismatic parts, plates, inserts, and features requiring controlled tool access. Drawing review should identify datum surfaces, pocket depth, corner conditions, machining allowance, surface requirements, and inspection points before programming.
Upload a Drawing
CNC Turning
Precision CNC turning services for shafts, pins, sleeves, bushings, and rotational features. Specify diameters, concentricity or runout requirements, thread details, material condition, mating relationships, and any downstream grinding or heat-treatment sequence.
Upload a Drawing
5-Axis Machining
5-axis CNC machining for complex contours, angled features, and parts where multi-face access affects setup strategy. Review the model with the drawing to confirm tool reach, fixture approach, datum transfer, surface requirements, and measurable critical features.
Upload a Drawing
Swiss & Micro Machining
Swiss machining and micro machining for small-diameter pins, connector features, slender shafts, and detailed rotational components. RFQs should clarify geometry, tolerances, material, burr-control expectations, inspection method, and the functional relationship to mating parts.
Upload a Drawing
Wire & Sinker EDM
Wire EDM and sinker EDM services for hardened features, narrow slots, sharp internal geometry, complex cavities, and profiles beyond conventional tool access. Discuss wire paths, electrode strategy, corner conditions, surface requirements, recast-layer considerations, and subsequent finishing.
Upload a Drawing
Precision Grinding
Precision surface and profile grinding for flatness, parallelism, profile control, and finish requirements after machining or heat treatment. Define datum faces, grinding stock, critical dimensions, material condition, and the inspection method needed for final acceptance.
Upload a Drawing
Mold Core & Cavity Inserts
Precision mold core and cavity inserts produced from customer drawings and 3D models. Review shutoff geometry, cooling or feature access, material and heat-treatment requirements, EDM and grinding needs, fitting relationships, critical dimensions, and inspection expectations.
Upload a Drawing
Ejector & Ejection Components
Ejector pins, sleeves, and ejection components configured to drawing-defined diameters, lengths, fits, and functional interfaces. Identify material condition, hardness requirements, surface needs, clearance relationships, wear considerations, and any matching core or plate features.
Upload a Drawing
Core Pins, Guide & Locating Components
Core pins, guide pins, bushings, and locating components require attention to mating fits, alignment datums, wear surfaces, and assembly relationships. Provide the applicable drawing set, material and heat-treatment requirements, critical dimensions, and inspection priorities.
Upload a Drawing
Slides, Lifters, Gates & Mold Accessories
Mold slides, lifters, gates, and accessories manufactured as configurable tooling components, not assumed stock items. Review travel geometry, bearing or shutoff surfaces, assembly interfaces, material condition, machining access, EDM needs, fitting allowance, and critical checks.
Upload a Drawing
Connector Mold Components
Precision connector mold components for detailed terminal, housing, and insert-molding tooling requirements. Drawings should clarify pitch-critical features, micro geometry, datum strategy, material condition, EDM or grinding requirements, mating components, and inspection documentation.
Upload a Drawing
Stamping Die Components
Precision stamping die components for punches, dies, inserts, guide elements, and related custom parts. Production planning depends on strip-interface details, cutting edges, clearance relationships, material and heat-treatment sequence, grinding stock, and dimensional inspection requirements.
Upload a Drawing
Injection, MIM, CIM & Overmolding Tooling
Tooling and component work associated with injection molding, metal injection molding, ceramic injection molding, and overmolding, when within verified production scope. Provide molding context, material requirements, critical interfaces, tool geometry, expected quantity, and quality documentation needs.
Upload a Drawing
Machining Materials
CNC machining materials selected against functional load, corrosion exposure, wear, machinability, dimensional stability, and downstream heat treatment or finishing. State the specified grade, approved substitutions if any, material certification needs, and the application context affecting selection.
Upload a Drawing
Surface Finishes & Heat Treatment
Surface finishing and heat treatment planned around material grade, wear or corrosion requirements, dimensional risk, and final surface function. Confirm the specified process, hardness or finish target, masking needs, sequence relative to machining and grinding, and verification requirements.
Upload a Drawing
Quality, Metrology & Documentation
Precision inspection, metrology, and quality documentation aligned to drawing-defined critical dimensions and the agreed inspection plan. Identify datums, tolerances, measurement methods, reporting format, traceability requirements, revision level, and any customer-specific acceptance criteria.
Upload a Drawing
Prototyping & Low-Volume Production
Rapid prototyping and low-volume manufacturing for teams validating geometry, fit, process assumptions, or early production requirements. Share the latest drawing and model, quantity range, material, critical dimensions, surface requirements, inspection needs, and target delivery date.
Upload a DrawingMold Lifters: Material Options Verified Against Your Drawing

Pre-Hardened Tool Steel
A practical choice for mold lifter bodies and support components when stable machining and balanced strength are required. Confirm supplied hardness, critical surfaces, machining allowance and any final grinding requirements against the drawing.

Through-Hardening Tool Steel
Used where wear resistance and load-bearing performance depend on a specified hardening route. Review heat-treatment distortion risk, finish-machining stock, EDM sequence and critical-dimension inspection before production is committed.

Hot-Work Tool Steel
Considered for lifter components exposed to elevated molding temperatures or repeated thermal cycling. Material grade, heat-treatment condition, surface requirements and cooling-related geometry should be evaluated from the application and drawing.

Stainless Tool Steel
Selected when corrosion resistance is relevant to the resin, molding environment or maintenance plan. Grade selection must account for achievable hardness, machining behavior, EDM finish and the drawing’s dimensional and surface requirements.

High-Speed Tool Steel
Applicable to localized wear features where the drawing specifies a high-hardness material solution. Machining and grinding strategy, heat-treatment sequence, wire-EDM access and verification points require review before quotation.
Mold Lifters: Supported Machining and EDM Processes

CNC Milling
CNC milling establishes lifter bodies, pockets, guide features, and accessible forming geometry. Tool access, datum locations, machining allowance, and subsequent EDM or grinding requirements are reviewed before the route is confirmed.

CNC Turning
CNC turning supports rotational lifter features, pins, sleeves, and locating details where the drawing calls for them. Concentricity requirements, bearing interfaces, material condition, and finishing allowances guide process planning and inspection.

Wire EDM
Wire EDM cuts precise profiles, slots, and internal contours where conventional tools cannot reach cleanly. The programmed wire path, start-hole access, corner conditions, and required finish are evaluated against the lifter drawing.

Sinker EDM
Sinker EDM forms deep ribs, sharp internal features, and cavity details requiring an electrode strategy. Electrode design, spark allowance, surface expectations, and post-EDM finishing are coordinated with the specified geometry.


Fitting and Inspection
Fitting and inspection verify how mold lifters relate to adjacent components, critical dimensions, and drawing revisions. The final documentation follows the agreed inspection plan and order requirements, with results communicated for review.
Mold Lifters: Hardware and Identification Options

Guide Elements
Guide pins, bushes, and locating features can be supplied as drawing-defined companion details for mold lifters, helping control alignment through assembly and ejection travel where the approved design requires them.

Retaining Fasteners
Specify screws, dowel locations, threads, and retention interfaces with the component drawing. Fastener selection should account for access, service requirements, load path, and the material or heat-treatment sequence.

Return Springs
Spring pockets and drawing-specified return springs can support controlled component return within the mold assembly. Review travel, preload, clearance, and installation access together before committing to the machining route.

Wear Plates
Wear plates, gibs, and contact pads may be added where the design calls for managed sliding contact. Material, hardness, lubrication provisions, and grinding stock require review alongside the mating surfaces.

Part Marking
Part numbers, revision identifiers, and orientation marks can be applied when specified, supporting assembly control and replacement-part traceability. Confirm marking location and method so critical surfaces and fits remain protected.

Inspection Labels
Inspection labels, packaging labels, and drawing-linked identification can be prepared to match the agreed delivery and documentation plan. Provide the required fields, revision status, and report expectations with the RFQ.
About SUUXIANG Mold Lifters
SUUXIANG is the public-facing brand of Dongguan SuuXiang Precision Mold Co., Ltd., established in 2010 in Chang’an Town, Dongguan, Guangdong, China. We help international engineering, sourcing, and quality teams turn controlled drawings and specifications into inspected precision mold components, custom CNC parts, connector tooling, and die components.
For mold lifters and related tooling components, our process planning can combine CNC milling and turning, multi-axis machining, wire EDM, sinker EDM, precision grinding, fitting, and inspection. Each route begins with a practical review of critical dimensions, datums, material and heat-treatment requirements, surface requirements, machining access, and inspection expectations.
What distinguishes SUUXIANG is disciplined coordination before production commitments: DFM discussion, documented revision control, process selection around functional features, and inspection aligned with the agreed order requirements. Provide your 2D drawing, 3D model when available, quantity, material, quality priorities, and delivery target for a focused RFQ review.

Mold Lifters: SUUXIANG’s Drawing-Based Sourcing Approach
DFM and Datum Review
SUUXIANG begins mold lifter work with the drawing, 3D model, molding application, and critical dimensions. The review aligns datum selection, undercut release requirements, shutoff-related geometry, machining access, and tolerance stack before a process route or quotation is discussed.
- Identify critical-to-quality dimensions and functional datums
- Review lifter travel, undercut geometry, and adjacent component clearance
- Flag tool-access, material, heat-treatment, and surface requirements
- Keep drawing revisions visible during project coordination

Machining and EDM Strategy
A mold lifter often combines angled forms, detailed profiles, and surfaces that require a deliberate CNC, wire EDM, sinker EDM, or multi-axis approach. SUUXIANG plans the route around geometry, access, electrode needs, stock condition, and the dimensions that control fit and release.
- Match process selection to geometry and feature accessibility
- Define wire paths or electrode strategy where required
- Consider machining sequence around heat treatment and distortion risk
- Preserve allowances for subsequent grinding or fitting

Grinding and Fitting Control
Lifter performance depends on how working surfaces relate after machining, EDM, heat treatment, and finishing. SUUXIANG reviews grinding stock, contact surfaces, sliding interfaces, and mating-part relationships so fitting requirements are understood as functional controls rather than unspecified shop adjustments.
- Review grinding allowance on critical mating surfaces
- Clarify sliding, contact, and shutoff-related interfaces
- Coordinate part condition with mating-component information
- Address fitting expectations before production release

Inspection Planning
Inspection planning for mold lifters should focus on the dimensions and relationships that affect assembly and motion. SUUXIANG aligns the inspection method and reporting needs with the approved drawing, datums, tolerance priorities, and order requirements, maintaining traceable revision control through delivery coordination.
- Connect measurement points to drawing datums and critical features
- Confirm required inspection records before production begins
- Distinguish functional dimensions from general dimensions
- Match final documentation to the verified inspection plan

Mold Lifters: SUUXIANG vs. Typical General Machining Suppliers
Compare the engineering controls that keep lifter requirements visible from drawing review through inspection planning and delivery coordination.
← Swipe left or right to view →
Mold Lifters: From Drawing Review to Delivery Coordination
A controlled workflow aligns DFM, machining, EDM, grinding, fitting and inspection requirements before shipment is coordinated.
Review Drawings and Requirements
Share 2D drawings, 3D models, material, quantity and quality needs so critical dimensions, datums, surfaces and application context can be reviewed.
Confirm DFM and Process
SUUXIANG evaluates machining access, tolerance stack, heat-treatment sequence, EDM requirements, grinding allowance and inspection expectations before production commitments are made.
Machine Critical Component Features
CNC milling, turning, multi-axis or micro-machining routes are selected according to geometry, material condition, tool access and designated datum strategy.
Apply EDM and Grinding
Wire EDM, sinker EDM and precision grinding address profiles, details and finished surfaces where the approved process plan requires those operations.
Fit, Inspect and Document
Components are fitted as required, inspected against the agreed plan, and documented with revision-controlled information matching the order requirements.
Pack and Coordinate Shipment
After inspection release, parts are prepared for packing and shipment coordination, with delivery information kept visible through the final project stage.
Start Your Mold Lifters RFQ
Provide the drawing, technical priorities, and delivery context needed for a focused manufacturing review.
Upload Drawings and Models
Send the latest 2D drawing and, when available, 3D model for mold lifters, including revision status, assembly context, and applicable notes.
Define Materials and Quantities
Specify material grade, heat-treatment requirements, quantity, and any approved alternatives so the proposed CNC, EDM, and grinding route can be reviewed appropriately.
Identify Critical Requirements
Highlight critical dimensions, datums, surface requirements, mating features, and functional risks that influence machining access, electrode strategy, fitting, and tolerance control.
Set Inspection and Delivery Needs
State required inspection reports, measurement methods, traceability expectations, target delivery date, and any packaging or project milestones affecting coordination before quotation.
Customer Reference Publication Controls
Verified Mold Lifters Project Outcomes
Customer-approved case pending validation: document the drawing revision, quantity, critical dimensions, inspection evidence, and measurable production outcome before publication.
Customer-approved case pending validation: include the mold lifter configuration, process route, delivery scope, and a buyer-approved result supported by project records.
Customer-approved case pending validation: confirm quoted quantities, dimensional priorities, inspection method, and the final outcome with the customer before using this testimonial.
The Complete Buyer’s Guide to Mold Lifters
Practical answers for buyers preparing drawing-based requests for custom mold lifter components and related tooling work.
Can SUUXIANG quote custom mold lifters from our drawing?
What is the MOQ for custom mold lifters?
How long does a mold lifter sample or production order take?
What files should we submit for a mold lifters RFQ?
Can SUUXIANG provide inspection reports for mold lifters?
How are drawing revisions handled after we submit an RFQ?
What material and heat-treatment information is needed?
Can SUUXIANG support payment, shipping, and IP requirements for international orders?
The Complete Buyer’s Guide to mold lifters
Use this decision framework to specify mold lifters, compare design and manufacturing criteria, evaluate drawing-based suppliers, and avoid the fit, material, tolerance, and validation mistakes that disrupt tooling programs.
1. What Are mold lifters?
Two coordinated motions define injection-mold lifters: ejector-plate travel drives the lifter upward while its angled path pulls the forming surface laterally away from an internal undercut. The molded feature must clear that lateral direction before the part can leave the core; lifters therefore suit ejector-side undercuts that can release during ejection (https://www.fictiv.com/articles/injection-molding-sliders-lifters-vs-handloads).
Four functional elements should appear on the assembly drawing: a lifter body, the part-forming surface, guide or support features that control the angled travel, and a positive return path for mold closing. Datum references, clearance around the pocket, contact faces, wear provisions, and the return sequence need review with the part geometry rather than being treated as generic hardware.
Three selection routes are typical: use a lifter when ejector-driven diagonal travel clears the feature; use a slide when the feature needs side action before ejection or greater lateral travel; use a hand-loaded insert when low volume can justify manual handling. The decision should follow undercut direction, stroke, projected molding load, tool-access constraints, cycle requirements, and the inspection plan.
2. How mold lifters Evolved
Two linked motions—ejection travel and lateral clearance—made the basic angled lifter a practical alternative where an undercut could not release straight from the core. Early concepts were commonly purpose-built around a particular part geometry, so fit-up depended heavily on the moldmaker’s alignment, support, and return details. https://www.fictiv.com/articles/injection-molding-sliders-and-lifters-vs-handloads
Three recurring production concerns pushed lifters toward more engineered assemblies: repeatable guidance, controlled wear surfaces, and replaceable elements. Because a lifter repeatedly enters and exits a metal block, abrasion-resistant hardened steel is often considered for the sliding interface; material and heat-treatment choices still require drawing-level review. https://www.fictiv.com/articles/injection-molding-sliders-and-lifters-vs-handloads
1 compact mold layout can turn a simple angled component into a system-level decision. Buyers should review guide length, bearing areas, lubrication access, return position, cooling-channel conflicts, grinding stock, and replacement access before release; a lifter that clears the part but cannot be inspected or serviced efficiently can raise tooling downtime.
3. Types of mold lifters
Two lifter decisions govern the preliminary concept: whether the forming tip is integral with its body, and whether the moving member fits the available ejector-side envelope. Map the undercut’s release direction before selecting a form.
| Type | Suitable Geometry | Space And Rigidity | Maintenance Tradeoff |
|---|---|---|---|
| Integral | Compact undercut | Simple envelope; rigid body | Replace whole member |
| Non-integral | Complex forming tip | Needs insert retention | Replace worn tip |
| Cylindrical | Narrow local feature | Round guide envelope | Simple fitting |
| T-shaped | Broad forming face | More plate space; stronger support | More fitting surfaces |
| Rack-driven or cooled | Constrained or thermal-sensitive area | Layout-specific support | More service points |
Integral And Non-Integral
Integral lifters combine body and forming feature, limiting joint movement and simplifying maintenance when the undercut is compact. Non-integral designs separate the forming insert, making replacement practical for wear-prone or complex profiles.
Selection starts with the molding load, insert access, and replacement cost; the drawing should identify the retained feature and datum relationship.
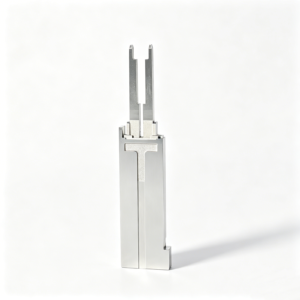
Cylindrical And T-Shaped
Cylindrical lifters suit narrow, localized undercuts where a round guide envelope is available. T-shaped forms offer a broader supporting section for larger forming faces, but consume more plate space and require controlled fitting.
Rigidity should be assessed from unsupported length, side load, and the contact area of the forming face.
Special Layout Arrangements
Rack-driven arrangements can package motion where angled channels or plate space are constrained. Cooled lifters need sealing, flow-path access, and service planning; compact arrangements trade service access for a smaller footprint.
Each special layout needs assembly-clearance and maintenance checks before release.
4. Materials for mold lifters
Material selection for mold lifters is a system decision, not a grade-name shortcut. Specify contact load, sliding distance, resin, cavity environment, lubrication, and dimensional-stability requirements before choosing the body, forming insert, or guide interface.
| Lifter Area | Selection Focus | Typical Decision |
|---|---|---|
| Body | Load and stiffness | Tool steel with suitable heat treatment |
| Forming surface | Resin wear and finish | Hardened or replaceable insert |
| Wear interface | Sliding distance and lubrication | Matched hardened surfaces or coating |
| Guide component | Alignment and friction | Hardened, finish-controlled guide |
Match Material To Function
Hardened tool steel is commonly used where a lifter repeatedly enters and exits a metal block because abrasion resistance matters (https://www.fictiv.com/articles/injection-molding-sliders-and-lifters-vs-handloads). Use separate, replaceable forming inserts when wear or repair risk is concentrated at the cavity surface.
Control Wear And Corrosion
Abrasive filled resins increase wear at forming faces and sliding interfaces, so hardness, finish, lubrication compatibility, and justified coatings must be reviewed together. Corrosion-resistant steel can be appropriate for humid, corrosive, or water-exposed cavity environments, subject to the required hardness and machining route.
Specify Treatment And Repair

Heat treatment should be defined with machining and grinding allowance, distortion risk, and final inspection datums. Production volume determines whether a repairable insert-and-body design is preferable to an integral lifter, particularly where a worn contact surface can be replaced without remaking the complete component.
5. Custom mold lifters From Drawings
SUUXIANG reviews custom mold lifters against the complete mold interface, not an isolated part print. Functional requirements should define movement, molding contact, wear surfaces, and inspection datums before machining is quoted.
Define Functional Geometry
The 2D drawing should specify lifter angle, head or forming geometry, body profile, required travel, and ejector-plate fit. Nominate molding clearances, shutoff surfaces, datum references, and allowable interference with adjacent inserts.
The 3D model should show the lifter’s full swept path and mating geometry. Resin grade, undercut depth, and target cycle conditions help assess load, wear, venting, and release risks.
Specify Process-Critical Features
Heat-treatment drawings should identify hardened zones and any areas requiring post-heat-treatment grinding or EDM. Surface-finish requirements belong on functional faces, bores, and sliding interfaces rather than as a blanket cosmetic note.
Cooling provisions require channel layout, connection constraints, and sealing details when applicable. Identification marking should state location, method, character size, and whether it must remain outside molding or sliding surfaces.
Submit A Reviewable RFQ
An RFQ should include revision-controlled 2D drawings, native or neutral 3D data, material specification, quantity, and inspection expectations. Provide ejector plates, guide blocks, return components, cavity or core inserts, and adjacent-component models where fit matters.
Cosmetic branding rarely changes lifter function; traceable part numbers and revision marks often do. SUUXIANG can use the supplied package to review tool access, EDM strategy, grinding stock, and inspection plan.
6. Construction Quality in mold lifters
Three construction interfaces govern lifter reliability: the angled travel path, bearing support, and return position. Review them as an assembly, because a correct individual dimension can still bind after heat treatment or fitting.
Geometry And Support
Two matched angle surfaces need controlled geometry, adequate bearing length, and robust radii at section changes. Unsupported slender sections, abrupt transitions, and poor datum alignment promote deflection or galling.
One drawing review should identify the travel datum, contact faces, clearance zones, and grinding allowance before machining.
Wear And Motion
Hardened wear surfaces and the specified heat-treatment sequence must suit the contact load and finishing route. Burrs at EDM, milled, or ground edges can score mating faces and obstruct free travel.
One functional assembly check should confirm smooth full stroke, alignment at both ends, and positive return to the intended closed position.
Evidence To Request
Four records make acceptance more defensible: material traceability where required, dimensional inspection results, hardness verification, and functional assembly evidence. The report should identify measured datums, instruments, acceptance criteria, and any deviations.
Each revision must carry a drawing revision, part identifier, and inspection-plan status; SUUXIANG should align final records to the approved order requirements.
- Material certificate when specified
- Critical-dimension report
- Hardness result and location
- Assembly stroke and return check
7. Choosing a mold lifter Manufacturer
Two suppliers can quote the same drawing yet control different risks. Compare their documented review, process route, measurement plan, revision discipline, and shipment preparation before releasing mold lifters.
| Evaluation Area | Question To Ask | Evidence To Request |
|---|---|---|
| Engineering | Is DFM feedback issued before release? | Marked drawing or review record |
| Capability | Which machining and EDM steps are planned? | Process route and access notes |
| Quality | How are critical dimensions verified? | Inspection plan and first-article report |
| Delivery | What changes the committed lead time? | Milestone schedule and revision log |
Drawing Review And DFM
A 2D drawing and 3D model should trigger a written review of datums, critical dimensions, lifter angle, tool access, EDM features, and grinding stock.
Ask whether deviations are identified before machining and recorded against the drawing revision.
Process And Material Evidence
Each quoted route should state milling, turning, wire EDM, sinker EDM, grinding, fitting, material sourcing, and heat-treatment coordination only where required.
Request material traceability and confirmation of heat-treatment sequence; do not assume a stated material arrives at final hardness.
Inspection And Program Control
A first article should be measured against agreed critical dimensions and inspection methods before repeat production.
Ask who approves changes, how revised files are acknowledged, what packaging protects finished faces, and which dates distinguish review, production, inspection, and dispatch.
8. Common mold lifter Buying Mistakes
Eight release checks prevent the most expensive mold lifters purchasing errors: a drawing can define geometry yet omit the operating conditions that govern motion, wear, and inspection.
Angle Without Release Study
One lifter angle does not prove an undercut will clear. Request a sectioned motion study showing release distance, steel-safe clearance, and interference through full ejector stroke.
Missing Process Inputs
Two omitted inputs—resin and annual volume—can invalidate a reasonable-looking design. State resin grade, filled versus unfilled condition, projected cycles, molding pressure context, and expected side load.
Cost-Only Component Selection
Three choices require a documented basis: material, heat-treatment condition, and bearing surface. Ask for the material specification, hardness requirement where applicable, lubrication method, and maintenance-access drawing before release.
Uncontrolled Fit And Motion
Two unclear items cause assembly risk: functional tolerances and real motion. Release an assembly drawing with datums, mating clearances, lubrication points, and an interference-free stroke validation; define the inspection record required.
9. Launching a Tooling Program
A tooling launch starts when design, sourcing, quality, and mold-build owners agree on one controlled data package. 2D drawings, 3D CAD, resin, molding conditions, undercuts, and revision status must travel together.
Review The Molding Function
Each undercut requires a defined release direction, lifter travel, shutoff condition, and ejection sequence. Design should identify mating features; mold-build should flag tool access, interference, EDM needs, and fitting risks before quotation.
Lock The Manufacturing Baseline
Critical dimensions need datums, tolerances, material, heat-treatment sequence, surface requirements, and an inspection method. Sourcing approves the quotation and schedule only after quality and the supplier confirm the DFM assumptions and revision-controlled scope.
Validate And Release Production
First-article inspection should compare agreed critical features against the approved drawing and report plan. Mold trial results, lifter movement, part release, changes, spare parts, lubrication, and maintenance expectations should be recorded before production approval.
10. mold lifters Pricing and Cost
2D drawings, 3D models, material grade, heat treatment, quantity, datums, surface callouts, and inspection requirements are the inputs needed for a defensible quote. Missing lifter angle, undercut geometry, or mating-component context can add clarification cycles and change the process route.
1 early DFM review can reduce rework by identifying difficult tool access, electrode needs, wire paths, and grinding stock before release. Consolidating compatible lifters and simplifying noncritical geometry usually lowers total program cost more reliably than requesting an unsupported unit-price target.
| Sourcing scenario | Design and process content | Inspection and quantity | Typical lead-time effect |
|---|---|---|---|
| Prototype | Complex geometry; CNC, EDM, fitting | Critical dimensions; 1–5 pieces | Programming and setup dominate |
| Low volume | Moderate complexity; CNC plus selective EDM | Dimensional report; 10–50 pieces | Setup spread across order |
| Production-oriented | Stable design; repeatable CNC, EDM, grinding | Defined plan; 50+ pieces | Planning and batching improve flow |
| Cost escalators | Hardened material, heat treatment, tight datums | Added reporting or functional checks | May require extra operations |
Upload Your Drawing for Mold Lifters Review
Share material, quantity, critical dimensions, quality needs, application context and delivery target for a disciplined drawing-based project review.