
Precision Lapping for Drawing-Based Parts
Submit your drawing for precision lapping review, DFM feedback, process planning, and inspection requirements aligned to your critical features.
Representative Components for Precision Lapping Projects





Precision Lapping Component Families and Quotation
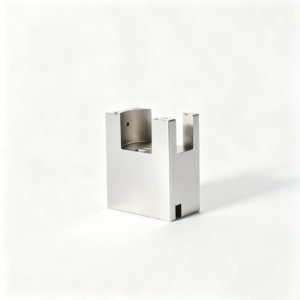








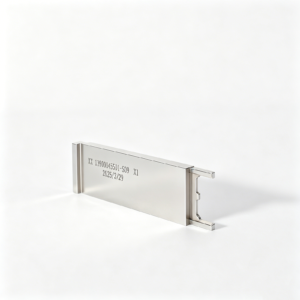
Why Engineering Teams Choose SUUXIANG for Precision Lapping
Drawing-driven planning that keeps critical requirements, process decisions, and inspection expectations visible before production begins.
Drawing-First DFM Review
We review drawings, models, material requirements, datums, and critical features to identify manufacturability questions before quotation or production planning.
Integrated Process Planning
CNC machining, EDM, grinding, fitting, and precision lapping are considered together to select practical sequences, allowances, and feature-access strategies.
Critical Dimensions Prioritized
Critical-to-quality dimensions, surface requirements, and tolerance relationships guide process discussions, helping teams focus controls where function and assembly depend on them.
Inspection Plan Alignment
Inspection methods and reporting expectations are discussed against the drawing so final documentation can align with the verified order requirements.
Revision Visibility
Revision details, manufacturing questions, and delivery coordination remain traceable, supporting clearer communication between engineering, sourcing, quality, and project teams.
Precision Components and Tooling Families
Drawing-driven process routes for configurable parts and tooling, reviewed for critical dimensions, manufacturability, inspection requirements and delivery needs.

CNC Machining Services
Precision CNC machining services for drawing-based parts requiring an appropriate combination of milling, turning, EDM, grinding and inspection. Submit drawings, material, quantity, critical dimensions and quality requirements so the process route can be reviewed before quotation.
Upload a Drawing
CNC Milling
Custom CNC milling services for prismatic parts, plates, inserts and features that depend on controlled datum relationships. Tool access, corner geometry, wall rigidity, machining allowance and surface requirements should be reviewed against the drawing before production planning.
Upload a Drawing
CNC Turning
Precision CNC turning services for rotational components, shafts, bushings, sleeves and threaded features. Diameter tolerances, concentricity, runout, datum selection, material condition and secondary machining needs determine the practical route and inspection approach.
Upload a Drawing
5-Axis Machining
5-axis CNC machining for complex geometries where multi-angle access can reduce setups or reach difficult features. The drawing review considers tool reach, fixture strategy, surface transitions, tolerance relationships and whether EDM or grinding is required afterward.
Upload a Drawing
Swiss & Micro Machining
Swiss machining and micro machining for small, detailed components where feature access, slender geometry and handling require careful process planning. Share critical dimensions, material, quantities and mating context to assess suitable machining and inspection methods.
Upload a Drawing
Wire & Sinker EDM
Wire EDM and sinker EDM services for hardened details, narrow slots, sharp internal geometry and features not suited to conventional cutting alone. Electrode strategy, wire path, flushing, recast-layer expectations and finishing allowances are defined from the drawing requirements.
Upload a Drawing
Precision Grinding
Precision surface and profile grinding for flatness, parallelism, profiles and controlled final stock removal. Grinding stock, heat-treatment sequence, datum condition, wheel access and inspection method need to be established before final dimensions are committed.
Upload a Drawing
Mold Core & Cavity Inserts
Precision mold core and cavity inserts produced from customer drawings for injection-tooling applications. Material, heat treatment, cavity detail, shutoff geometry, cooling interfaces, EDM requirements and critical mating dimensions guide the manufacturing and inspection plan.
Upload a Drawing
Ejector & Ejection Components
Ejector pins, sleeves and ejection components manufactured as configurable mold-component families. Fit, clearance, hardness, surface condition, stroke-related interfaces and dimensional relationships with the mating mold assembly should be supplied for review.
Upload a Drawing
Core Pins, Guide & Locating Components
Core pins, guide pins and locating components made to drawing-defined geometry and fit requirements. Functional datums, mating bores, alignment features, wear considerations, material condition and inspection priorities determine the suitable process sequence.
Upload a Drawing
Slides, Lifters, Gates & Mold Accessories
Mold slides, lifters, gates and accessories for tooling assemblies with moving or flow-critical interfaces. Design review focuses on travel geometry, shutoffs, bearing surfaces, gating details, fitting allowances and relationships to the surrounding mold components.
Upload a Drawing
Connector Mold Components
Precision connector mold components for tooling that forms fine-pitch, terminal-related or alignment-sensitive connector features. Drawing review addresses small details, datum control, EDM strategy, wear surfaces, polishing needs and inspection evidence for critical features.
Upload a Drawing
Stamping Die Components
Precision stamping die components for drawing-based die assemblies, including punches, dies, guide elements and forming-related details. Material, hardness, edge condition, clearance relationships, grinding strategy and mating-component context should be defined before production.
Upload a Drawing
Injection, MIM, CIM & Overmolding Tooling
Injection, MIM, CIM and overmolding tooling components supported where requirements fall within verified production scope. Process planning evaluates material, cavity or insert geometry, molding interfaces, thermal treatment, EDM and grinding needs, plus drawing-defined quality expectations.
Upload a Drawing
Machining Materials
CNC machining materials selected against the drawing, application and required manufacturing route. Specify the designated grade, material condition, hardness or heat-treatment requirement, corrosion considerations and any traceability needs before quotation and production.
Upload a Drawing
Surface Finishes & Heat Treatment
Surface finishing and heat treatment planned around functional surfaces, dimensional stability and downstream fitting. Define finish type, roughness priorities, coating or treatment requirements, masking needs and the dimensional features affected by each post-machining process.
Upload a Drawing
Quality, Metrology & Documentation
Precision inspection, metrology and quality documentation aligned with the order and verified inspection plan. Identify critical dimensions, datums, measurement methods, reporting format, material records and revision requirements early so deliverables match the production scope.
Upload a Drawing
Prototyping & Low-Volume Production
Rapid prototyping and low-volume manufacturing for drawing-based parts that need controlled process selection before larger commitments. Provide the drawing, model, material, quantity, delivery target and inspection needs to evaluate manufacturability, revision risk and suitable production routing.
Upload a DrawingMaterials Considered for Precision Lapping

Hardened Tool Steel
Common for mold inserts, punches, and wear components. Its high hardness supports durable working surfaces, while heat-treatment condition, grinding stock, and required flatness must be reviewed before final finishing.

Stainless Steel
Used for corrosion-conscious mold, connector, and custom precision parts. Alloy grade and hardness affect machinability and surface response, so passivation needs, mating conditions, and inspection priorities should accompany the drawing.

Tungsten Carbide
Selected for high-wear pins, dies, and cutting features where rigidity matters. Its very hard, brittle character calls for careful handling, appropriate EDM or grinding strategy, and clear edge-condition requirements.

Aluminum Alloys
Often specified for lightweight fixtures, prototype tooling, and machined housings. The softer material can be sensitive to clamping and surface damage, making alloy designation, coating requirements, and datum strategy important to review.

Engineering Plastics
Used for insulating fixtures, guides, and low-friction functional components. Their softer, temperature-sensitive behavior can influence finishing and measurement, so resin grade, operating environment, and dimensional priorities should be defined.
Precision Lapping Process Routes for Drawing-Based Parts


Wire EDM
Wire EDM can be considered for profiles, narrow features and hardened-workpiece geometry where a controlled wire path is appropriate. The required contour, start-hole access, corner condition and downstream finishing requirements guide feasibility review.

Sinker EDM
Sinker EDM may support cavities, detailed forms and features beyond practical cutting-tool access. Electrode design, burn allowance, surface requirement and the relationship to later fitting or grinding are evaluated from the drawing.

Precision Grinding
Precision grinding is planned where controlled dimensions, flatness-related features or surface requirements call for a grinding route. Material condition, heat-treatment sequence, grinding stock and inspection method must be confirmed for the project.

Fitting Assembly
Fitting addresses the functional relationship between mating mold or tooling components after machining. Clearance, alignment, contact areas and any handwork expectations are defined against drawings, assembly context and agreed acceptance criteria.

Inspection Control
Inspection planning links critical dimensions, datums and reporting requirements to the production route. SUUXIANG aligns measurement methods, revision status and final documentation with the order-specific inspection plan before release.
Mold Tooling Accessories and Component Features

Guide Elements
Guide pins, bushings, and locating elements support repeatable mold alignment. Drawing review should define fit relationships, datum references, hardness condition, lubrication requirements, and the inspection method for critical mating surfaces.

Ejection Parts
Ejector pins, sleeves, plates, and related ejection parts are evaluated for clearance, stroke, guidance, and mating geometry. SUUXIANG reviews critical dimensions and finishing requirements before selecting an appropriate machining and grinding route.

Gate Components
Gate inserts and related flow-control features require close attention to edge condition, surface requirement, material treatment, and access for machining or EDM. Provide molding context and mating-part information with the RFQ.

Slides and Lifters
Slides, lifters, wear features, and locating interfaces are assessed as functional assemblies rather than isolated parts. Include travel direction, contact areas, assembly datums, and heat-treatment sequence to support a practical manufacturing review.

Mold Accessories
Custom mold accessories can include retainers, stops, spacers, locking features, and mounting elements. A complete drawing package helps confirm thread details, tolerances, surface priorities, and whether fitting or inspection documentation is required.

Connector Tooling
Connector-tooling components often combine small features, precise locating geometry, and demanding mating relationships. Submit 2D drawings, models, material requirements, and critical-dimension priorities so the process route can be evaluated responsibly.
About SUUXIANG Precision Lapping
SUUXIANG is the sole public-facing brand of Dongguan SuuXiang Precision Mold Co., Ltd., established in 2010 and based in Chang’an Town, Dongguan, Guangdong, China. XiaoCheng Huang is the founder and legal representative. We help international teams turn drawings, models, and specifications into inspected custom CNC parts, precision mold components, connector tooling, and die components.
Our work is planned around the features that matter: datums, critical dimensions, machining access, EDM requirements, grinding allowance, heat-treatment sequence, and inspection method. CNC machining, EDM, grinding, fitting, and quality control are coordinated as a manufacturing workflow rather than quoted as disconnected operations.
For precision lapping and related component requirements, SUUXIANG begins with DFM and drawing review before production commitments. This gives buyers a clearer basis for discussing material, quantity, revision control, surface priorities, reporting needs, and delivery expectations before the process route is confirmed.

Precision Lapping Planning for Critical Features
DFM and Datum Review
Precision lapping planning starts with the drawing: functional datums, critical dimensions, mating relationships, surface requirements and measurement references. SUUXIANG reviews these inputs before quoting so the proposed route reflects the part’s actual inspection and assembly priorities.
- Identify critical-to-quality dimensions and datum relationships
- Review tolerance stack, surface callouts and accessible reference faces
- Flag drawing gaps or manufacturability risks before production commitments

EDM and Grinding Strategy
For mold and connector-tooling features, EDM and grinding decisions must support the final functional geometry. SUUXIANG evaluates tool access, electrode requirements, wire paths, hardened-condition work and finishing sequence to avoid leaving critical surfaces dependent on an unsuitable earlier operation.
- Assess wire-EDM access for profiles, slots and internal geometry
- Define electrode strategy where sinker EDM is appropriate
- Align grinding operations with datum and final-surface requirements

Machining Allowance Planning
Controlled stock allocation gives later processes room to establish the required surface and geometry without overworking the part. SUUXIANG considers machining allowance, heat-treatment sequence, distortion risk and finishing access when planning precision lapping and related grinding operations.
- Reserve finishing stock on surfaces requiring final correction
- Consider heat treatment before final EDM or grinding decisions
- Confirm whether lapping supports the stated functional requirement

Inspection and Revision Control
Inspection planning should follow the drawing’s critical features, not a generic checklist. SUUXIANG aligns measurement methods, reporting expectations and revision status with the order so engineering, sourcing and quality teams can review the same production basis before shipment.
- Agree inspection points and report requirements during RFQ review
- Maintain visible drawing and revision-control references
- Match final documentation to the verified inspection plan

Precision Lapping Planning Beyond Generic Quoting
Compare the project controls that help teams evaluate drawing-based precision lapping work before production commitments.
← Swipe left or right to view →
Precision Lapping: From Drawing Review to Shipment
Each route is confirmed against the drawing, critical dimensions, material condition, inspection requirements, and delivery priorities before production commitments are made.
Review RFQ Inputs
Share the 2D drawing, 3D model when available, material, quantity, application context, quality requirements, and target delivery date for an informed initial review.
Confirm DFM Strategy
SUUXIANG reviews datums, critical dimensions, tolerance stack, machining access, heat-treatment sequence, and the appropriate precision lapping, EDM, or grinding route before quotation.
Plan Controlled Production
After requirements are aligned, the team defines the process sequence, machining allowances, electrode or wire path needs, checkpoints, and revision-control requirements.
Machine Critical Features
CNC machining, EDM, grinding, fitting, and finishing are applied according to the confirmed process plan and the part features requiring controlled geometry or surfaces.
Inspect Pack Coordinate
Completed parts are inspected against the agreed plan, documented as required, packed for protection, and coordinated for shipment based on verified order and delivery details.
Start Your Precision Lapping Project
A drawing-led workflow for aligning manufacturability, quality expectations, production planning, and delivery documentation before work proceeds.
Submit Your Requirements
Share 2D drawings, 3D models when available, material, quantity, critical dimensions, surface priorities, target date, and inspection or reporting requirements.
Align Quote and Sampling
Review DFM findings, process options, datum strategy, lapping or grinding considerations, quotation scope, and any prototype, sample, or approval requirements.
Approve the Production Plan
Confirm the agreed drawing revision, material and heat-treatment sequence, machining allowances, inspection method, acceptance criteria, and delivery coordination before production starts.
Receive Inspected Parts
SUUXIANG coordinates machining, EDM, grinding, fitting, and inspection according to the approved plan, with final documentation matched to the verified inspection requirements.
Precision Lapping Quality Documentation and Certification Evidence
Customer Evidence Is Published Only When Verified
Approved customer testimonial evidence is being verified before publication. SUUXIANG does not publish named project outcomes, quantities, tolerances, or delivery results without customer permission and supporting production records.
Case-summary evidence is being prepared from verified drawing-review, machining, inspection, and delivery records. Published results will identify the applicable part scope, measurement basis, and permission status.
Customer feedback will be added only after the quoted outcome, supporting documentation, and attribution have been approved. For current project evaluation, submit the drawing, material, quantity, and inspection requirements.
Precision Lapping FAQ for RFQ Preparation
Clarify feasibility, documentation, commercial requirements, and the technical inputs needed for a drawing-based review.
Can SUUXIANG review my precision lapping drawing before quoting?
What information is needed for a precision lapping RFQ?
Is there a minimum order quantity for precision lapping parts?
Can I order samples before production?
How long does a precision lapping order take?
What materials and heat-treatment conditions can be reviewed?
Can SUUXIANG provide inspection reports for precision lapping components?
How are shipping, payment, and intellectual property handled?
The Complete Buyer’s Guide to precision lapping
Use this decision framework to specify precision lapping requirements, compare process options, assess supplier controls, and avoid quoting, tolerance, material, inspection, and lead-time mistakes when sourcing drawing-based precision components.
1. What Is precision lapping?
0.000001 inch is a published example of flatness reached under specialized lapping conditions, illustrating why precision lapping is a controlled abrasive-finishing operation rather than ordinary stock removal. It refines flatness, parallelism, thickness, and surface finish after milling, grinding, EDM, or heat treatment has established the basic geometry.
Micron-sized loose abrasive, carried in an oil- or water-based slurry across a conditioned lap plate, removes high points gradually under low pressure and speed. That averaging action is typically wet and can remove roughly 5 to 500 microns per side, but the correct allowance depends on material, part rigidity, initial condition, and final requirement. Source: https://www.trilap.net/post/what-is-precision-lapping
2 drawing questions usually determine whether lapping is justified: are opposing faces simultaneously critical for flatness or parallelism, and is a tight thickness-plus-finish requirement beyond an economical grinding or milling route? SUUXIANG should review datums, allowable stock, heat-treatment sequence, surface callouts, and inspection method before selecting lapping; a lapped finish is not automatically the lowest-cost answer.
2. Evolution of precision lapping
Two-surface hand lapping established the basic mechanism: loose abrasive carried between a workpiece and a conditioned lap selectively removes high points. Optical work extended the method where controlled form and fine finish mattered, making plate condition and abrasive size part of the process rather than shop-floor judgment alone.
Single-sided machines retained direct control of one reference face, while double-sided equipment processes both faces simultaneously in carriers. This production change made thickness and parallelism more repeatable across batches, but it also made loading, carrier condition, slurry delivery, pressure, and dwell time controlled variables. https://www.petersenprecision.com/capabilities/lapping-honing
Four inputs now belong in a drawing review: required flatness or parallelism, thickness stock to remove, surface-finish target, and the datum or face that governs function. Abrasive grade, material behavior, and process time jointly affect the result, so buyers should specify the inspection method and reporting need instead of treating precision lapping as a generic polishing note. https://www.accumet.com/precision-lapping-polishing
3. Types of precision lapping
Process selection starts with the functional surface: one accessible face, two opposing faces, or a specified contour. The drawing must define the controlled geometry, stock condition, finish target, and inspection datum.
| Variant | Best Surface | Primary Outcome | Tradeoff |
|---|---|---|---|
| Loose-abrasive | Single face or flat pair | Fine geometry control | Slower removal |
| Fixed-abrasive fine grinding | Opposed flat faces | Thickness consistency | Less localized flexibility |
| Polishing | Finished functional or cosmetic face | Lower roughness | Limited geometry correction |
| Shaped lapping | Convex or concave form | Controlled profile | Higher setup effort |
Single-Sided Lapping
Single-sided lapping suits a face that needs localized flatness or must retain an opposite-side feature. It offers direct fixture control, but handling and cycle time can limit throughput.
- RFQ: identify lapped face and datum
- State removal allowance and edge condition
- Provide flatness and Ra requirements
Double-Sided And Fine Grinding
Double-sided lapping processes both opposing faces together for thickness and parallelism control. Petersen Precision distinguishes loose-abrasive lapping from bonded-abrasive fine grinding, which generally favors repeatable higher-volume processing: https://www.petersenprecision.com/capabilities/lapping-honing
- RFQ: give finished thickness and parallelism
- Specify carrier-sensitive part geometry
- State batch quantity and allowable stock
Polishing And Shaped Lapping
Polishing refines appearance or low roughness after geometry is established; it should not substitute for a flatness callout. Controlled-curvature lapping suits defined convex or concave forms, but requires profile data and more development control.
- RFQ: provide profile tolerance and reference radius
- Identify cosmetic versus functional finish
- Include mating-surface context
4. Materials for precision lapping
Material response sets the lapping recipe before a tolerance is quoted. Hardness, brittleness, heat sensitivity, section thickness, and incoming grind or EDM condition determine abrasive, carrier, pressure, and removal allowance.
| Material family | Primary lapping consideration | Typical control focus |
|---|---|---|
| Hardened steel, carbide | High hardness; abrasive and plate selection | Removal rate, flatness |
| Stainless, aluminum, titanium | Loading, smearing, thermal response | Carrier, low pressure |
| Ceramic, glass, silicon | Brittleness and edge damage | Fine abrasive, support |
| Engineering plastics | Compliance and heat sensitivity | Minimal pressure, trial |
Material Response
Hardened steels and carbides generally tolerate firmer support, while stainless steel, aluminum, titanium, and engineering plastics can load, smear, or distort under unsuitable slurry and pressure.
Ceramics, glass, and silicon are brittle; edge chipping, subsurface damage, and carrier support must be evaluated alongside finish.
Starting Condition And Trials
EDM recast layer, grinding direction, saw damage, and stock variation change the removal needed before a stable finish is possible.
Thin, large-area, brittle, heat-sensitive, or mixed-material parts merit a sample trial to confirm carrier design, removal rate, edge condition, and inspection method.
Evidence Before Production
A drawing should identify material grade, hardness or temper, starting thickness, flatness datum, finish target, and permitted stock removal.
A documented trial is especially prudent when geometry limits support or when a cosmetic surface has functional mating requirements.
5. Surface finish and secondary options
Precision lapping specifications should separate functional contact requirements from appearance. Put the controlling value, datum reference, inspection method, and acceptance condition on the drawing or RFQ before quoting.
| Requirement | Drawing Or RFQ Callout | Why It Matters |
|---|---|---|
| Surface roughness | Ra value, cutoff, surface ID | Controls functional texture |
| Geometry | Flatness, parallelism, datum | Controls mating behavior |
| Edges | Break size and burr limit | Protects assembly |
| Protection | Cleaning, packaging, traceability | Preserves verified condition |
Call Out Functional Surfaces
Ra, flatness, parallelism, and finished thickness control fit, sealing, preload, or electrical contact. Identify the applicable face, datum, measurement area, and whether the requirement applies before or after heat treatment.
Define Edges And Cleanliness
Edge condition should state deburr limits, allowable break, and whether sharp edges must remain for function. Cleaning and packaging should name contamination risks, corrosion protection, part separation, labeling, and lot or revision traceability.
Confirm Secondary Processing
Coating, passivation, plating, or polishing can change thickness, contact behavior, and measurement sequence. Specify the governing standard, mask areas, thickness range, cosmetic class, and whether the supplier must coordinate a compatible verified route.
6. Quality controls in precision lapping
Before release, the drawing must define the functional datum, measurement locations, and acceptance method. For precision lapping, geometry, material condition, and metrology form one control plan—not separate checks.
Datum And Stock Plan
0.01 mm of remaining stock can be decisive on thin or heat-treated parts. Specify the lapped face datum, pre-lap condition, stock allowance, and whether thickness is measured from opposed faces or a functional reference.
2 protected edges reduce chipping and rollover risk during handling. Identify chamfers, break-edge limits, unsupported areas, and any carrier contact zones before routing.
Process Condition Control
1 conditioned plate profile governs the geometry transferred to the work. Record plate condition, abrasive type and grit, slurry concentration, feed condition, carrier or fixture identification, and cleaning status by lot.
100% segregation of incompatible abrasives is prudent where scratch limits are critical. Clean carriers, plates, gauges, and packaging paths between material or grit changes to prevent embedded-particle contamination.
Inspection And Reporting
3 geometry results—flatness, parallelism, and thickness—should be tied to stated datums, sample quantity, instrument, resolution, and measurement locations. Measure roughness with the specified cutoff and direction; do not substitute visual finish for Ra evidence.
0.00001 in parallelism may require a method capable of resolving the requirement, but capability must be confirmed for the actual part. Agree the report format during drawing review; reference guidance: https://www.accumet.com/precision-lapping-polishing
7. Choosing a precision lapping supplier
Two suppliers may quote the same drawing yet use different datum control, stock allowance, and inspection logic. Choose precision lapping capability through documented planning rather than a claimed finish value.
| Evaluation Area | Ask For | Useful Evidence |
|---|---|---|
| Material traceability | How is the lot linked? | Material record and job traveler |
| Metrology | How are flatness and thickness verified? | Method, datum, and report sample |
| Process fit | What machine and fixture route applies? | Route rationale and first-article plan |
| Communication | Who controls revisions and status? | Named update cadence and change record |
Engineering Review
Before quotation, ask for a drawing-review response that identifies CTQ features, datum references, material condition, and lapping allowance.
One capable reply states whether single- or double-sided processing, carriers, and pre-machining are appropriate for the geometry.
- Which dimensions are measured before and after lapping?
- What stock and distortion risks are anticipated?
- Which revision controls govern the route?
Evidence And Sampling
First-article planning should define sample quantity, measurement method, acceptance criteria, and report format before production.
Current certificates, when required, should be requested for the specific site, process scope, material lot, and order—not assumed from a logo.
Delivery And Protection
Realistic lead times include material release, machining, lapping trials, inspection, report approval, and export-safe packaging.
Each shipment should identify part revision, quantity, lot linkage, and handling protection for finished faces.
8. Common precision lapping sourcing mistakes
Before purchase-order release, the drawing and inspection plan must define what lapping is expected to control. A finish operation cannot correct unsuitable geometry, missing stock, or an undefined acceptance method.
Treating Lapping As A Cure-All
1 process route cannot recover warped thin parts, inaccessible faces, or excessive pre-process error. The consequence is rework, yield loss, or a revised quote; confirm rigidity, datum strategy, and controlled grinding or machining allowance before release.
Leaving Requirements Unmeasurable
2 requirements—flatness and roughness—need a value, measurement area, datum, instrument or method, and sampling expectation. Without them, supplier and buyer may accept different results; add those criteria and identify functional versus nonfunctional surfaces before release.
Confusing Finish With Function
3 common errors are specifying polishing when a matte lapped texture is acceptable, tightening nonfunctional faces, and approving incomplete reports. These choices add cost or leave quality risk; state the required surface function, protect thin-part handling, and require dimensional, flatness, roughness, material, and revision evidence matched to the order.
9. From drawing review to production launch
A production launch starts with controlled inputs, not a quotation alone. For precision lapping, the drawing must connect functional surfaces to measurable acceptance before material is released.
Define Drawing Acceptance
2D drawings and native or neutral 3D CAD should identify revision, units, datums, critical surfaces, and mating context.
Each lapped face needs an acceptance method for flatness, parallelism, thickness, roughness, edge condition, and allowable stock removal.
Confirm Material And Route
Material grade, starting condition, hardness range, and heat-treatment sequence must be confirmed before allowance and process routing are agreed.
EDM, grinding, and lapping allowances require review against tool access, distortion risk, and reference datums after heat treatment.
Approve Evidence Before Pilot
One sample or first article should be approved against the agreed inspection plan before pilot production.
Each inspection record should carry part number, revision, lot identity, method, result, and disposition.
Control Repeat-Order Changes
Pilot and repeat orders require a single change owner on each side and written revision release.
Any mold core, connector insert, or stamping-die change must reassess mating geometry, electrodes, wire paths, heat treatment, and inspection scope.
10. precision lapping pricing and cost drivers
2 quote inputs determine whether precision lapping is a finishing step or a higher-risk development route: the controlled stock-removal allowance and the required flatness, parallelism, thickness, and Ra. SUUXIANG reviews the drawing, material condition, datum scheme, quantity, and inspection evidence before issuing a project-specific quote; no published unit price can represent every requirement.
1 consolidated lot normally spreads carrier, conditioning, setup, and first-article effort across more parts. Clear revision-controlled specifications, realistic allowances, and agreed inspection sampling reduce avoidable rework, sorting, expedited logistics, and quotation contingencies.
| Cost driver | Lower-cost condition | Cost increase trigger | Quantity effect |
|---|---|---|---|
| Part geometry | Stable, accessible faces | Thin, fragile, or difficult-to-handle parts | Dedicated handling is diluted across larger lots |
| Material and allowance | Known condition; controlled stock | Hardness variation or excess removal | More removal increases cycle time per batch |
| Tolerance and finish | Functional limits and defined Ra | Tighter thickness, flatness, or polish target | Inspection and process trials may rise |
| Setup and inspection | Complete drawing and sampling plan | Unclear datums, revisions, or 100% reporting | Repeatable lots reduce non-recurring effort |
| Lead time | Planned production window | Expedite or split deliveries | Consolidated releases reduce coordination cost |
Upload Your Drawing for a Precision Lapping Quote
Include 2D or 3D files, material, quantity, critical dimensions, inspection requirements, and target delivery date for a focused drawing review.