
Connector Housing Mold Inserts, Built From Your Drawing
DFM-led review of connector housing mold inserts coordinates critical dimensions, CNC, EDM, grinding, and inspection before production.
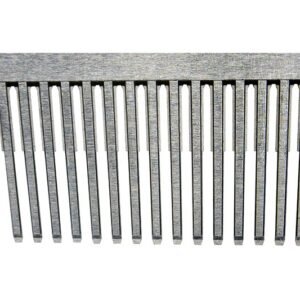
Featured Connector Housing Mold Insert Configurations








Related Configurable Components and RFQ Support










Why Choose SUUXIANG for Connector Housing Mold Inserts
A disciplined workflow that connects drawing review, process planning, controlled production, and inspection evidence.
Drawing Review First
Review drawings, models, materials, and functional requirements before quotation to identify manufacturability questions and clarify the production basis.
Critical Dimension Focus
Align critical dimensions, datums, surface requirements, and tolerance priorities with an appropriate machining, EDM, grinding, and inspection approach.
Process-Route Planning
Plan machining access, electrode strategy, wire paths, heat-treatment sequence, and grinding stock around the insert geometry and quality requirements.
Inspection Planning
Define inspection methods and reporting expectations against the order requirements, helping teams establish relevant evidence before production begins.
Revision Visibility
Maintain visible revision and delivery information so engineering, sourcing, and quality teams can coordinate changes through the manufacturing workflow.
Connector Mold Inserts and Tooling Components
Configurable component families and process routes organized around tool access, critical dimensions, material condition, and inspection requirements.

CNC Machining Services
Precision CNC machining services for drawing-based parts requiring coordinated milling, turning, EDM, grinding, fitting, and inspection. Process planning begins with critical dimensions, datums, material condition, surface requirements, quantity, and delivery expectations.
Upload a Drawing
CNC Milling
Custom CNC milling services for prismatic mold parts, inserts, plates, and complex profiles. Drawing review considers feature access, cutter reach, corner radii, workholding, datum setup, machining allowance, and dimensions that require inspection after subsequent processes.
Upload a Drawing
CNC Turning
Precision CNC turning services for rotational components such as pins, sleeves, bushings, shafts, and locating details. Requirements should define diameters, concentricity, runout, surface condition, material, heat-treatment sequence, and interfaces with mating tooling components.
Upload a Drawing
5-Axis Machining
5-axis CNC machining supports multi-face features, angled geometry, contoured forms, and reduced setup transitions where the drawing and part geometry justify the route. Tool access, clamping strategy, datum control, and downstream EDM or grinding requirements are reviewed before production.
Upload a Drawing
Swiss & Micro Machining
Swiss machining and micro machining support small, detailed cylindrical parts where diameter control, slender geometry, cross features, and handling require disciplined process planning. Submit the drawing, material, critical dimensions, quantity, and any mating or functional context for review.
Upload a Drawing
Wire & Sinker EDM
Wire EDM and sinker EDM services address hardened materials, narrow slots, internal corners, fine details, and forms with limited cutter access. Electrode strategy, wire path, flushing, recast-layer considerations, EDM allowance, and finish requirements should be defined during drawing review.
Upload a Drawing
Precision Grinding
Precision surface and profile grinding is used where flatness, parallelism, profile accuracy, surface condition, or final size must follow machining or heat treatment. Grinding stock, datum sequence, material condition, and inspection method need agreement before the process route is set.
Upload a Drawing
Mold Core & Cavity Inserts
Precision mold core and cavity inserts are manufactured from drawings for injection and related tooling applications. Review focuses on parting surfaces, cooling or venting interfaces, shutoffs, cavity detail, material and heat treatment, EDM needs, mating parts, and critical dimensions.
Upload a Drawing
Ejector & Ejection Components
Ejector pins, sleeves, and ejection components are configured around the mold’s ejection layout and functional interfaces. Drawings should identify diameters, fits, head geometry, surface needs, material condition, stroke-related considerations, and critical mating dimensions.
Upload a Drawing
Core Pins, Guide & Locating Components
Core pins, guide pins, and locating components are produced for repeatable positioning and controlled interfaces within mold assemblies. Requirements should clarify datum relationships, fits, concentricity, hardness or treatment sequence, wear considerations, and inspection priorities.
Upload a Drawing
Slides, Lifters, Gates & Mold Accessories
Mold slides, lifters, gates, and accessories are drawing-driven components requiring attention to motion interfaces, shutoffs, bearing surfaces, gate geometry, material condition, and assembly fit. Manufacturing planning may combine CNC machining, EDM, grinding, fitting, and inspection.
Upload a Drawing
Connector Mold Components
Precision connector mold components support connector-tooling details where fine features, pin locations, cavity geometry, mating interfaces, and repeatable alignment are central. Provide product context, material, critical dimensions, surface requirements, and quality documentation needs with the RFQ.
Upload a Drawing
Stamping Die Components
Precision stamping die components are planned around the drawing’s cutting, forming, guiding, and locating functions. Material, heat treatment, edge condition, clearances, grinding allowance, wire-EDM strategy, and mating-component relationships should be reviewed before commitment.
Upload a Drawing
Injection Mold Components for MIM, CIM & Overmolding
Injection, MIM, CIM, and overmolding tooling components are supported when requirements fall within verified production scope. A review should cover material flow-related geometry, inserts, shutoffs, parting conditions, material and treatment requirements, critical dimensions, and inspection expectations.
Upload a Drawing
Machining Materials
CNC machining materials are selected against the drawing, application, machining route, heat-treatment sequence, corrosion or wear needs, and inspection requirements. Confirm the specified grade, material condition, substitution rules, and any required traceability before production.
Upload a Drawing
Surface Finishes & Heat Treatment
Surface finishing and heat treatment are considered as part of the dimensional plan, not as isolated finishing steps. Specify surface condition, hardness or treatment requirements, masking or interface constraints, grinding allowance, and final inspection priorities in the RFQ.
Upload a Drawing
Quality, Metrology & Documentation
Precision inspection, metrology, and quality documentation are planned from the drawing’s critical dimensions, datum scheme, tolerances, and reporting requirements. Align on inspection methods, sampling or reporting expectations, revision status, material records, and order-specific documentation before production.
Upload a Drawing
Prototyping & Low-Volume Production
Rapid prototyping and low-volume manufacturing support drawing-based evaluation, tooling development, and controlled production quantities. Share the 2D drawing, 3D model when available, material, quantity, delivery target, critical features, and inspection needs for a practical process review.
Upload a DrawingMaterials for Connector Housing Mold Inserts

H13 Tool Steel
A heat-work tool steel often considered for inserts exposed to repeated thermal cycling or demanding molding conditions. Confirm the specified hardness, heat treatment, surface finish and EDM strategy for the actual connector-housing application.

S136 Stainless Steel
A corrosion-resistant mold steel option for inserts where polish quality, moisture exposure or resin-related corrosion may influence maintenance planning. Grade condition, hardness target and surface-treatment requirements should be defined in the RFQ.

P20 Prehardened Steel
A prehardened tool-steel option commonly evaluated for mold bases, larger insert features and development tooling. Its suitability depends on cavity geometry, expected production conditions, wear areas and the required machining and finishing route.

D2 Tool Steel
A high-wear tool steel candidate for localized features that require abrasion resistance. Review machinability, heat-treatment sequence, grinding stock and wire-EDM access before committing it to fine connector-tooling details or tight datums.

Copper Alloy Inserts
A high-conductivity material option for localized cooling or thermal-management features in connector housing molds. The final alloy and insert design should be reviewed for strength, wear exposure, mating surfaces and the intended machining process.
Connector Housing Mold Inserts: Supported Precision Processes


Wire EDM
Wire EDM produces narrow slots, sharp internal profiles, and complex through features where conventional cutter access is limited. Wire-path planning considers corner conditions, stock condition, critical dimensions, and the relationship between mating connector features.

Sinker EDM
Sinker EDM addresses deep ribs, fine cavities, non-through details, and geometries requiring controlled electrode strategy. Electrode design, spark allowance, surface requirements, and later polishing or fitting needs are defined from the approved drawing.


Tool Fitting
Fitting verifies how connector housing mold inserts interact with adjacent cores, cavities, slides, gates, and locating components. The work focuses on functional interfaces, contact conditions, assembly clearance, and drawing-controlled revision alignment.

Dimensional Inspection
Inspection follows the agreed critical-dimension and reporting plan, using appropriate methods for the part geometry and order requirements. Results are checked against drawing revisions, datums, and specified documentation before delivery coordination.
Complementary Components for Connector Housing Mold Inserts

Guide Components
Guide pins, bushes, and locating elements help control repeatable mold-half alignment. Selection should consider plate stack, mating clearances, lubrication approach, wear exposure, and the datum scheme defined for the connector tooling assembly.

Locating Components
Precision locating blocks, keys, and stop elements support controlled insert positioning during assembly and maintenance. Define the functional datum, tolerance relationship, mounting method, and access for inspection before machining begins.

Ejection Parts
Ejector pins, sleeves, blades, and related retention parts can be specified around part geometry and release conditions. Drawing review should identify contact faces, clearance needs, hardness requirements, and any fitting or grinding allowance.

Gate Components
Gate inserts, sprue-related parts, and replaceable feed features are configured around resin flow, tool access, wear risk, and maintenance needs. Provide gate location, surface priorities, and mating-component information for a practical review.

Slide Components
Slides, wear plates, gibs, and retaining elements support side-action features where connector geometry requires them. SUUXIANG reviews travel, locating faces, machining access, fit requirements, and inspection points from the supplied drawing.
About SUUXIANG
SUUXIANG is the sole public-facing brand of Dongguan SuuXiang Precision Mold Co., Ltd., established in 2010 in Chang’an Town, Dongguan, Guangdong, China. Founded by XiaoCheng Huang, the company helps engineering, sourcing, and quality teams convert controlled drawings and specifications into inspected custom parts, precision mold components, and connector tooling.
For connector housing mold inserts, our planning brings together CNC milling and turning, multi-axis machining, wire and sinker EDM, precision grinding, fitting, and inspection. Before quotation or production commitment, we review critical dimensions, datum strategy, tool access, machining allowance, EDM needs, and inspection expectations.
What distinguishes SUUXIANG is disciplined project control around the drawing. We keep revision, process, quality, and delivery requirements visible throughout the work, so buyers can evaluate manufacturing decisions with the evidence needed for their specific program.

Connector Housing Mold Inserts: Core Tooling Capabilities
DFM and Datum Review
Before quoting connector housing mold inserts, SUUXIANG reviews drawings and models for critical dimensions, datum relationships, wall-feature access, tolerance stack risks, material requirements, and heat-treatment sequence. The review establishes what must be controlled before process commitments are made.
- Identify critical-to-quality dimensions and functional datums
- Check tool access, machining allowances, and feature reach
- Clarify material, surface, and heat-treatment requirements
- Align inspection needs with the drawing revision

CNC and EDM Planning
Connector tooling often combines accessible milled geometry with fine ribs, deep slots, sharp internal details, or narrow profiles. SUUXIANG selects an appropriate CNC, wire EDM, and sinker EDM route from the actual geometry, considering electrode strategy, wire path, and finishing requirements.
- Match process choice to feature geometry and access
- Review electrode needs before machining begins
- Plan wire paths for narrow or intricate profiles
- Coordinate EDM finishing with downstream grinding

Grinding and Fitting Strategy
For connector housing mold inserts, grinding stock and fitting interfaces require deliberate control after machining and EDM. SUUXIANG reviews mating faces, locating features, shutoff conditions, and surface priorities so finishing operations support assembly function rather than introduce avoidable rework.
- Define grinding allowance around precision faces
- Review locating, guiding, and mating interfaces
- Sequence finishing around heat treatment where required
- Keep fitting decisions tied to approved drawings

Inspection and Revision Control
Inspection planning begins with the dimensions that affect connector alignment, cavity function, and insert interchangeability. SUUXIANG links measurement methods, reporting expectations, and revision identification to the order so delivered connector housing mold inserts can be checked against the agreed specification.
- Prioritize critical dimensions and datum-based checks
- Confirm required inspection reports before production
- Maintain visible drawing and revision identification
- Coordinate final documentation with the inspection plan

Connector Housing Mold Inserts: A Drawing-Driven Comparison
Compare the project controls that help teams evaluate custom tooling components before production commitments.
← Swipe left or right to view →
Connector Housing Mold Inserts: Production Workflow
A controlled, drawing-led sequence that keeps manufacturing decisions, inspection evidence and delivery requirements visible throughout the project.
Review Drawings and Requirements
We review 2D drawings, 3D models, material, quantity, critical dimensions, datums, surface requirements, delivery target and inspection expectations before quotation.
Confirm DFM and Route
Project discussion identifies machining access, tolerance stack risks, heat-treatment sequence, EDM needs, grinding allowance and a practical process route for approval.
Machine Critical Features
CNC milling, turning, multi-axis work or micro machining produce the planned geometry while revision-controlled drawings and agreed specifications guide production.
Apply EDM and Grinding
Wire EDM, sinker EDM and precision grinding address fine profiles, inaccessible features and final stock removal according to the confirmed electrode and datum strategy.
Inspect Pack and Coordinate
Parts are inspected against the agreed plan, with order-matched documentation, protective packing and delivery coordination aligned to the confirmed project requirements.
How to Work With SUUXIANG on Connector Housing Mold Inserts
Provide complete requirements early so DFM, process planning, inspection, and delivery coordination can be aligned before production commitments.
Submit Your Drawing Package
Send 2D drawings and available 3D models with material, heat treatment, quantity, application context, delivery target, and required inspection documentation.
Define Critical Requirements
Identify critical dimensions, datums, surface requirements, mating features, and revision status so connector housing mold insert risks are visible before quotation.
Review DFM and Quotation
Review proposed machining, EDM, grinding, fitting, and inspection approaches with SUUXIANG, including access constraints, allowances, electrode strategy, and commercial scope.
Confirm Samples or Production
Confirm the approved revision, quality expectations, and any sample or production release requirements before manufacturing proceeds through the agreed process route.
Receive Documented Delivery
Coordinate delivery against the confirmed schedule and receive order-matched inspection documentation, revision information, and traceable communication for the completed parts.
Connector Housing Mold Inserts: Certifications and Quality Documentation
Customer Evidence Publication Policy
Customer-approved testimonial pending. This slot will publish a verified outcome on drawing-revision clarity after the customer approves the wording, attribution, and supporting project evidence.
Customer-approved testimonial pending. This slot will document the agreed inspection evidence, including the applicable critical dimensions and report scope, once the customer authorizes public use.
Customer-approved testimonial pending. This slot will describe the verified delivery-coordination outcome, including revision communication and shipment timing, after customer review and written publication approval.
Connector Housing Mold Inserts FAQ
Practical answers for drawing-led sourcing, process planning, inspection, and revision control.
What files should I send for connector housing mold inserts?
Which materials and heat treatments are suitable for connector housing mold inserts?
When do connector housing mold inserts require EDM instead of CNC machining?
How much grinding allowance should be specified on mold inserts?
How are connector housing mold inserts inspected?
How do you control revisions for connector housing mold inserts?
How should I plan lead time for connector housing mold inserts?
Can SUUXIANG support shipping and protect confidential connector tooling data?
Buyer’s Guide to connector housing mold inserts
Use this decision framework to specify insert geometry, materials, tolerances, and validation needs; compare supplier capabilities; and avoid tooling, fit, durability, and handoff mistakes before production.
1. What Are connector housing mold inserts?
One connector housing mold insert is a replaceable, precision-made tooling element installed within an injection mold. It locally forms critical plastic geometry such as terminal cavities, polarization keys, latch windows, sealing lands, lead-in chamfers, and other interfaces that control fit and function.
Two components are often confused with the insert: a molded-in metal contact is an electrical part placed into plastic during insert molding, while the finished connector housing is the molded polymer component delivered to assembly. A mold insert instead remains in the production tool and repeatedly shapes the housing; it is neither an electrical contact nor part of the shipped housing.
Three service benefits make inserts central to connector tooling: localized wear control, targeted correction after drawing revision, and replacement without remachining a complete mold block. Their datum locations, shutoffs, vent details, and surface condition directly influence cavity consistency, flash risk, terminal retention geometry, and repeatable molding performance.
2. Evolution of connector housing mold inserts
Two design shifts define the evolution: moldmakers moved from largely monolithic hardened cavity blocks toward replaceable insert systems, then toward feature-specific inserts machined, EDM-finished, ground, and fitted to a controlled datum scheme. The change made local wear, damage, or engineering revisions easier to isolate without remaking the entire cavity block.
Five product pressures accelerated that shift: smaller housings, higher contact counts, finer pitch, tighter terminal-location requirements, and engineering resins with demanding flow, shrinkage, or wear behavior. These conditions push insert design beyond nominal cavity geometry toward steel support, venting, gate proximity, shutoff robustness, electrode strategy, wire access, and measurable relationships between terminal cavities and mating features.
One production priority now dominates early review: repeatable transfer from drawing revision to production-ready tooling. Modular connector housing mold inserts can support parallel manufacture and targeted adjustment, but only when datums, interfaces, heat-treatment sequence, grinding stock, inspection points, and revision ownership are defined before machining begins.
3. Types of connector housing mold inserts
Connector housing mold inserts should be reviewed by the function and datum they control, not only by their steel outline. Each category exposes a different risk to wear, flash, damage, or future revision.
Cavity And Core Inserts
Cavity inserts form external walls, latches, and sealing faces; core inserts form internal voids and ribs. Ask which datums govern mating geometry and where abrasive resin or part-release damage will concentrate.
Terminal And Moving Inserts
Terminal-cavity and pin inserts establish contact pitch, retention windows, and small passages, where bent pins, flash, or polishing damage can alter fit. Slider or lifter inserts form undercuts; ask how travel, shutoff contact, and replacement access are controlled.
Shutoff Gate And Replaceable Inserts
Shutoff inserts define sealing intersections and are exposed to flash, galling, and edge chipping; gate inserts control melt entry and can suffer erosion or gate vestige damage. Interchangeable wear or revision inserts localize service changes; ask which features can be replaced without remaking the base tool.
4. Materials for connector housing mold inserts
P20 and hardened tool steels address different risk profiles in connector housing mold inserts. Resin grade, glass content, moisture exposure, polish target, feature size, cycle volume, and cooling behavior must be reviewed before release.
| Option | Best Fit | Key Trade-Off |
|---|---|---|
| Pre-hardened steel | Trials, revisions, repairable blocks | Lower wear reserve |
| Hardened tool steel | Glass-filled resin, high cycles | Heat treatment and grinding required |
| Stainless mold steel | Corrosion risk, polished cavities | Material and finish route must match resin |
| PVD or nitriding | Wear-prone sliding surfaces | Verify adhesion, thickness, repairability |
Steel Selection By Duty
P20-type pre-hardened steel suits development tools and serviceable insert blocks where machining changes or weld repair may be expected.
H13- or D2-type tool steel, hardened after rough machining, better suits repeated loading, small edges, and glass-filled resin wear; heat treatment must leave grinding stock.
Corrosion And Finish
420 stainless-family mold steel is considered when humid processing, corrosive resin byproducts, or polished cavity surfaces make rust resistance important.
Mirror-polish requirements narrow the acceptable steel, heat-treatment, EDM, and finishing route; a coating cannot correct poor substrate finish or damaged geometry.
Surface Options
PVD coatings can reduce sliding wear and adhesion on selected inserts, while nitriding can harden a surface without adding a separate coating layer.
0.1 mm-scale ribs, pins, and shutoffs require a review of coating thickness, edge condition, thermal transfer, and future repair method.
5. Custom features for connector housing mold inserts
Custom features should be specified from functional design intent, not treated as cosmetic options. For connector housing mold inserts, the drawing must connect every feature to molding behavior, inspection datum, service need, or revision risk.
Cavity And Insert Strategy
Cavity count affects output, runner balance, and the effort required to qualify dimensional consistency across positions.
Interchangeable inserts speed localized changes and service, but add interfaces that require controlled fitting and datum transfer.
Molding Feature Decisions
Gate location, venting, and ejector clearance must protect terminal cavities, mating faces, and other critical features during fill and release.
Texture or polish requirements belong on the drawing with area boundaries; finer cosmetics can increase finishing work and complicate repair.
Datums And Revision Evidence
Datum strategy should locate functional connector geometry before noncritical exterior surfaces, preventing tolerance stacks from masking a mismatch.
Identification marks need a defined location, depth, and revision meaning. Revision-controlled drawings, models, and inspection plans keep replacement inserts traceable.
6. Quality elements in connector housing mold inserts
Connector function is protected by an insert system, not a single dimension. Review steel condition, datum flow, cavity geometry, shutoffs, cooling, vents, alignment, and service access against the part’s CTQ features.
Datums And Terminal Cavities
Two or more controlled datums should locate the terminal-cavity pitch, retention windows, and mating-face features. A broken datum chain can shift contacts even when individual insert dimensions pass inspection.
100% cavity acceptance should define the measurement method, sampling rule, and functional gauge where terminal retention or mating fit is critical.
- Which datum locates terminal pitch?
- Which cavity dimensions are CTQ?
- Is a functional gauge required?
Shutoffs, Vents, And Cooling
0.01 mm-scale shutoff wear can create flash at cavity edges; the permitted flash location and limit belong on the acceptance record. Restricted venting can contribute to short shots, while uneven cooling can amplify warpage.
Specified vent locations, cooling-circuit access, and witness limits make troubleshooting repeatable after launch.
- Identify permitted flash zones
- Specify vent-cleaning access
- Define warpage inspection datum
Steel Condition And Maintainability
Each wear-prone insert should identify steel condition, heat-treatment state, surface-finish requirement, and replacement interface. Consistent guide, locating, and fitting features protect alignment through maintenance cycles.
SUUXIANG should review drawing revisions, grinding allowance, EDM strategy, and inspection evidence before confirming a process route.
- State heat-treatment sequence
- Call out critical finish areas
- Require revision-controlled reports
7. Choosing a connector housing mold insert manufacturer
A 2D drawing, 3D model, and critical-dimension list reveal more than a capability brochure. Evaluate connector housing mold inserts against documented process decisions, inspection evidence, and controlled response to revisions.
| Evaluation Area | Evidence To Request | Decision Signal |
|---|---|---|
| DFM | Annotated drawing review | Risks identified early |
| Process | Route and setup rationale | CNC, EDM, grinding fit |
| Inspection | Method and report sample | CTQs are measurable |
| Delivery | Milestone plan and capacity basis | Lead time is transparent |
Start With Drawing Review
A responsive DFM review should identify datum conflicts, tool access, EDM electrodes or wire paths, grinding stock, and inspection points before release.
Two revision cycles are often enough to expose whether questions are specific, traceable, and answered against the current drawing.
- Request annotated DFM feedback
- Confirm critical dimensions and datums
- Record revision identifier and date
Match The Process Route
CNC machining, EDM, grinding, and fitting should be proposed as a route tied to geometry and tolerance—not as a generic capability list.
A first-article plan should state the sample quantity, measurement method, acceptance criteria, and disposition path before material is cut.
Require Production Evidence
Material traceability should connect the received material, heat-treatment requirement where applicable, and final part documentation to the purchase order.
Prototype and low-volume support require visible capacity assumptions, lead-time milestones, revision control, and inspection-report scope.
- Material certificates when specified
- First-article inspection report
- Revision-controlled traveler or record
- Quoted lead-time milestones
8. Common connector housing mold insert mistakes
Connector housing mold inserts usually fail first at the interfaces between drawing intent, molding behavior, and inspection. A pre-machining review should turn each assumption into a controlled question.
Drawing And Datum Gaps
2D drawings without section views, datum callouts, or mating geometry invite conflicting interpretations. Ask: which features locate the terminal, seal, and mating face, and which datum scheme governs inspection?
Steel And Resin Exposure
Steel selected only on purchase price can wear, corrode, or polish poorly under the specified resin and additives. Confirm resin grade, glass or mineral filler, flame-retardant package, moisture exposure, and required surface treatment before selecting the insert material.
Tolerance And Service Access
±0.01 mm callouts applied broadly raise cost without protecting connector function, while hidden screws or ejector access delay maintenance. Identify the functional tolerance stack, measurement method, and every feature requiring cleaning, fitting, or replacement.
Shrinkage, Revisions, And Reports
Shrinkage values copied from a resin datasheet do not replace validation for wall thickness, gate location, and fiber orientation. Freeze a revision-controlled model before machining, then require inspection results tied to datums plus a mating, terminal-retention, or gauge-based functional check.
9. Launching connector housing mold inserts successfully
A successful launch treats the insert as a controlled interface, not a standalone machined item. Freeze manufacturing inputs before material is cut, then use tryout evidence to govern every revision.
Capture The RFQ Package
One RFQ package should include released 2D drawings, native or neutral 3D models, resin grade, shrinkage assumptions, cavity count, quantity, and target date.
Two lists should separately identify critical dimensions, datums, cosmetic surfaces, mating features, inspection reports, and the customer’s acceptance plan.
Review And Approve The Route
One DFM review should confirm tool access, parting-line risk, wire paths, electrode strategy, heat-treatment sequence, grinding stock, and measurement access.
Two comparable quotations should state scope, material condition, process route, inspection deliverables, exclusions, lead-time basis, and revision assumptions. Approve the drawing revision and change authority before machining starts.
Close The Tryout Loop
First-article inspection should compare measured results with the agreed critical-dimension plan before mold tryout. Record resin, molding conditions, defects, and dimensional feedback against the controlled drawing.
One revision log should assign each change an owner, reason, affected dimensions, approval date, and implementation status. Release pilot-run evidence before production handoff, including final inspection records and approved revision files.
10. Connector housing mold insert pricing
Two quote tiers commonly separate prototype inserts from low-volume repeat work: prototypes concentrate programming, setup and first-article inspection; repeat quantities can distribute those fixed activities across more pieces. Geometry, steel condition, EDM content and grinding access usually change cost more than part envelope alone.
Five approved inputs control a defensible quotation: drawing revision, critical tolerances, specified material and heat treatment, quantity, and validation or inspection requirements. SUUXIANG should confirm the process route and delivery priority after drawing review, because urgent scheduling, electrodes, wire paths and reporting can alter the final price.
| Quote tier | Typical cost drivers | Evidence to confirm |
|---|---|---|
| Prototype insert | Setup, complex features, EDM or grinding | Revision-controlled drawing; first-article plan |
| Low-volume inserts | Repeat quantity, shared setups, wear-risk features | Quantity release; material and heat-treatment requirements |
| Expedited work | Schedule priority, outside-process coordination | Target date; validation and inspection scope |
Start Your Connector Housing Mold Inserts Drawing Review
Upload your 2D drawing and 3D model with material, quantity, critical dimensions, inspection requirements, and target delivery date for a focused review.