
Custom EDM Electrodes for Mold Tooling, Built From Your Drawing
SUUXIANG reviews geometry, datum strategy, critical dimensions, and inspection needs before producing custom EDM electrodes for mold tooling.
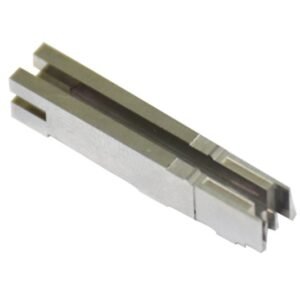
Representative Mold-Tooling Components and Electrode-Related Work





Related Configurable Component Families and RFQs







Why Engineering Teams Choose SUUXIANG for Custom EDM Electrodes for Mold Tooling
A drawing-led workflow that aligns DFM, electrode strategy, precision machining, inspection planning, and revision control before production.
Drawing-First Review
We review drawings, models, datums, critical dimensions, material requirements, and application context to identify manufacturability questions before quotation.
Practical DFM Input
Early DFM discussion clarifies tool access, feature geometry, machining allowance, electrode splits, flushing considerations, and process risks before manufacturing begins.
Route Selection
CNC machining, sinker EDM, wire EDM, grinding, and fitting are planned around geometry, surface requirements, hardness sequence, and inspection priorities.
Critical-Dimension Planning
Inspection methods and reporting needs are discussed against critical features, datum strategy, tolerances, and order-specific quality expectations.
Revision-Visible Communication
Project coordination keeps drawing revisions, production questions, inspection expectations, and delivery information visible throughout the custom tooling workflow.
RFQ-Ready Documentation
Upload drawings with quantities, material, heat treatment, surface priorities, target date, and reporting requirements for a focused technical review.
Electrode and Mold-Tooling Component Families
Drawing-driven process routes for precision components, EDM electrodes, and tooling work where geometry, datum control, material condition, and inspection requirements shape production.

CNC Machining Services
Precision CNC machining services for drawing-based parts requiring planned milling, turning, EDM, grinding, fitting, and inspection. Review focuses on critical dimensions, datums, material condition, tool access, and the process sequence needed to produce an inspectable component.
Upload a Drawing
CNC Milling
Custom CNC milling services for prismatic parts, inserts, electrode blanks, plates, and detailed mold features. Tool reach, corner radii, wall geometry, clamping, stock allowance, and datum setup are assessed before selecting a practical machining route.
Upload a Drawing
CNC Turning
Precision CNC turning services for shafts, bushings, sleeves, pins, collars, and rotational tooling components. Drawings should define concentricity, runout, thread details, bearing or mating surfaces, and any secondary milling, EDM, grinding, or heat-treatment requirements.
Upload a Drawing
5-Axis Machining
5-axis CNC machining for angled features, compound surfaces, deep access conditions, and geometries where multiple setups could affect positional control. The manufacturing review considers tool orientation, reachable surfaces, clamping strategy, tolerance relationships, and inspection access.
Upload a Drawing
Swiss & Micro Machining
Swiss machining and micro machining for small, slender, or detail-intensive pins, shafts, sleeves, and connector-related components. Diameter-to-length ratio, feature spacing, material behavior, burr control, and measurement method must be reviewed against the drawing and functional requirements.
Upload a Drawing
Wire & Sinker EDM
Wire EDM and sinker EDM services for narrow slots, sharp internal forms, hardened materials, intricate cavity details, and features beyond conventional tool access. Planning addresses wire paths, start holes, electrode design, flushing, recast considerations, and finishing requirements.
Upload a Drawing
Precision Grinding
Precision surface and profile grinding for flatness, parallelism, thickness control, profile accuracy, and finished functional surfaces. Grinding stock, heat-treatment sequence, datum transfer, wheel access, and inspection criteria should be established before production.
Upload a Drawing
Mold Core & Cavity Inserts
Precision mold core and cavity inserts produced from approved drawings and material specifications. Machining plans account for parting geometry, cooling or venting features, EDM details, hardening sequence, grinding allowance, fitting interfaces, and critical molded-part surfaces.
Upload a Drawing
Ejector & Ejection Components
Ejector pins, sleeves, and ejection components for controlled mold movement and repeatable part release. Requirements typically include fit relationships, alignment, surface condition, wear considerations, heat treatment, and the dimensions that affect ejection performance.
Upload a Drawing
Core Pins, Guide & Locating Components
Core pins, guide pins, and locating components machined around functional alignment and mating interfaces. Drawing review examines concentricity, clearance or interference fits, straightness, surface finish, hardness requirements, and the datum scheme used for inspection.
Upload a Drawing
Slides, Lifters, Gates & Mold Accessories
Mold slides, lifters, gates, and accessories for moving, guiding, feeding, or supporting mold functions. Geometry is evaluated with travel direction, wear faces, clearances, assembly references, lubrication needs, machining access, and fitting requirements in view.
Upload a Drawing
Connector Mold Components
Precision connector mold components for feature-dense tooling where pin locations, fine profiles, mating relationships, and repeatability affect connector performance. Process planning may combine CNC machining, EDM, grinding, fitting, and defined inspection of critical interfaces.
Upload a Drawing
Stamping Die Components
Precision stamping die components for forming, cutting, guiding, and supporting die operations. Material condition, clearance relationships, edge geometry, wear surfaces, heat treatment, grinding sequence, and assembly datums should be specified for an appropriate manufacturing route.
Upload a Drawing
Injection, MIM, CIM & Overmolding Tooling
Injection mold components for MIM, CIM, and overmolding applications, produced within verified project scope. The drawing review considers material-flow geometry, shutoffs, inserts, molding interfaces, thermal or wear requirements, machining access, and inspection expectations before commitment.
Upload a Drawing
Machining Materials
CNC machining materials selected against the drawing, application, heat-treatment condition, corrosion exposure, wear needs, and dimensional requirements. Material availability, machinability, certification needs, and any supplied material standard should be clarified in the RFQ.
Upload a Drawing
Surface Finishes & Heat Treatment
Surface finishing and heat treatment planned as controlled stages rather than afterthoughts. Requirements should identify coating or finish type, roughness, hardness, masking, dimensional changes, grinding allowance, corrosion needs, and any post-treatment inspection requirements.
Upload a Drawing
Quality, Metrology & Documentation
Precision inspection, metrology, and quality documentation aligned to the agreed drawing revision and inspection plan. Critical dimensions, datums, measuring methods, report format, material evidence, and traceability expectations should be confirmed before production begins.
Upload a Drawing
Prototyping & Low-Volume Production
Rapid prototyping and low-volume manufacturing for drawing-driven parts that need practical process planning before repeat production. Quantity, revision maturity, material, critical dimensions, inspection needs, and target delivery date guide the appropriate machining and documentation approach.
Upload a DrawingCustom EDM Electrodes for Mold Tooling: Materials to Review

Graphite Grades
A lightweight, easily machined electrode option for detailed cavity features, deep ribs, and multi-electrode programs. Grade selection affects particle structure, edge integrity, wear behavior, and attainable surface condition during sinker EDM.

Red Copper
A conductive electrode material often considered where fine feature transfer and surface requirements demand careful control. Copper machining, electrode geometry, flushing conditions, and expected wear should be reviewed together before the EDM plan is released.

Copper Tungsten
A dense composite electrode material suited to applications where dimensional stability and wear resistance are important. Its machining approach, cost implications, and EDM behavior should be evaluated against feature size, tool steel, and finish priorities.

Pre-Hardened Tool Steel
A practical mold-tooling material for bases, inserts, and supporting components when the specified condition supports the intended machining route. Confirm critical dimensions, machining allowance, EDM areas, and inspection requirements from the drawing.

Hardened Tool Steel
A tooling material commonly specified for cavity inserts, cores, and wear-critical mold components requiring EDM and precision grinding. Heat-treatment sequence, datum protection, finishing stock, and measurement method need agreement before production.
Custom EDM Electrodes for Mold Tooling: Process Routes


Sinker EDM
Sinker EDM forms cavities, ribs, deep details, and internal features where cutting-tool access is limited. Electrode strategy, spark allowance, finish targets, and datum relationships should be defined against the tooling drawing.

Wire EDM
Wire EDM cuts accurate profiles, inserts, apertures, and intricate contours in suitable workpiece conditions. The planned wire path, start-hole needs, stock condition, and critical dimensions are reviewed alongside the specified geometry.


Component Fitting
Fitting brings mating tooling components together for functional relationships beyond isolated dimensions. Clearance, contact areas, assembly sequence, and application context help determine where hand fitting or controlled adjustment is appropriate.

Final Inspection
Inspection verifies agreed critical dimensions, datum-based measurements, surface priorities, and required reporting against the order-specific plan. Revision control keeps the drawing, model, and inspection evidence aligned before delivery coordination.
Tooling Interfaces and Supporting Components

Electrode Holders
Holder selection connects the electrode to the EDM machine interface. Confirm the holder style, clamping method, reference surfaces, and required repeatability against the machine setup and project drawing before machining.

Mounting Shanks
Custom shanks provide a controlled connection between the electrode and its holder. Dimensions, material, thread or clamping features, and datum relationship should support the planned machining, EDM orientation, and setup sequence.

Locating Features
Dowel holes, reference pads, keyways, and other locating features help establish repeatable orientation. Their placement should follow the agreed datum scheme so electrode positioning, inspection, and replacement remain traceable across revisions.

EDM Fixtures
Dedicated fixtures can support complex electrode geometry, multi-position burning, or controlled inspection. Review access, clamping clearance, flushing considerations, and contact surfaces with the electrode strategy before committing to a fixture design.

Identification Labels
Engraved marks, labels, or controlled identification fields help distinguish electrodes within a tooling program. Confirm part number, revision, cavity reference, and marking location so identification does not interfere with functional surfaces.

Storage Protection
Protective trays, covers, or handling provisions can reduce risk to delicate electrode details during transfer and storage. Define the required protection level, packaging method, and shipment identification when these are relevant to the order.
A Drawing-Led Partner for EDM Electrode Tooling
SUUXIANG is the sole public-facing brand of Dongguan SuuXiang Precision Mold Co., Ltd., established in 2010 in Chang’an Town, Dongguan, Guangdong, China. XiaoCheng Huang is the founder and legal representative. We help global engineering, sourcing, and quality teams turn drawings and specifications into inspected custom EDM electrodes for mold tooling, precision components, and related tooling work.
Our work is planned around the drawing, 3D model, material requirement, quantity and critical dimensions. CNC machining, sinker EDM, wire EDM, grinding, fitting and inspection are coordinated according to tool access, datum strategy, electrode needs, heat-treatment sequence and the agreed inspection plan.
What distinguishes SUUXIANG is disciplined project communication before commitments are made. We review manufacturability, machining allowances, surface requirements, revision status and traceability requirements early, so customers can align the process route and acceptance evidence with the needs of the mold or production program.

From Electrode Strategy to Inspection
DFM and Datum Review
Before quotation, SUUXIANG reviews the drawing, model, critical dimensions, datum scheme, cavity geometry, material requirements and surface priorities. This early review identifies tool-access constraints, tolerance-stack risks and information that must be resolved before electrode design and production planning.
- Confirm critical-to-quality dimensions and functional datums
- Review cavity accessibility, corner conditions and feature depth
- Align material, heat-treatment and surface requirements
- Clarify revision status, quantity and inspection expectations

Electrode Strategy and Access
Custom EDM electrodes for mold tooling are planned around the geometry that cutting tools cannot reach efficiently. SUUXIANG evaluates electrode split strategy, burn direction, holder interface, spark-gap requirements and flushing access so the electrode design supports the intended cavity feature and downstream setup.
- Assess CNC reach before assigning EDM features
- Define burn direction and electrode partitioning
- Review holder, reference surfaces and setup repeatability
- Consider flushing paths for deep or detailed features

EDM and Grinding Sequence
The process route is coordinated across CNC machining, sinker or wire EDM, grinding and fitting according to the drawing and verified project requirements. Sequencing decisions account for machining allowance, heat-treatment stage, datum preservation and the surfaces that require final grinding or controlled finishing.
- Set machining and grinding allowance by process stage
- Protect datums through heat treatment and EDM operations
- Plan wire paths and sinker-EDM features separately
- Coordinate fitting surfaces with final dimensional requirements

Inspection and Revision Control
Inspection planning connects the drawing’s critical features to practical measurement methods and order documentation. SUUXIANG keeps revision information visible throughout the project and aligns final records with the agreed inspection plan, helping purchasing and quality teams review delivered custom EDM electrodes for mold tooling.
- Identify dimensions requiring defined inspection methods
- Match inspection records to the released drawing revision
- Record material, quantity and order-specific requirements
- Flag unresolved quality or documentation questions early

What to Confirm Before Selecting an EDM Electrode Supplier
A drawing-led workflow for reviewing critical features, planning EDM routes, and aligning inspection evidence before production.
← Swipe left or right to view →
From Drawing Review to Delivery
Each project is planned around the drawing, critical dimensions, EDM strategy, inspection requirements, and controlled revision information before production commitments are made.
Drawing and DFM Review
We review 2D and 3D data, material, application, datums, critical dimensions, surface requirements, quantity, and delivery expectations before confirming a workable route.
Process and Electrode Planning
The team defines machining access, electrode geometry, burn allowance, flushing considerations, wire paths, heat-treatment sequence, grinding stock, and inspection points for the approved revision.
CNC Machining and EDM
CNC milling, turning, multi-axis machining, wire EDM, or sinker EDM are applied according to the documented process plan and feature requirements.
Grinding and Precision Fitting
Where required, precision grinding and fitting address mating interfaces, datum relationships, finish requirements, and remaining stock while protecting the intended functional geometry.
Inspection and Delivery Coordination
Completed custom EDM electrodes for mold tooling are checked against the agreed inspection plan, then packed with applicable documentation and coordinated delivery information.
Source EDM Electrodes with a Controlled RFQ
Share complete requirements early so electrode strategy, critical dimensions, inspection expectations, and delivery coordination can be reviewed before production.
Submit Your Drawing Package
Provide 2D drawings, 3D models when available, material, quantity, application context, target date, and any critical dimensions or surface requirements.
Review DFM and Requirements
SUUXIANG reviews datum strategy, machining access, electrode geometry, EDM allowance, interfaces, inspection needs, and revision status before preparing a project-specific quotation.
Align First-Article Expectations
Where the project requires it, confirm sample or first-article scope, measurement methods, acceptance criteria, and documentation before moving into production.
Produce and Inspect Parts
Manufacturing follows the agreed CNC, EDM, grinding, fitting, and inspection route, with controlled handling of critical dimensions and approved drawing revisions.
Receive Verified Documentation
Before delivery, align final part identification and inspection documentation with the order requirements and verified inspection plan for clear receiving review.
Quality Documentation for EDM Electrode Orders

Customer References Pending Approval
Customer references are published only after the project context, quotation, and reported outcome have been verified and approved for release.
Custom EDM Electrodes for Mold Tooling FAQ
Practical answers for engineering, procurement, and quality teams preparing a drawing-led electrode tooling inquiry.
What should I send when requesting custom EDM electrodes for mold tooling?
Can you quote prototype or low-volume EDM electrode orders?
How long does it take to make custom EDM electrodes for mold tooling?
Can I order a sample or first article before a larger tooling order?
How do you control electrode material and heat-treatment requirements?
What inspection information can be included with an EDM electrode order?
How are drawing revisions and confidential tooling data handled?
What payment and shipping details should I confirm before placing an order?
Complete Buyer’s Guide to Custom EDM Electrodes for Mold Tooling
Use a practical decision framework to specify electrode geometry, material, quality controls, and supplier capability—while avoiding costly errors in tolerance transfer, flushing design, inspection, and production handoff.
1. What Are Custom EDM Electrodes?
2D drawings and 3D CAD models define a custom EDM electrode as a purpose-made conductive tool whose working form is programmed to reproduce a required mold feature by sinker EDM. Its geometry, datum references, orbit or spark-gap allowance, and holder interface must be established before manufacture.
90-degree internal corners, narrow ribs, deep pockets, and inaccessible cavity details often exceed practical cutter reach or require tool lengths that compromise rigidity. In those cases, the electrode approaches the hardened workpiece under controlled electrical discharges, transferring its inverse working geometry while a planned gap separates electrode and steel.
3 common mold-tooling uses are cavity inserts with fine texture boundaries, core details with deep or thin features, and shutoff or gate regions where milling access is limited. For custom edm electrodes for mold tooling, the drawing review should identify the feature datum, target steel condition, permitted radii, finishing requirement, and inspection method before the electrode strategy is released.
2. How Mold-Tooling EDM Evolved
1970s-era mold shops often relied on manually shaped, bench-fitted electrodes and operator knowledge to transfer a cavity feature. That approach could solve difficult geometry, but repeatability depended heavily on individual setup, orientation marking, and hand-maintained records.
3D CAD/CAM changed the handoff by letting the mold feature, electrode geometry, spark gap, holder orientation, and machining paths be defined from controlled digital data. CNC-machined blanks then made it practical to produce intricate forms consistently, while standardized holders established a repeatable datum between electrode machining, inspection, and sinker EDM.
1 controlled revision now matters as much as the electrode shape. Buyers sourcing custom edm electrodes for mold tooling should require the current model or drawing revision, electrode ID, holder reference, datum scheme, burn allowance, EDM setup information, and inspection requirements; these records shorten engineering-to-shop handoffs and help prevent an obsolete electrode from reaching the machine.
3. Types of custom edm electrodes for mold tooling
One cavity rarely benefits from one universal electrode. Electrode format should follow feature access, required finish, expected wear, and the flushing path before EDM parameters are selected.
Roughing, Semi-Finishing, And Finishing
Three-stage sets separate metal removal from final geometry. Roughing electrodes prioritize stable sparking and stock removal; semi-finishing restores controlled detail after wear.
Finishing electrodes carry the smallest details and final surface intent. Their geometry needs enough land, datum stability, and wear allowance to avoid transferring a rounded or undersized feature.
Segmented And Multi-Electrode Sets
Two or more electrodes are justified when a cavity combines deep walls, shutoff-adjacent details, and inaccessible corners. Splitting the work lets each electrode approach from a stable direction and preserves its own datum and flushing strategy.
Segment joints should not fall on cosmetic surfaces or critical sealing edges. The EDM drawing should identify sequence, spark gaps, electrode offsets, and verification points.
Deep-Rib And Thin-Wall Forms
Deep-rib electrodes need a stiff shank, conservative rib proportions, and a dielectric escape route. Poor debris evacuation can cause secondary discharge, localized damage, and unstable finish.
Thin-wall forms require controlled clamping and short effective reach. Buyers should provide minimum wall thickness, rib depth, corner radii, and any forbidden witness locations during drawing review.
4. Materials for custom edm electrodes for mold tooling
Four electrode families create different trade-offs in burn rate, detail retention, and shop handling. Select material from the cavity drawing, tool-steel condition, specified finish, and expected electrode repeat quantity.
| Material | Machining And Handling | Typical EDM Use |
|---|---|---|
| Graphite | Fast machining; dust control; brittle thin details | Roughing and general cavities |
| Copper | Fine detail; heavy; slower milling | Fine finishing and sharp features |
| Copper-tungsten | High wear resistance; difficult machining | Small, demanding finishing features |
| Specialty alloys | Review cost and application case | Exceptional wear or feature needs |
Material Trade-Offs
Graphite machines quickly and is light, but its dust requires controlled extraction and careful handling of thin ribs. Copper conducts heat and electricity well, supports delicate edges and fine finishing, yet is heavier and less convenient to machine.
Copper-tungsten resists wear and deformation in small, high-energy features, but costs more and machines slowly. Silver-tungsten or specialty grades require an application-specific review rather than a default material callout.
Match The Burn Strategy
Roughing electrodes prioritize stable removal, flushing access, and replacement cost; graphite is often practical where geometry permits. Fine-finishing electrodes prioritize corner integrity, wear control, and the required cavity surface.
For custom edm electrodes for mold tooling, provide the 2D drawing, 3D model, steel grade and heat-treatment state. Also identify Ra target, critical radii, unsupported thin features, quantity per mold, and planned production repeats.
5. Customizing custom edm electrodes for mold tooling
A controlled electrode definition extends beyond the burn geometry. For custom edm electrodes for mold tooling, the interface, datums, allowances, and identification must agree before CAM and EDM setup.
| Specification | 3D Model | 2D Drawing | EDM Setup Sheet |
|---|---|---|---|
| Holder and datum | Interface geometry | Reference dimensions | Clamping reference |
| Allowances | Spark and relief surfaces | Finish and corner notes | Offset or orbit instruction |
| Identification | Electrode ID | Cavity and revision | Burn sequence and verification |
Define The Machine Interface
One holder or shank standard should be named with its clamping dimensions and reference face. The model should show the holder, shank, electrode body, and tool-access envelope.
Two orientation marks or asymmetric features prevent a rotated installation. The 2D drawing should identify the primary datum, secondary datum, and electrode zero point.
Control Allowances And Relief
Three allowance types require separate callouts: spark gap, finish stock, and corner condition. Never let a CAM model imply whether an edge is sharp, radiused, or intentionally relieved.
Two flushing paths should be shown where deep or enclosed burns need debris evacuation. Relief features also need dimensions so they cannot transfer unwanted cavity geometry.
Document Splits And Traceability
Each split electrode needs a cavity number, burn sequence, and revision identifier. The EDM setup sheet should map every electrode ID to its workpiece datum, orbit or offset instruction, and inspection requirement.
One released 3D model defines geometry; a controlled 2D drawing defines critical dimensions. Revision status must match across the model, drawing, electrode label, and setup documentation.
6. Construction Quality That Protects Accuracy
Two independent references—an electrode datum and a holder datum—should survive machining, inspection, and setup. Construction quality determines whether the programmed burn geometry can be repeated at the intended machine position.
Datums And Holding
One primary datum, two secondary locating features, and a documented orientation prevent ambiguous setting. Holder runout or poor concentricity can move fine features before EDM begins.
Three contact surfaces should clamp cleanly without rocking or distortion. Stable clamping matters most when long, thin, or segmented electrodes are transferred between machines.
Geometry And Edges
One approved compensation model must distinguish nominal electrode geometry, spark gap, wear allowance, and intended cavity result. An inspected electrode is not evidence that the finished cavity meets drawing requirements.
Two edge conditions require review: protected sharp features and removed burrs. Burrs, loose graphite, or damaged corners can alter discharge behavior and contaminate the setup.
Surface And Traceability
Two practical checks are surface condition and flushing clearance around the burn zone. Clearance must support debris removal without creating an unintended witness or weak electrode section.
Each electrode record should link part revision, material, datum scheme, inspection results, and EDM program identifier. Final cavity acceptance requires its own dimensional inspection against the mold drawing and agreed datums.
7. How to Evaluate an EDM Electrode Supplier
Two gates should precede an electrode purchase order: technical release and quality release. For custom edm electrodes for mold tooling, assess evidence, interfaces, and change discipline rather than a supplier’s general equipment list.
DFM And CAM Readiness
One drawing-review record should identify datums, EDM spark allowance, burn direction, tool access, and flushing constraints.
Two questions matter: can CAM output be checked against the released model, and are electrode splits approved before machining?
Traceability And Measurement
One material record should link the electrode blank, grade, purchase order, and job traveler.
Two report details should be agreed before release: measured features and their datum reference. Ask which instrument, sampling plan, and report format will be used.
Interfaces And Delivery Control
One holder definition should cover shank geometry, locating faces, orientation, clamping method, and machine-specific offsets.
Two controls protect prototypes: revision acknowledgement before machining and protective packaging that prevents edge damage or mixed electrodes. Ask for the communication owner and response path for deviations.
8. Common EDM Electrode Sourcing Mistakes
Eight recurring RFQ omissions create avoidable EDM risk before machining starts. For custom edm electrodes for mold tooling, resolve the manufacturing assumptions in the release package, not through shop-floor interpretation.
Datum And Gap Definition
Two missing items—electrode datums and spark-gap assumptions—can shift the transferred geometry. Provide a datum-linked electrode drawing, target cavity dimensions, polarity and gap strategy; otherwise inspection results can be correct to the wrong reference.
Material And Burn Strategy
Two price-led decisions cause rework: choosing material without considering wear, finish and geometry, and using one electrode plan for roughing and finishing. Specify the intended burn stage and acceptance criteria; otherwise wear compensation and surface results may be inconsistent.
Flushing And Holder Interfaces
Two interface details—flushing access and holder definition—determine whether a designed electrode can burn stably. Share cavity depth, flushing paths, holder standard and clamping datum; otherwise debris, arcing or setup misalignment can damage the cavity or delay release.
Revision And Schedule Control
Two control failures—undocumented revisions and unsupported requested dates—break traceability. Issue a controlled revision with change notes, quantity and required inspection evidence, then confirm the process sequence; otherwise obsolete geometry may be made or lead time may be missed.
9. Steps to Launch an Electrode Program
A controlled launch for custom edm electrodes for mold tooling begins with a complete technical package and defined approval gates. For prototypes and low-volume programs, visible revision ownership prevents an electrode from being machined against superseded cavity data.
Build The RFQ Package
1 RFQ package should include 2D drawing, 3D model, electrode quantity, cavity steel, datum scheme, surface target, delivery date, and EDM-machine or holder context.
1 buyer or program manager should identify the controlling drawing revision and inspection-report requirement before quotation.
Close Technical Approvals
2 reviews should confirm manufacturability: the supplier reviews tool access, burn direction, clearance, flushing, wear allowance, and inspection approach; the mold designer approves the electrode design.
1 approved record should lock material, holder interface, burn map, revision, and any split-electrode strategy before material release.
Control Build And Feedback
3 production records should travel with the job: material identification, machining route, inspection results, and label data linking each electrode to its cavity and revision.
1 EDM trial should compare the burned feature with the acceptance criteria. The EDM technician returns wear, flushing, finish, and fit observations for the next revision.
10. Custom EDM Electrode Pricing and Lead Times
1 RFQ can produce very different pricing when electrode count, burn geometry, datum scheme, and tolerance zones change. For custom edm electrodes for mold tooling, SUUXIANG should quote only after reviewing controlled 2D/3D data, material, required quantity, and delivery conditions.
2 process stages commonly separate roughing from finish-burn electrodes, so a low electrode count does not necessarily mean a simple job. Confirm holder interface, inspection report format, revision level, and whether fitting or EDM setup information is included before comparing quotations.
| Cost and schedule driver | Lower impact | Higher impact |
|---|---|---|
| Geometry | Open, accessible form | Deep ribs, fine details, multiple electrodes |
| Material | Readily machinable selected stock | Specified copper or graphite grade |
| Quantity | Repeated, stable program | One-off or revision-sensitive set |
| Holder | Standardized interface | Custom holder or orientation control |
| Inspection | Basic dimensional checks | CTQ report and datum-based verification |
| Finishing | Roughing stage | Fine finishing and edge protection |
Upload Your Drawing for Custom EDM Electrodes for Mold Tooling
Send 2D/3D files, material and heat-treatment details, quantity, critical dimensions, quality requirements, and target date for a drawing-led review.