
CNC Machined Threaded Adapters, Reviewed Before Production
Send your drawing for CNC machined threaded adapters. SUUXIANG will align DFM, critical-dimension review, process planning, and inspection requirements before production.
Representative Precision-Machined Components





Drawing-Based Product Families and Quotation


CNC Machined Threaded Adapters: Engineering Advantages
Drawing-led planning keeps critical thread interfaces, mating features, and inspection expectations visible before production begins.
Drawing-First DFM Review
Review thread callouts, mating conditions, material requirements, and critical dimensions before quotation so manufacturability questions are addressed early.
Datum Strategy Alignment
Define functional datums and measurement references for threads, shoulders, bores, and sealing faces to support consistent setup and inspection.
Process Route Planning
Select CNC turning, milling, EDM, grinding, and fitting steps around geometry, access, heat treatment, and required finishing allowances.
Critical Thread Control
Identify thread form, engagement length, concentricity, and adjacent functional features requiring focused machining and verification planning.
Inspection Plan Visibility
Align inspection methods, reporting needs, and critical-to-quality dimensions with the drawing before production commitments are finalized.
Revision Traceability
Keep drawing revisions, project communication, and delivery requirements visible throughout machining, inspection, and order coordination.
CNC-Machined Components by Application
Drawing-driven process routes for mold, connector, die and custom interfaces, reviewed against critical dimensions, materials, inspection requirements and production intent.

CNC Machining Services
Precision CNC machining services for drawing-based custom parts, combining milling, turning, multi-axis machining, EDM, grinding and inspection as the geometry, material condition and critical dimensions require.
Upload a Drawing
CNC Milling
Custom CNC milling services for prismatic parts, plates, inserts and complex features. Drawing review considers datum structure, cutter access, corner radii, remaining stock and inspection access before a machining route is committed.
Upload a Drawing
CNC Turning
Precision CNC turning services for shafts, sleeves, threaded adapters, pins and rotational features. Requirements are reviewed for concentricity, runout, thread definition, surface condition and any secondary milling, EDM or grinding operations.
Upload a Drawing
5-Axis Machining
5-axis CNC machining supports parts with compound angles, contoured surfaces and features that benefit from fewer setups. Process planning evaluates tool reach, workholding, datum transfer and access to critical dimensions.
Upload a Drawing
Swiss & Micro Machining
Swiss machining and micro machining support small-diameter pins, shafts, sleeves and miniature interface components. Feasibility depends on material, feature scale, length-to-diameter relationship, tolerances, surface requirements and inspection method.
Upload a Drawing
Wire & Sinker EDM
Wire EDM services and sinker EDM services address hardened materials, narrow slots, internal profiles, sharp geometry, and features inaccessible to conventional cutting. Electrode design, wire path, flushing, recast-layer considerations, and finishing allowance are reviewed by application.
Upload a Drawing
Precision Grinding
Precision surface and profile grinding is used where flatness, parallelism, profile control or final size requires a controlled finishing process. Grinding stock, heat-treatment sequence, datum references and measurement strategy should be defined early.
Upload a Drawing
Mold Core & Cavity Inserts
Precision mold core inserts and mold cavity inserts are produced to drawing-defined geometry, material, and finish requirements. Review covers shutoff areas, cooling or feature access, EDM strategy, heat treatment, fitting relationships, and inspection priorities.
Upload a Drawing
Ejector & Ejection Components
Ejector pins, sleeves and ejection components are made to support reliable movement and controlled fit within the mold assembly. Key considerations include mating clearances, hardness condition, straightness, surface finish and identification of critical working dimensions.
Upload a Drawing
Core Pins, Guide & Locating Components
Core pins, guide pins and locating components are evaluated as mating interfaces, not generic catalog items. Drawings should establish datums, fit relationships, alignment needs, material condition, wear considerations and inspection requirements.
Upload a Drawing
Slides, Lifters, Gates & Mold Accessories
Mold slides, lifters, gates and accessories are produced as configurable tooling components for the specified mold design. Manufacturing review addresses travel interfaces, shutoffs, wear faces, machining access, EDM needs, fitting and assembly-critical dimensions.
Upload a Drawing
Connector Mold Components
Precision connector mold components support terminal, housing and interconnect-tooling applications where pitch, alignment and repeated mating relationships matter. Review focuses on datum strategy, fine features, material condition, EDM or grinding requirements and inspection evidence.
Upload a Drawing
Stamping Die Components
Precision stamping die components are produced for drawing-defined cutting, forming, guiding and locating functions. Process planning considers working edges, material and heat-treatment sequence, clearance relationships, grinding stock, surface condition and mating interfaces.
Upload a Drawing
Injection, MIM, CIM & Overmolding Tooling
Injection mold components, including components for MIM, CIM, and overmolding tooling, are considered within verified production scope. A drawing review identifies material, shrinkage-related interfaces, core and cavity geometry, feature access, surface needs, and the required machining, EDM, and fitting route.
Upload a Drawing
Machining Materials
CNC machining materials are selected against the drawing, function, heat-treatment condition and finishing requirements. RFQs should identify the specified grade, material form, certification or traceability needs, and any application-driven constraints.
Upload a Drawing
Surface Finishes & Heat Treatment
Surface finishing and heat treatment are planned around function, material and dimensional risk. Requirements should define finish type, roughness or appearance criteria, hardness or treatment condition, masking needs and whether post-treatment grinding is required.
Upload a Drawing
Quality, Metrology & Documentation
Precision inspection, metrology and quality documentation are aligned to the drawing’s critical dimensions and agreed inspection plan. Requirements may include first-article data, dimensional reports, material records, revision identification and traceable delivery documentation.
Upload a Drawing
Prototyping & Low-Volume Production
Rapid prototyping and low-volume manufacturing support drawing-based validation, bridge quantities and controlled production runs. Provide the latest drawing or model, quantity, material, critical dimensions, surface requirements, inspection needs and target delivery date.
Upload a DrawingMaterials for CNC Machined Threaded Adapters

Stainless Steel
A practical choice for threaded interfaces exposed to moisture, washdown, or corrosive service. Grade selection, thread engagement, burr control, and any passivation requirement should be reviewed against the mating component and operating environment.

Aluminum Alloys
Well suited to weight-sensitive housings, brackets, and connector assemblies where efficient machining is important. Alloy, temper, wall thickness, thread-insert needs, and anodizing strategy should be defined before machining.
Carbon Steel
Used for robust industrial adapters where strength and economical material selection are central considerations. Confirm coating, heat treatment, thread protection, and corrosion exposure during drawing review so the finished interface matches its intended service.
Alloy Steel
Consider for demanding mechanical connections that may require higher strength or controlled heat-treatment sequences. Machining allowance, distortion risk, grinding needs, and final thread inspection must be evaluated with the specified material condition.
Brass Alloys
Often selected for machinability and corrosion-conscious fluid, electrical, or instrument connections. The RFQ should identify the alloy, thread standard, sealing approach, surface requirement, and mating material to assess suitability for the assembly.
CNC Machined Threaded Adapters: Process Options
CNC Turning
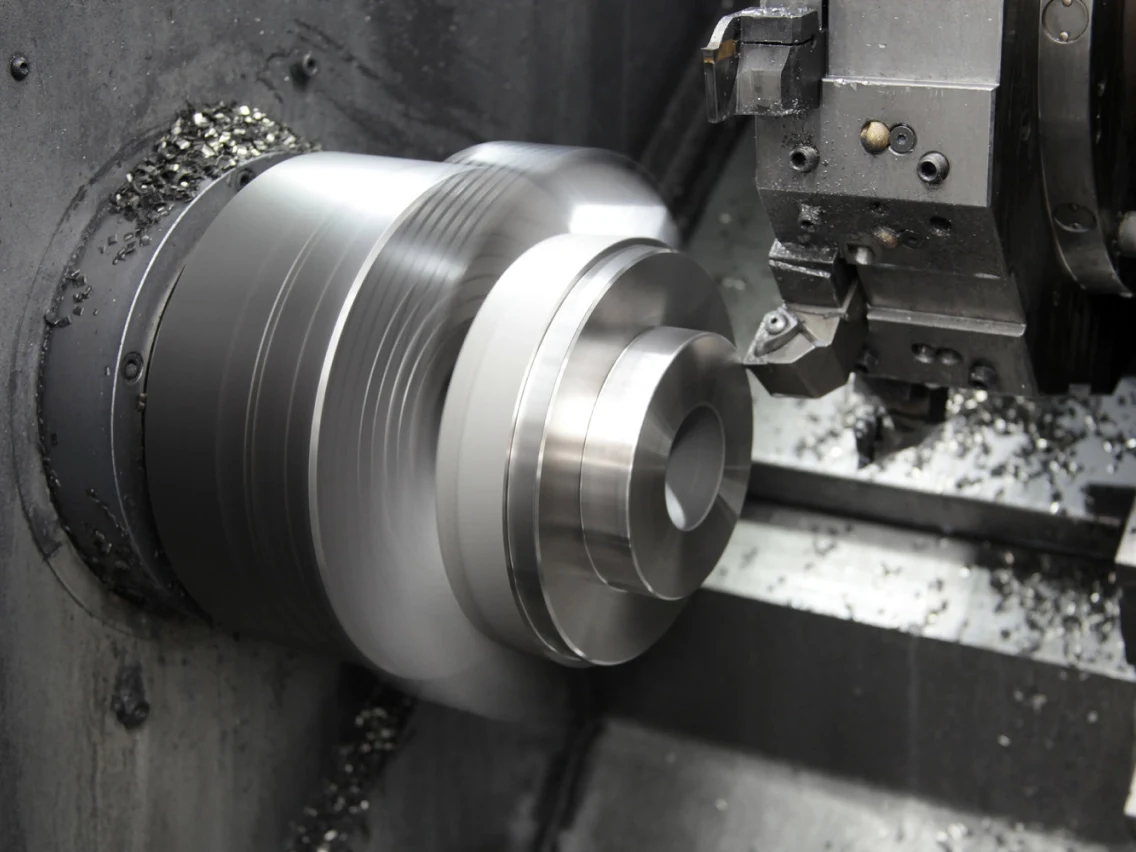
CNC turning forms concentric diameters, shoulders, bores, and external or internal thread features. It establishes stable rotational geometry and controlled thread engagement for adapter bodies designed around a common centerline.
CNC Milling
CNC milling produces flats, wrench features, cross holes, mounting faces, ports, and other non-rotational geometry. Tool access and datum relationships are reviewed before machining to protect functional interfaces.
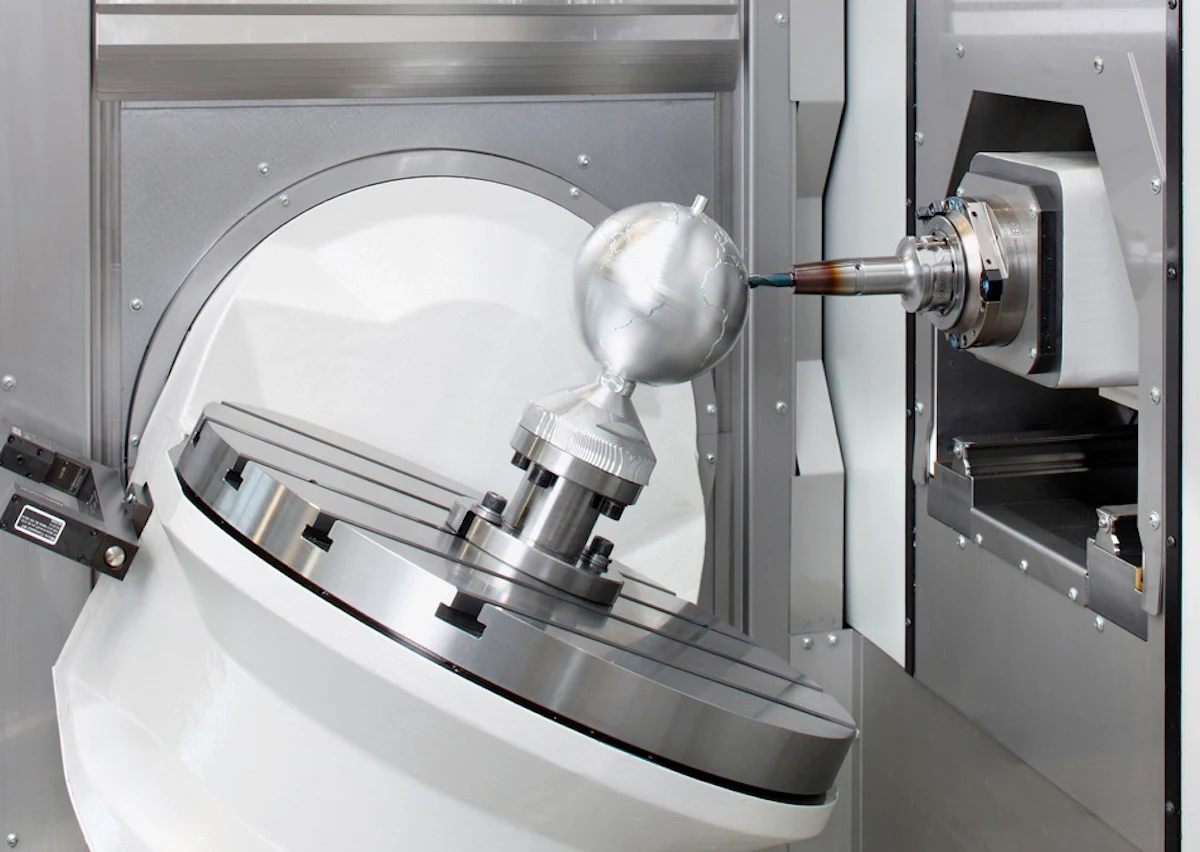

EDM Processing
Wire or sinker EDM can support fine internal profiles, hardened material features, and geometry with limited cutting-tool access. Electrode or wire-path strategy, surface requirements, and downstream finishing are defined from the drawing.
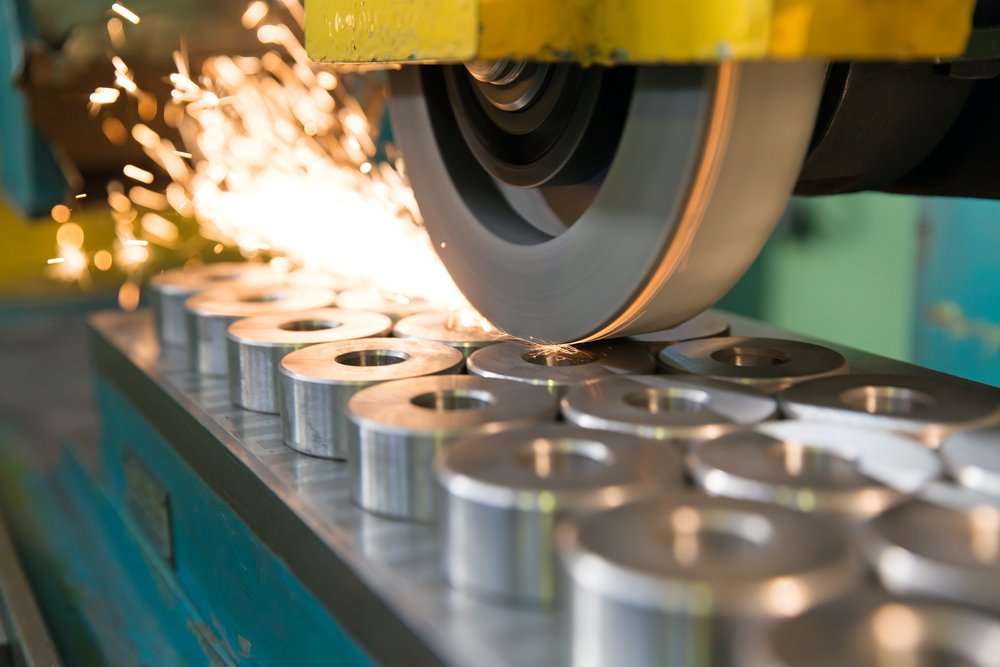
Precision Grinding
Precision grinding refines selected diameters, faces, and mating surfaces when the drawing calls for controlled geometry or finish. Grinding stock and heat-treatment sequence must be considered before the process plan is released.
Fitting and Inspection
Fitting confirms the practical relationship of mating features, while inspection follows the agreed critical-dimension plan. SUUXIANG keeps revision information and required reporting aligned with the order before delivery.
CNC Machined Threaded Adapters: Hardware and Identification Options
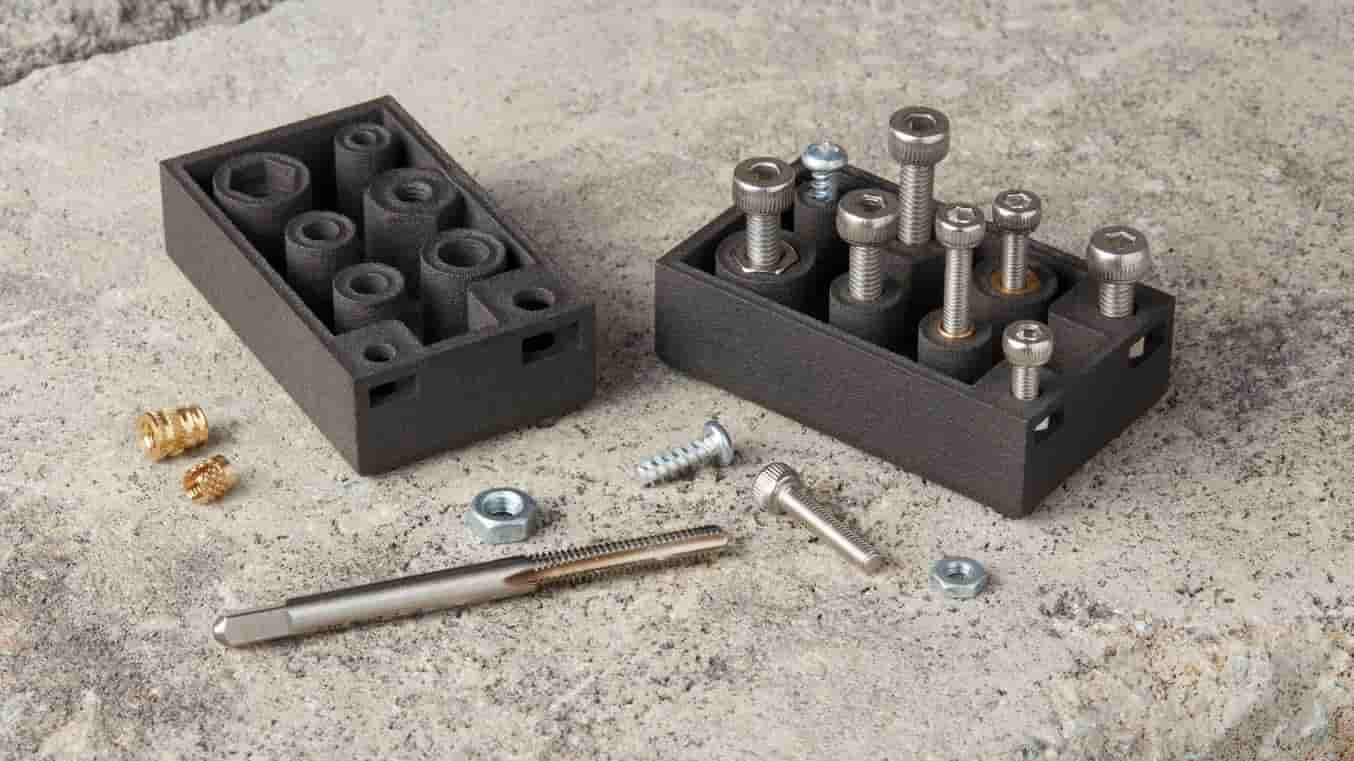
Threaded Inserts
Threaded inserts can support repeated assembly or provide a specified interface in a machined adapter. Material pairing, installation method, pull-out requirements, and the available wall thickness should be reviewed before production.

Sealing Features
O-ring grooves, sealing faces, and specified gasket interfaces can be machined where the drawing defines the mating condition. Seal size, groove geometry, surface requirements, pressure exposure, and assembly direction require application review.

Locating Features
Dowel holes, flats, shoulders, and anti-rotation details help establish repeatable orientation during assembly. Their datum relationship, positional tolerance, tool access, and interaction with adjacent components should be confirmed from the drawing.
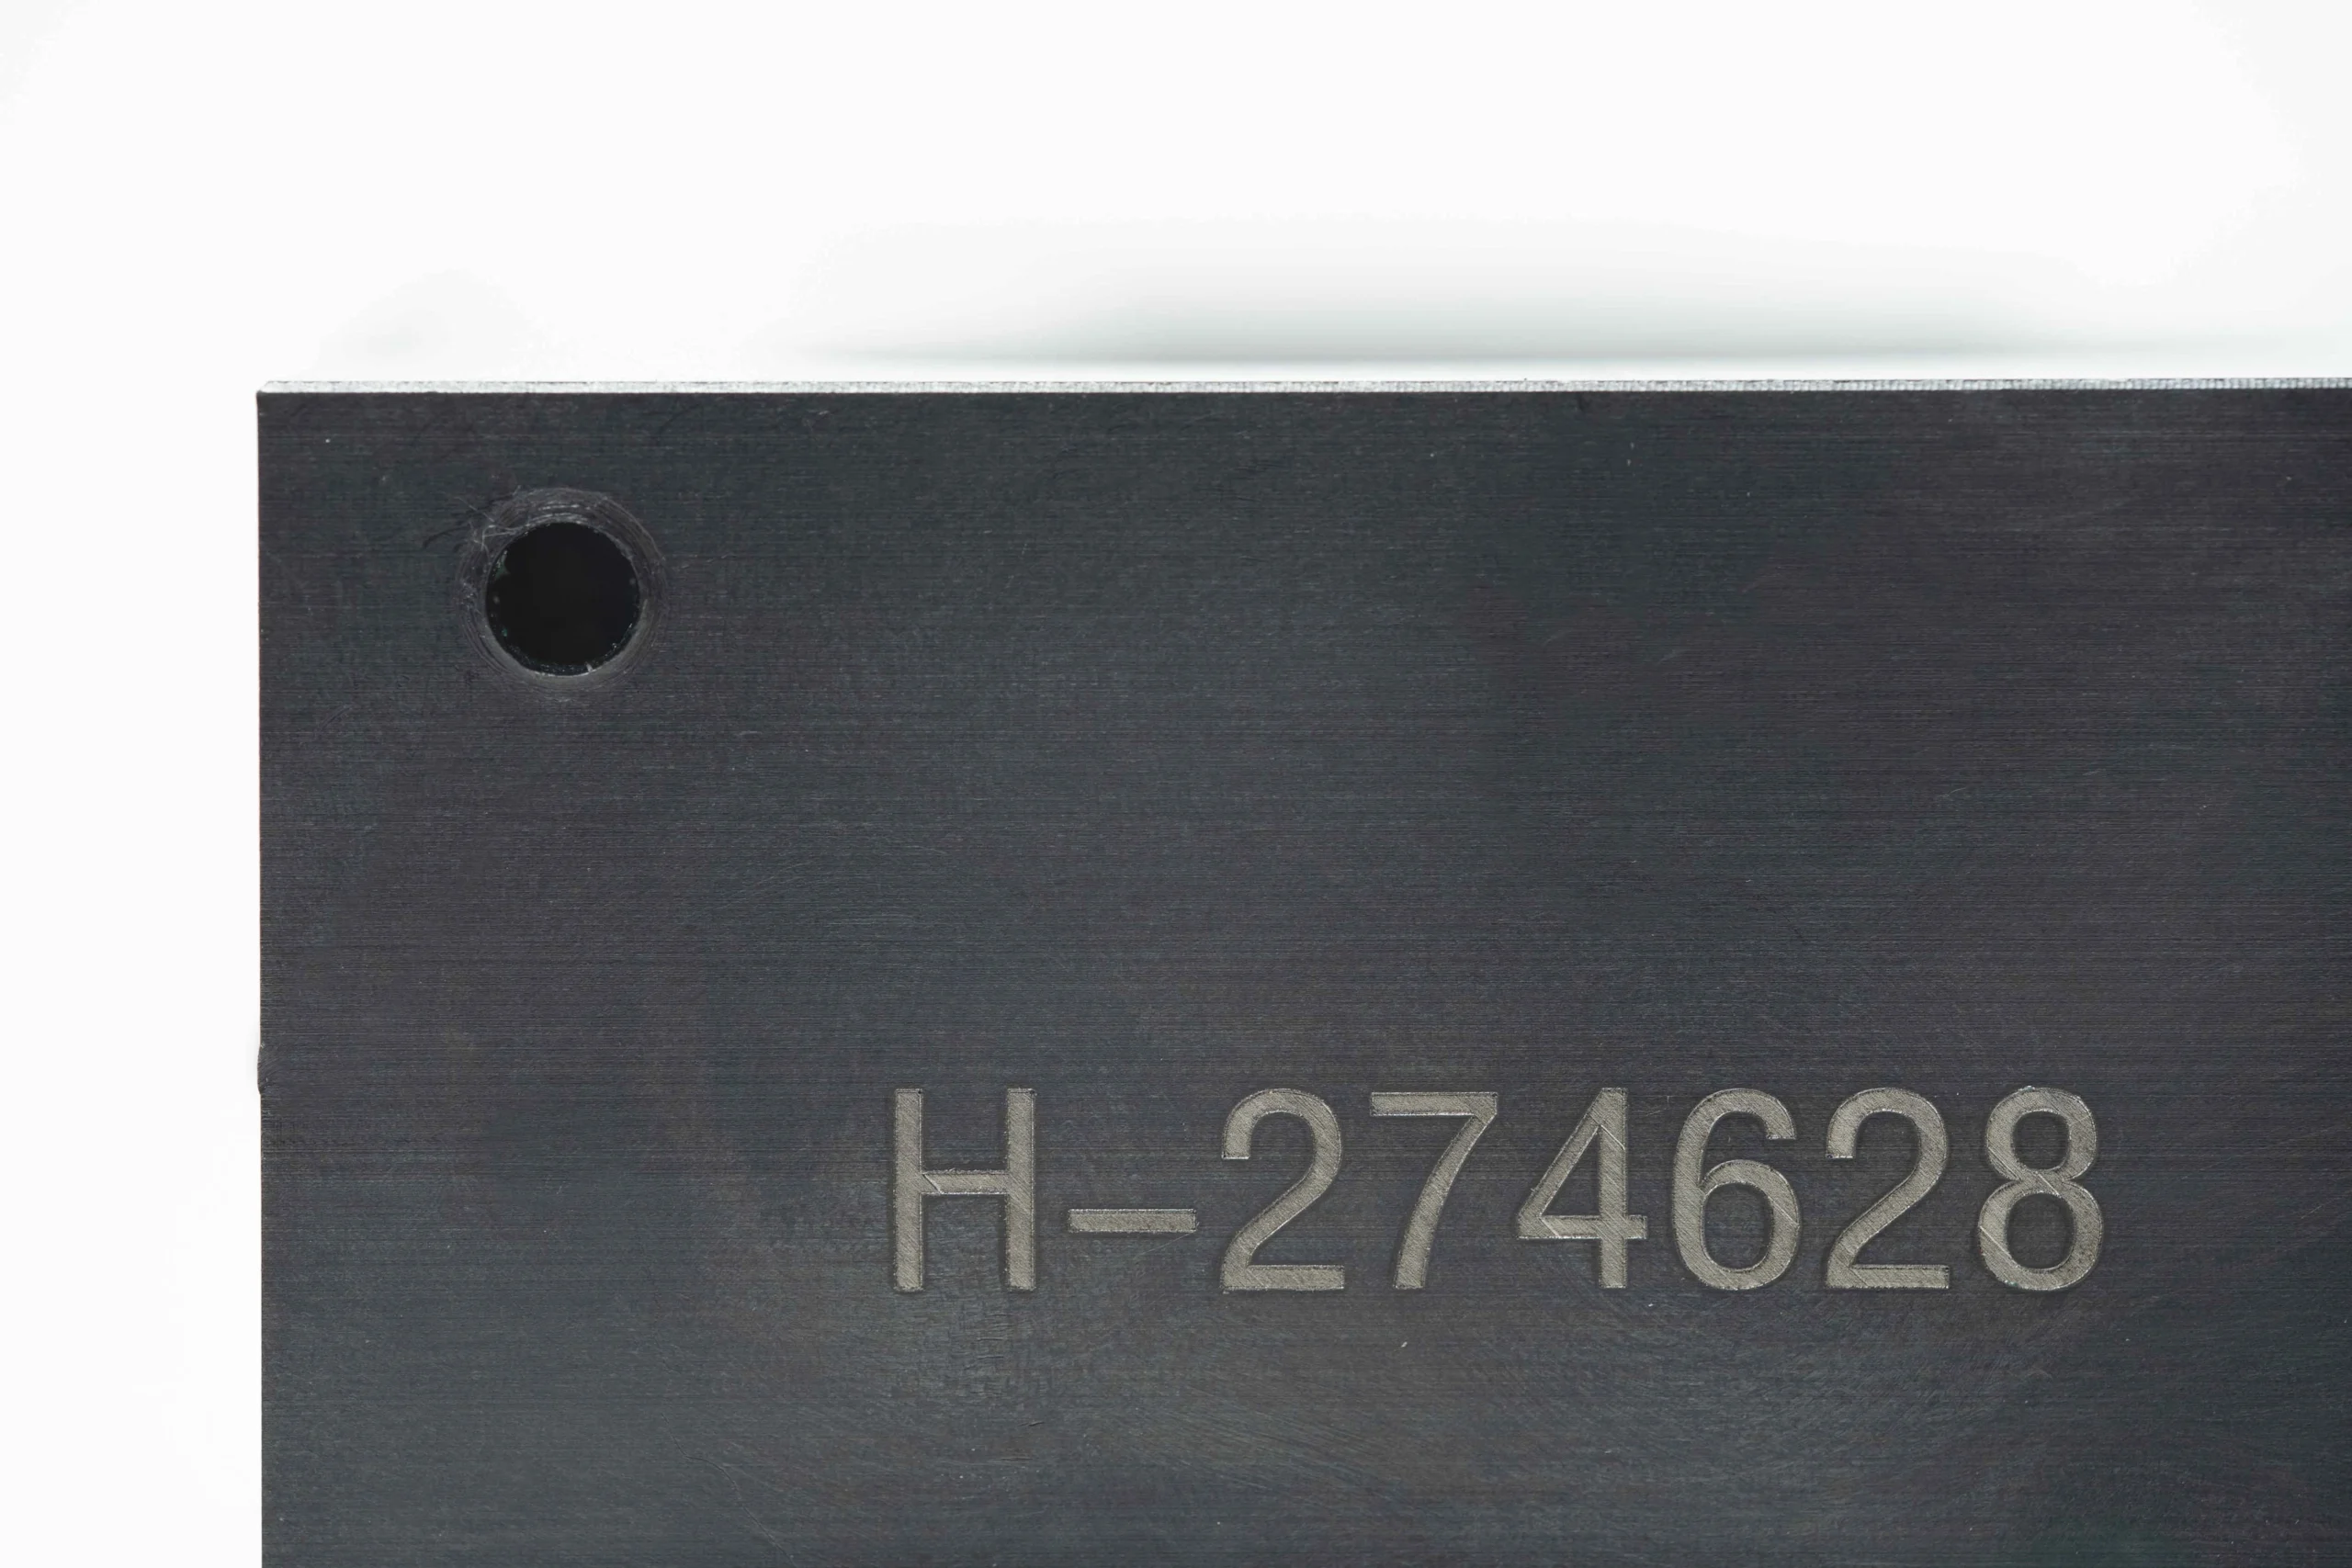
Identification Marks
Part numbers, revision marks, orientation indicators, and lot identifiers can support controlled assembly and traceability. Marking method, location, character size, and cosmetic limits should be specified so critical surfaces remain protected.

Protective Packaging
Protective caps, compartmented trays, and labeled packaging can reduce damage to threads and finished surfaces during handling and shipment. Packaging requirements should reflect part geometry, finish sensitivity, quantity, and receiving inspection needs.
CNC Machined Threaded Adapters, Built with Discipline
Established in 2010, SUUXIANG is the sole public-facing brand of Dongguan SuuXiang Precision Mold Co., Ltd., based in Chang’an Town, Dongguan, Guangdong, China. Founder and legal representative XiaoCheng Huang leads a company that helps international engineering, sourcing, and quality teams turn drawings and specifications into inspected custom machined parts, precision mold components, connector tooling, and die components.
Our practical scope combines CNC milling and turning, multi-axis machining, EDM, precision grinding, fitting, inspection, and controlled project coordination. For CNC machined threaded adapters, production planning begins with the drawing, thread callouts, datums, material requirements, surface needs, and the mating context that determines manufacturability.
What distinguishes SUUXIANG is a disciplined engineering workflow before commitments are made. We review critical dimensions, tool access, tolerance stack, machining and grinding allowance, inspection method, revision status, and delivery requirements so the agreed process route and final documentation match the order.

CNC Machined Threaded Adapters: Interface Control
DFM Before Commitments
SUUXIANG reviews the drawing, mating interface, datums and critical dimensions before quotation or production commitments. This establishes whether thread form, engagement length, sealing features and machining access can be controlled through a practical manufacturing route.
- Confirm thread callouts, class or fit requirements and mating-part context
- Identify critical diameters, concentricity and datum relationships
- Review tool access, relief geometry and deburring requirements
- Align material, heat treatment and surface requirements with the drawing

CNC and EDM Routing
CNC machined threaded adapters may require more than a turning operation when profiles, cross-holes, internal geometry or hardened features are involved. SUUXIANG plans CNC milling, turning, EDM and secondary operations around the specified geometry and inspection needs.
- Select turning and milling sequences around datum stability
- Assess wire EDM or sinker EDM needs for inaccessible features
- Plan machining allowance for subsequent finishing operations
- Keep the process route linked to the approved revision
Grinding and Fitting Strategy
Where interface performance depends on controlled seats, shoulders, locating diameters or mating alignment, grinding and fitting requirements should be defined early. SUUXIANG evaluates grinding stock, heat-treatment sequence and functional contact conditions before routing the part for final finishing.
- Define surfaces that require grinding rather than general machining
- Allow appropriate stock before heat treatment and final grinding
- Review contact faces, runout relationships and assembly clearance
- Clarify whether fitting is required against a mating component
Inspection With Revision Visibility
Inspection planning for threaded adapters begins with the dimensions that affect assembly and function. SUUXIANG aligns measurement methods, reporting expectations and revision control with the order so customers can review the evidence required for their quality process.
- Identify critical dimensions and their intended inspection methods
- Define thread, datum and surface-reporting requirements
- Maintain visibility of approved drawing revisions and changes
- Match final documentation to the verified inspection plan
Why Choose SUUXIANG for CNC Machined Threaded Adapters
Compare a documented, drawing-led workflow with the variable handoff often found at a generic machining supplier.
← Swipe left or right to view →
CNC Machined Threaded Adapters: From Drawing to Delivery
Each production route and delivery commitment is confirmed against the approved drawing, application requirements, and inspection plan.
Review Drawings and Requirements
We review drawings, models, material, quantity, thread callouts, mating context, critical dimensions, surface requirements, and requested inspection documentation before quotation.
Confirm DFM and Process
The project discussion identifies datum strategy, tool access, tolerance stack risks, machining allowance, heat-treatment sequence, and any EDM or grinding requirements.
Plan Controlled Production
After requirements are aligned, SUUXIANG defines the appropriate CNC turning, milling, multi-axis machining, EDM, grinding, fitting, and revision-control workflow.
Machine Critical Thread Features
Manufacturing follows the approved process route, with thread interfaces, functional datums, and specified surfaces managed according to the project’s documented priorities.
Inspect Pack and Coordinate
Completed parts are inspected against the agreed plan, then packed and prepared with order-matched documentation and shipment coordination confirmed for the project.
How to Source CNC Machined Threaded Adapters
Move from drawing review to inspection-linked delivery with a defined engineering and production workflow.
Submit Your Technical Package
Send 2D drawings, 3D models when available, material, quantity, thread callouts, critical dimensions, surface requirements, inspection needs, application context, and target delivery date.
Align the Manufacturing Plan
Review DFM findings, datum strategy, tool access, thread measurement approach, machining or EDM route, heat-treatment sequence, quotation assumptions, and prototype or sampling requirements.
Approve Production Details
Confirm the controlled revision, material requirements, critical-to-quality dimensions, agreed inspection plan, acceptance criteria, packaging needs, and delivery coordination before production begins.
Receive Verified Parts
SUUXIANG coordinates machining, EDM, grinding, fitting, and inspection as applicable, then provides delivery information and documentation aligned with the approved order and inspection plan.
Certifications and Quality Documentation
Customer Reference Publication Policy
Customer testimonial publication is pending written authorization and verified project-outcome evidence. SUUXIANG does not publish attributed performance, quality, or delivery results until the relevant customer and supporting records have been approved for public use.
Customer testimonial publication is pending written authorization and verified project-outcome evidence. Project-specific dimensional, inspection, and delivery results will be shared only when documentation and customer approval support an accurate public statement.
Customer testimonial publication is pending written authorization and verified project-outcome evidence. For a current RFQ, submit the drawing, critical dimensions, material, quantity, and inspection requirements so the production route can be reviewed against your application.
CNC Machined Threaded Adapters FAQ
Practical answers for drawing-led adapter projects, from prototype review through documented delivery.
What quantities can SUUXIANG quote for cnc machined threaded adapters?
How long do samples and production orders take?
Which materials and heat treatments can be specified for cnc machined threaded adapters?
What drawings and files are needed for a threaded adapter quote?
Can SUUXIANG provide inspection reports for custom threaded adapters?
How are shipping and payment arranged for an international order?
How does SUUXIANG control IP, drawing revisions, and production changes?
The Complete Buyer’s Guide to cnc machined threaded adapters
Use a practical decision framework to specify threaded interfaces, compare materials and finishes, assess supplier controls, and avoid costly drawing, tolerance, inspection, and sourcing mistakes before production.
1. What Are cnc machined threaded adapters?
Two threaded interfaces can be converted, joined, spaced, retained, or sealed by one drawing-defined adapter. CNC machined threaded adapters are precision parts whose thread form, engagement length, shoulders, bores, wrench features, and sealing faces must work with the mating assembly—not merely fit a nominal thread callout.
CNC turning produces concentric diameters, bores, faces, and external or internal threads; milling adds flats, cross-holes, ports, anti-rotation features, or non-round interfaces. Secondary operations such as deburring, tapping, grinding, or inspection may be necessary where burr direction, seating geometry, thread runout, or surface condition affects assembly function.
A custom part is usually preferable when a catalog fitting cannot meet the required interface combination, envelope, datum relationship, sealing arrangement, material condition, or traceability need. Before quoting, SUUXIANG should review the 2D drawing, 3D model, mating-part details, critical dimensions, thread standard, intended load or fluid path, and inspection requirements.
2. How Threaded Adapters Evolved
1841 marked the adoption of Joseph Whitworth’s 55-degree thread form in Britain, while 1864 brought William Sellers’ 60-degree form to U.S. practice. These standards made interchangeable fasteners and pipe-connected equipment practical, but they also left different flank angles, pitches, taper conventions and callout habits in installed equipment.
1947 saw the founding of ISO, accelerating international thread standardization without eliminating legacy inch, pipe and regional interfaces. As hydraulic, pneumatic and process-fluid systems expanded, adapters increasingly had to join dissimilar threads while preserving shoulder position, seal location and assembly access.
CNC turning and milling later made drawing-controlled adapters economical for short runs, compact envelopes and mixed-standard interfaces. Modern connector and fluid applications may combine fine threads, small bores, controlled concentricity and sealing features; therefore, a legacy mating standard, not the adapter’s outside shape, often determines the RFQ data and inspection approach.
3. Types of cnc machined threaded adapters
Six recurring configurations cover most cnc machined threaded adapters. Geometry alone is insufficient: the drawing must define thread callouts, sealing interfaces, engagement length, drive access, and load direction.
| Configuration | Primary Function | Drawing Distinction |
|---|---|---|
| Reducer | Convert interfaces | Both thread callouts and sealing face |
| Coupler | Extend or join | Gender, wrench access, engagement |
| Angled | Change routing | Angle, clocking, centerlines |
| Flanged | Carry clamp load | Seat datum and flange geometry |
| Hex custom | Transmit torque | Drive form and feature datums |
Male-To-Female Reducers
A male-to-female reducer converts size or thread form in a compact path. Specify both thread designations, hand, engagement length, bore transition, and the sealing face or taper.
Same-Gender Couplers
Male-to-male and female-to-female couplers join two matching interfaces. Show wrench clearance, thread reliefs, minimum wall thickness, and whether axial load or torque governs.
Straight And Angled Adapters
Straight bodies preserve in-line routing; angled bodies resolve access conflicts. Dimension the centerline angle, clocking reference, bend clearance, and sealing location on each port.
Flange And Shoulder Styles
Flanges distribute clamp load, while shoulders establish an axial stop. Define flange diameter, seating datum, contact finish, fastener pattern, and any gasket or O-ring groove.
Hex And Multi-Feature Interfaces
Hex bodies provide installation torque; custom interfaces can combine threads, bores, cross-holes, flats, and locating diameters. Identify the drive feature, torque direction, datums, and inspection-critical relationships.
4. Materials for cnc machined threaded adapters
Six material families cover most cnc machined threaded adapters. Select from load, service temperature, fluid or chemical exposure, mating material, mass target, and required finish—not unit price alone.
| Material | Strength / Weight | Exposure And Finish |
|---|---|---|
| Aluminum alloy | Moderate / low | Anodize; isolate from dissimilar metals |
| Stainless steel | High / medium | Corrosive service; passivate as specified |
| Carbon or alloy steel | High / medium | Coat against corrosion |
| Brass or copper alloy | Moderate / medium | Check media and galvanic pairing |
| Engineering polymer | Low–moderate / very low | Validate temperature, creep, and chemicals |
Match Material To Service
Aluminum suits low-mass, readily machined designs and accepts anodizing, but requires galvanic review beside stainless or copper alloys.
Stainless steel suits wet or corrosive exposure; specify grade, chloride environment, and passivation requirements in the drawing.
Check Load And Media
Carbon and alloy steels provide high strength but usually need coating or controlled environments. Brass machines well and suits many fittings, while copper alloys require media and galvanic compatibility review.
Engineering polymers can reduce mass and resist selected chemicals, but temperature, creep, thread engagement, and pressure must be validated.
Specify The Complete Condition
Two parts with identical base metal can perform differently after heat treatment, plating, passivation, or anodizing. State mating materials, media, temperature range, finish, and corrosion test expectations before routing production.
5. Custom Features and Surface Finishes
Two functional interfaces often drive adapter customization: the thread system and the sealing or torque feature. Specify both on the drawing, with datums and any protected surfaces clearly identified.
| Finish | Primary Purpose | Dimensional Effect | Corrosion Or Cosmetic Need |
|---|---|---|---|
| Anodizing | Aluminum protection | Build-up requires allowance | Corrosion and color |
| Passivation | Stainless cleaning | Minimal change | Corrosion support |
| Plating | Protection or conductivity | Thickness controlled | Corrosion or appearance |
| Black oxide | Low-glare appearance | Minimal build-up | Limited corrosion protection |
| Bead blasting | Uniform texture | Can alter fine edges | Cosmetic preparation |
| Deburring | Remove sharp edges | Edge break specified | Functional handling |
Interface Features
Two thread standards can coexist only when pitch, engagement, and runout are defined.
One wrench-flat, knurl, cross-hole, shoulder, or O-ring groove changes tool access and inspection requirements.
Finish By Function
One finish should be selected for a stated function, not appearance alone.
0.000 mm nominal dimensional change is never assumed; coating thickness belongs in the tolerance review.
Marking And Presentation
Laser marking supports part identification, revision traceability, and orientation marks.
One bead-blasted cosmetic surface still needs a defined mask boundary near threads and sealing faces.
6. Construction and Quality Control Essentials
One adapter drawing should define the functional thread and the datum chain before production. Assembly reliability depends on mating geometry, not nominal diameter alone.
Thread Definition And Engagement
Each thread callout should state standard, size, pitch, class, handedness, and whether it is internal or external. Specify the required minimum full-thread engagement and identify any thread-relief requirement.
Datums And Functional Geometry
Two or more functional datums should control faces, bores, and thread axes. State concentricity or runout relative to the mating datum, plus chamfer dimensions, burr limits, sealing-land geometry, and finish where these affect assembly.
Inspection Evidence
Go/no-go gauges efficiently verify thread acceptance, while a CMM can report datum-related runout and sealing features. Require visual burr checks and a first-article record listing measured critical dimensions, gauge status, revision, sample quantity, and acceptance result.
7. Choosing a Threaded Adapter Manufacturer
A supplier decision should begin with the released drawing, not a generic capability list. For cnc machined threaded adapters, compare how each candidate converts thread, datum, sealing, and inspection requirements into a controlled route.
| Evaluation Area | Evidence To Request | Award Question |
|---|---|---|
| Drawing review | Marked-up DFM response | Are risks and assumptions explicit? |
| Inspection | Sample report and gauge plan | How are critical threads verified? |
| Traceability | Material and revision records | Can each lot match the order? |
| Packaging | Protection proposal | How are threads protected in transit? |
Review The Drawing
Before award, request written DFM feedback identifying inaccessible features, thread callout ambiguities, datum conflicts, and deburring risks. Ask the supplier to distinguish assumptions from drawing requirements.
Verify Production Evidence
For one comparable part, request a redacted inspection report, material traceability example, proposed gauge plan, and explanation of the machining sequence. Discuss how turning, milling, EDM, or grinding would protect critical features.
Control Changes And Delivery
Before prototype release, define revision ownership, approval records, report format, lot identification, and packaging protection for threads and finished surfaces. Confirm that prototype findings, gauges, and process decisions transfer into later production.
8. Common Sourcing Mistakes to Avoid
Eight release errors repeatedly turn a straightforward adapter into a fit, seal, or traceability problem. Resolve each against the mating assembly and approved drawing before machining begins.
Thread Definition Gaps
Thread size alone is incomplete without standard, pitch, class, handedness, and engagement length; the result can be a part that starts but will not mate correctly. Ask: Which complete thread callout and acceptance gauge apply?
Nominal Dimensions And Fits
A nominal diameter is not an actual functional size when tolerances, datums, and mating material are unstated; interference, looseness, or thread damage can follow. Ask: What finished limits must this feature meet against the specified counterpart?
Finish And Sealing Assumptions
A cosmetic finish may alter contact surfaces, while an undefined seal method leaves leak performance untestable. Ask: Is sealing by thread, gasket, O-ring, taper, or face—and which surfaces must remain masked or controlled?
Sample And Revision Control
A sample approval without inspection criteria accepts appearance rather than verified CTQs, and informal drawing edits create mixed revisions in production. Ask: Which dimensions, surface defects, records, and revision identifier must be approved before release?
9. From Drawing to Production Launch
A controlled launch for cnc machined threaded adapters converts design intent into a release package. It prevents thread, sealing, mating, inspection, and revision assumptions from reaching the shop floor.
Define Interfaces And Characteristics
Before RFQ, engineering should provide the mating-part drawing, thread designation, engagement requirement, sealing method, datum scheme, and application environment.
Critical characteristics should identify thread gauges, concentricity, sealing faces, wrench features, and any dimensions that affect assembly.
Close The Manufacturing Package
During DFM review, SUUXIANG can assess tool access, turning versus milling route, burr control, finish sequence, and inspection access against the supplied requirements.
Procurement should lock material, heat treatment, finish, quantity, delivery target, packaging, and required reports before approving a prototype or first article.
Release And Control Revisions
After first-article acceptance, quality should approve the inspection plan, sample basis, traceability fields, and protection for threads and sealing surfaces.
For repeat orders, procurement should reference the approved drawing revision; engineering must issue changes formally, and quality should confirm whether requalification is required.
10. cnc machined threaded adapters Pricing
3 quantity bands are useful for comparing cnc machined threaded adapters: prototype, bridge, and repeat production. Unit cost usually falls as programming, workholding, first-article setup, and inspection planning are spread across more parts; it does not fall if each revision changes the route.
2 quotation controls matter most: define every thread standard, datum, tolerance, material condition, finish, and acceptance method on the drawing, then state quantity and required delivery date. Include any certificates, inspection report, protective packaging, and mating-part context so suppliers quote the same scope rather than an assumed baseline.
| Quantity band | Primary cost drivers | Quotation evidence |
|---|---|---|
| 1–10 | Programming, setup, material minimums, first-piece inspection | 2D/3D files; revision; critical threads |
| 11–100 | Cycle time, tool wear, tolerance, deburring or secondary operations | Material; finish; inspection sampling |
| 100+ | Cycle stability, fixturing, packaging, delivery releases | Forecast; pack quantity; release schedule |
Upload Your Drawing for CNC Machined Threaded Adapters
Include material, quantity, critical dimensions, inspection expectations, and target delivery date so SUUXIANG can review manufacturability before quotation.