
CNC Fixtures for Battery Welding From Your Drawings
Submit your battery-welding fixture drawing for DFM, critical-dimension review, and a planned CNC, EDM, grinding, and inspection workflow.
Representative Precision Components for Battery-Welding Fixture Development





Related Drawing-Based Components and Quotation


Engineering Advantages for CNC Fixtures for Battery Welding
Manufacturing decisions organized around your drawing, critical dimensions, and inspection requirements.
DFM Before Quotation
Before quotation, we review critical dimensions, material, electrode access, clamping intent, and manufacturability questions documented in your drawing package.
Datum-Led Planning
We translate locating, clamping, and critical features into datum-led machining plans that help manage tolerance stack and inspection alignment.
Integrated Process Routes
CNC machining, wire or sinker EDM, precision grinding, and fitting are planned around access, geometry, required finish, and functional interfaces.
Inspection Planning
Inspection planning identifies measurement methods, report requirements, and critical-to-quality dimensions before production, so final documentation matches the verified order plan.
Revision Visibility
Controlled revision visibility keeps drawing changes, manufacturing questions, and delivery information clear throughout the project, reducing avoidable interpretation risk.
Traceable Communication
Traceable communication connects drawing requirements, process decisions, inspection expectations, and shipment records, giving sourcing and quality teams a clearer review path.
CNC Fixtures and Precision Tooling Families
Configure each family from your drawing, critical dimensions, material, inspection requirements, and battery-welding or mating-component context.

CNC Machining Services
Precision CNC machining services for drawing-based fixtures, tooling components, and custom machined parts. Process planning considers datums, critical dimensions, material condition, tool access, inspection needs, and the production route required before quotation.
Upload a Drawing
CNC Milling
Custom CNC milling services for fixture plates, nests, clamps, mold inserts, and shaped tooling features. Review focuses on workholding, machining access, wall geometry, tolerances, and whether subsequent EDM or grinding is needed.
Upload a Drawing
CNC Turning
Precision CNC turning services for rotational components such as pins, sleeves, bushings, shafts, and locating elements. Drawings should define functional diameters, concentricity, surface requirements, material condition, and inspection priorities.
Upload a Drawing
5-Axis Machining
5-axis CNC machining supports complex fixture geometry, contoured mold features, and multi-face components where fewer setups may protect datum relationships. Feasibility depends on tool reach, workholding, feature access, material, and inspection strategy.
Upload a Drawing
Swiss & Micro Machining
Swiss machining and micro machining support small, detail-sensitive pins, shafts, sleeves, and connector-tooling features. Review diameter-to-length relationships, handling risk, burr control, critical features, material, and measurement methods before committing a route.
Upload a Drawing
Wire & Sinker EDM
Wire EDM and sinker EDM services address hardened materials, narrow slots, internal profiles, sharp-feature requirements, and forms beyond practical cutting-tool access. Electrode design, wire path, flushing, finish, recast-layer considerations, and downstream fitting should be reviewed.
Upload a Drawing
Precision Grinding
Precision surface and profile grinding establishes controlled faces, profiles, and fit-critical dimensions after machining or heat treatment. Grinding stock, datum sequence, flatness or parallelism requirements, wheel access, and inspection method guide planning.
Upload a Drawing
Mold Core & Cavity Inserts
Precision mold core and cavity inserts are configured from molding function, material, parting-line geometry, cooling or venting needs, critical dimensions, and finish requirements. CNC, EDM, grinding, fitting, and inspection are planned around the approved drawing.
Upload a Drawing
Ejector & Ejection Components
Ejector pins, sleeves, and ejection components require attention to motion, clearance, bearing length, material condition, heat treatment, and wear surfaces. Supply begins with verified dimensions and mating-component context, not assumed standard configurations.
Upload a Drawing
Core Pins, Guide & Locating Components
Core pins, guide pins, and locating components are planned around datum control, mating fits, guidance travel, wear, and assembly relationships. Drawings should identify critical diameters, tolerances, material or hardness requirements, and inspection expectations.
Upload a Drawing
Slides, Lifters, Gates & Mold Accessories
Mold slides, lifters, gates, and accessories are configured for movement, shutoff, alignment, wear, and mating interfaces. Review slide travel, interference risks, datum references, machining access, EDM requirements, and fitting responsibility before production.
Upload a Drawing
Connector Mold Components
Precision connector mold components support fine-pitch, multi-cavity, and contact-feature tooling where positional relationships matter. Engineering review addresses micro features, steel selection, EDM strategy, polish needs, mating components, and inspection of critical geometry.
Upload a Drawing
Stamping Die Components
Precision stamping die components include punches, dies, guides, plates, and locating elements built to drawing-defined geometry. Material, heat-treatment sequence, clearance relationships, wear areas, wire-EDM path, grinding stock, and inspection criteria require confirmation.
Upload a Drawing
Injection, MIM, CIM & Overmolding Tooling
Injection mold components and tooling for MIM, CIM, and overmolding applications are assessed within verified production scope. Drawings and application context help define geometry, material, finish, dimensional priorities, molding interfaces, and the suitable CNC, EDM, or grinding sequence.
Upload a Drawing
Machining Materials
CNC machining materials are selected against drawing requirements, functional loads, corrosion exposure, machinability, heat-treatment needs, and mating conditions. Submit the specified grade, material standard, required condition, and any approved substitution rules with the RFQ.
Upload a Drawing
Surface Finishes & Heat Treatment
Surface finishing and heat treatment are planned as controlled requirements tied to function, wear, corrosion, appearance, or molding performance. Specify finish target, hardness or treatment requirement, dimensional impact, masking needs, and post-treatment inspection priorities.
Upload a Drawing
Quality, Metrology & Documentation
Precision inspection, metrology, and quality documentation are aligned to the drawing and agreed inspection plan. Identify critical dimensions, datum references, measurement methods, report format, revision status, traceability needs, and any customer-specific quality requirements.
Upload a Drawing
Prototyping & Low-Volume Production
Rapid prototyping and low-volume manufacturing support drawing-driven validation, fixture iteration, replacement tooling components, and controlled initial runs. Provide quantity, revision status, material, critical dimensions, inspection needs, and target date so the production route can be assessed.
Upload a DrawingMaterials for CNC Fixtures for Battery Welding

Aluminum Alloys
A lightweight, rigid option for fixture bases, nests, and structural plates where fast handling matters. CNC-machined aluminum supports complex geometry, but drawing review should address wear surfaces, grounding requirements, and protective finishing.

Stainless Steel
A durable choice for locating pins, clamp bodies, and exposed fixture hardware in demanding production environments. Its corrosion resistance suits repeated handling, while grade selection and heat-treatment requirements should follow load and wear conditions.
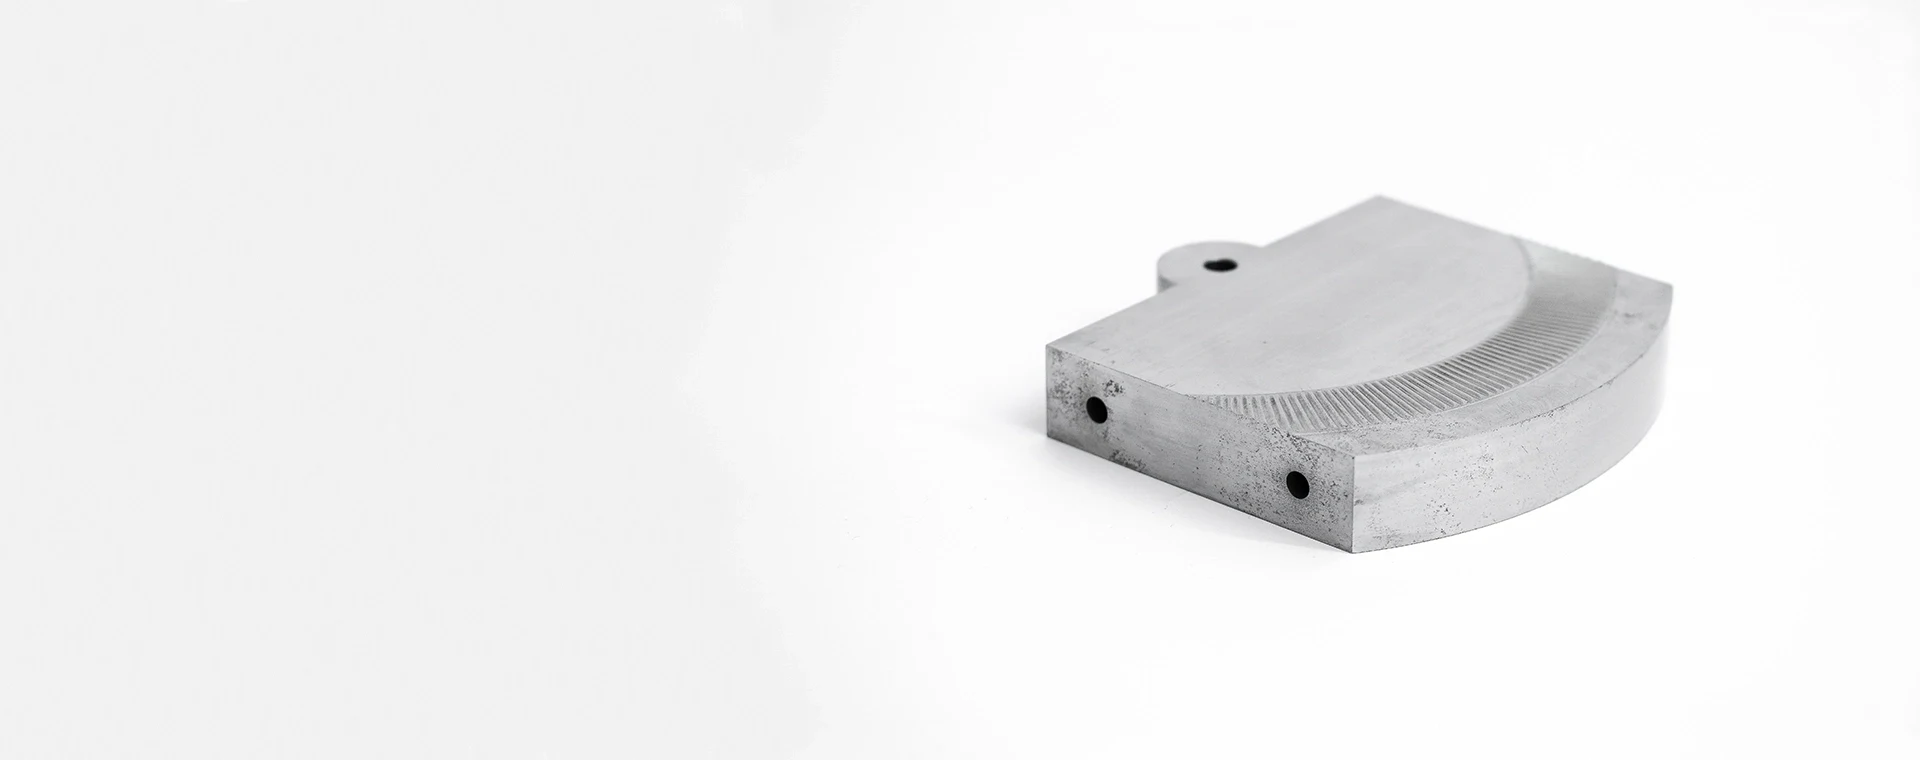
Tool Steel
A robust material for hardened locating features, guides, and high-cycle contact components. Tool steel can provide strong wear resistance after the specified heat-treatment route, but grinding allowance, EDM strategy, and final inspection points require definition.
Engineering Plastics
A nonconductive option for cell-support nests, separators, and contact-adjacent elements where surface protection is important. Material grade should be selected around heat exposure, dimensional stability, clamping force, and the required insulation path.
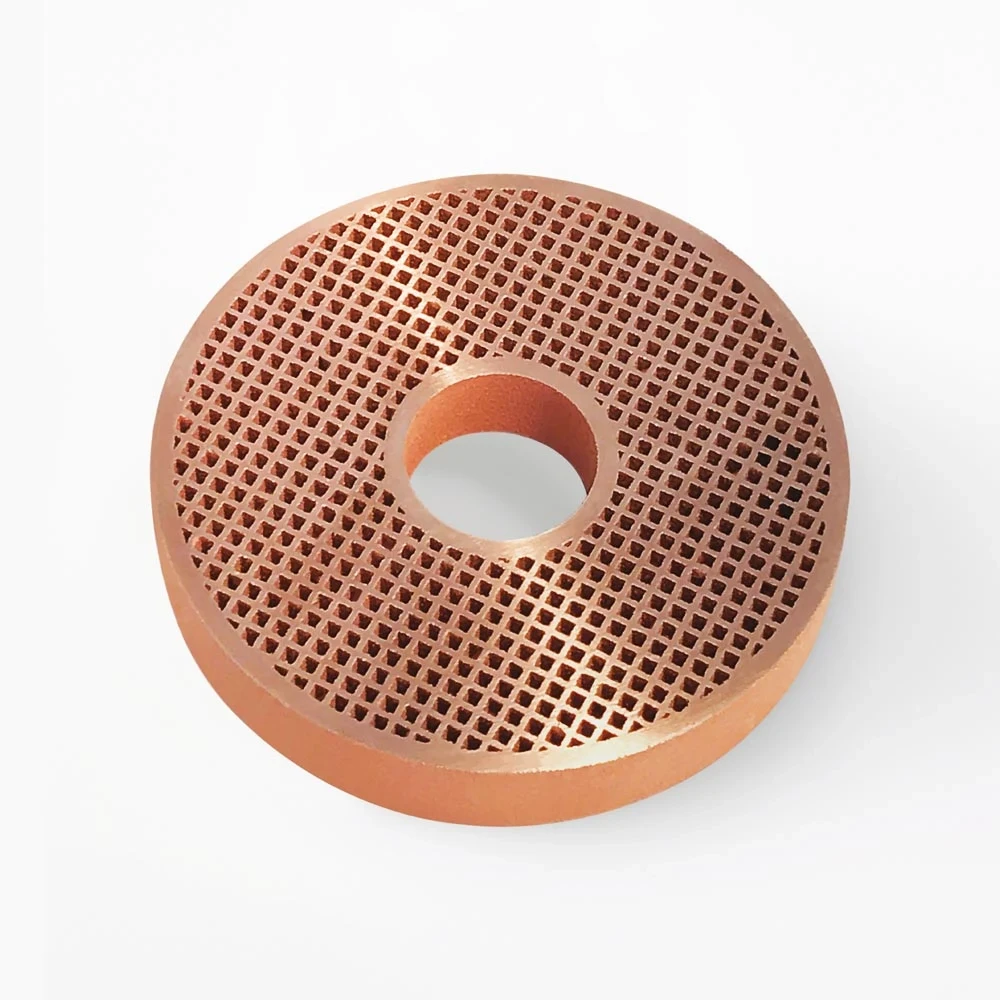
Copper Alloys
A conductive choice for specified current-carrying interfaces or electrode-related fixture components. Copper alloys offer useful electrical performance, yet their softer machining behavior, heat management, interface wear, and mating-part requirements should be confirmed from the drawing.
Processes for Battery Fixture Manufacturing
CNC Milling
CNC milling forms pockets, locating features, mounting faces, and complex prismatic geometry. Drawing review confirms cutter access, workholding approach, machining allowance, and the critical dimensions that require planned inspection.
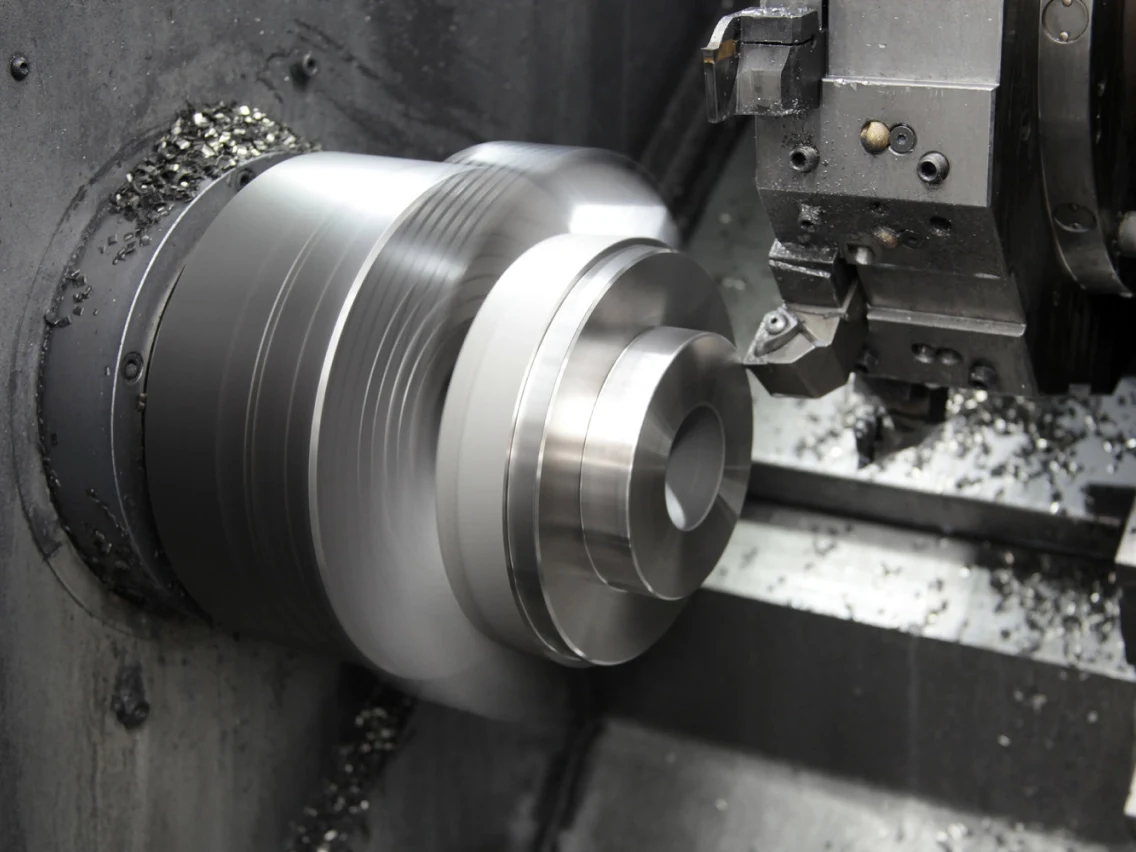
CNC Turning
CNC turning produces concentric cylindrical features such as pins, bushings, sleeves, and threaded interfaces. It supports controlled relationships between diameters, shoulders, and datums when rotational geometry is central to the fixture design.
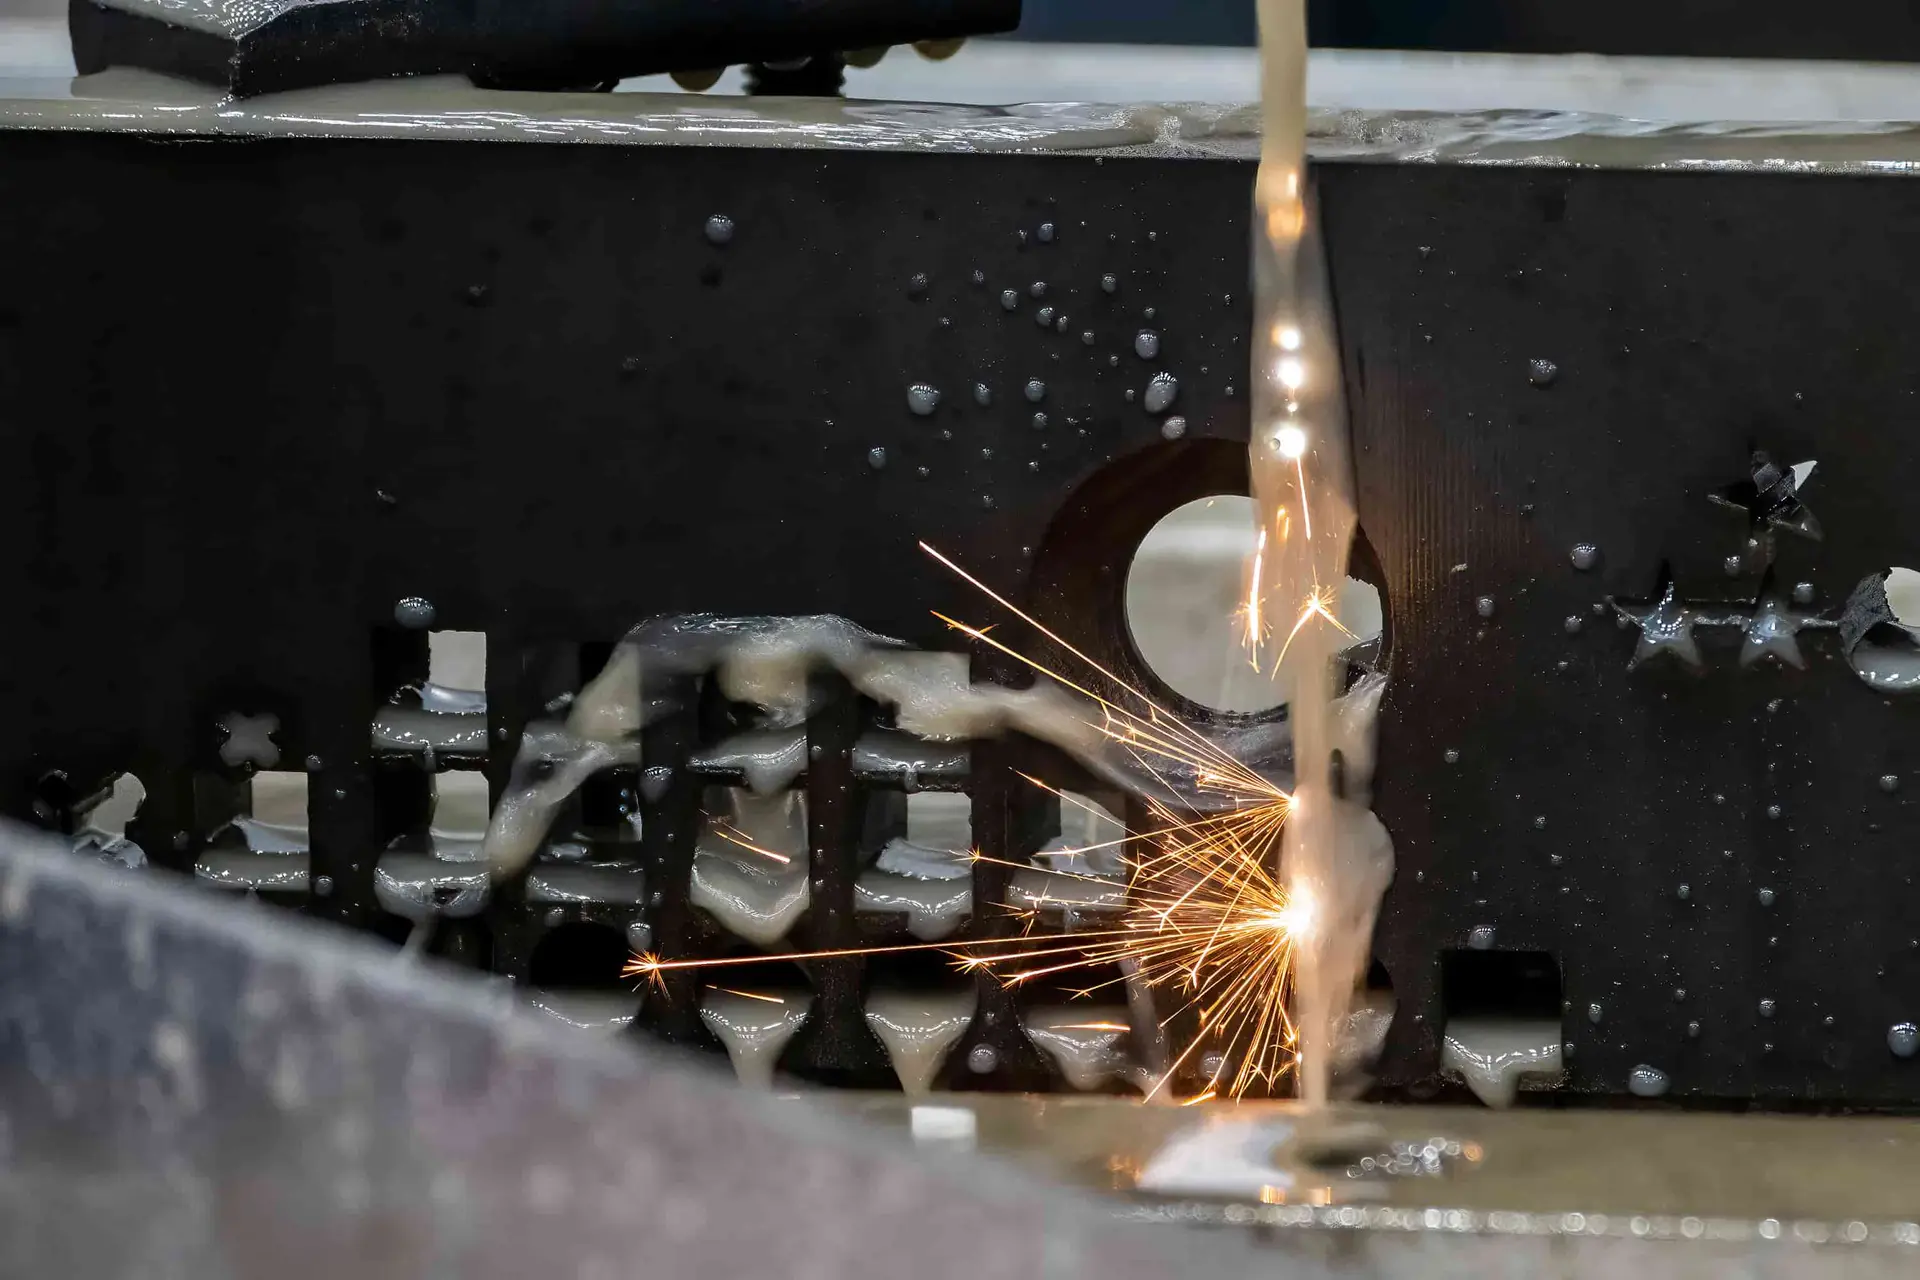
Wire EDM
Wire EDM cuts precise profiles, narrow slots, and internal contours where conventional cutter access is limited. The wire path, start-hole location, corner requirements, and datum relationship should be reviewed against the drawing.
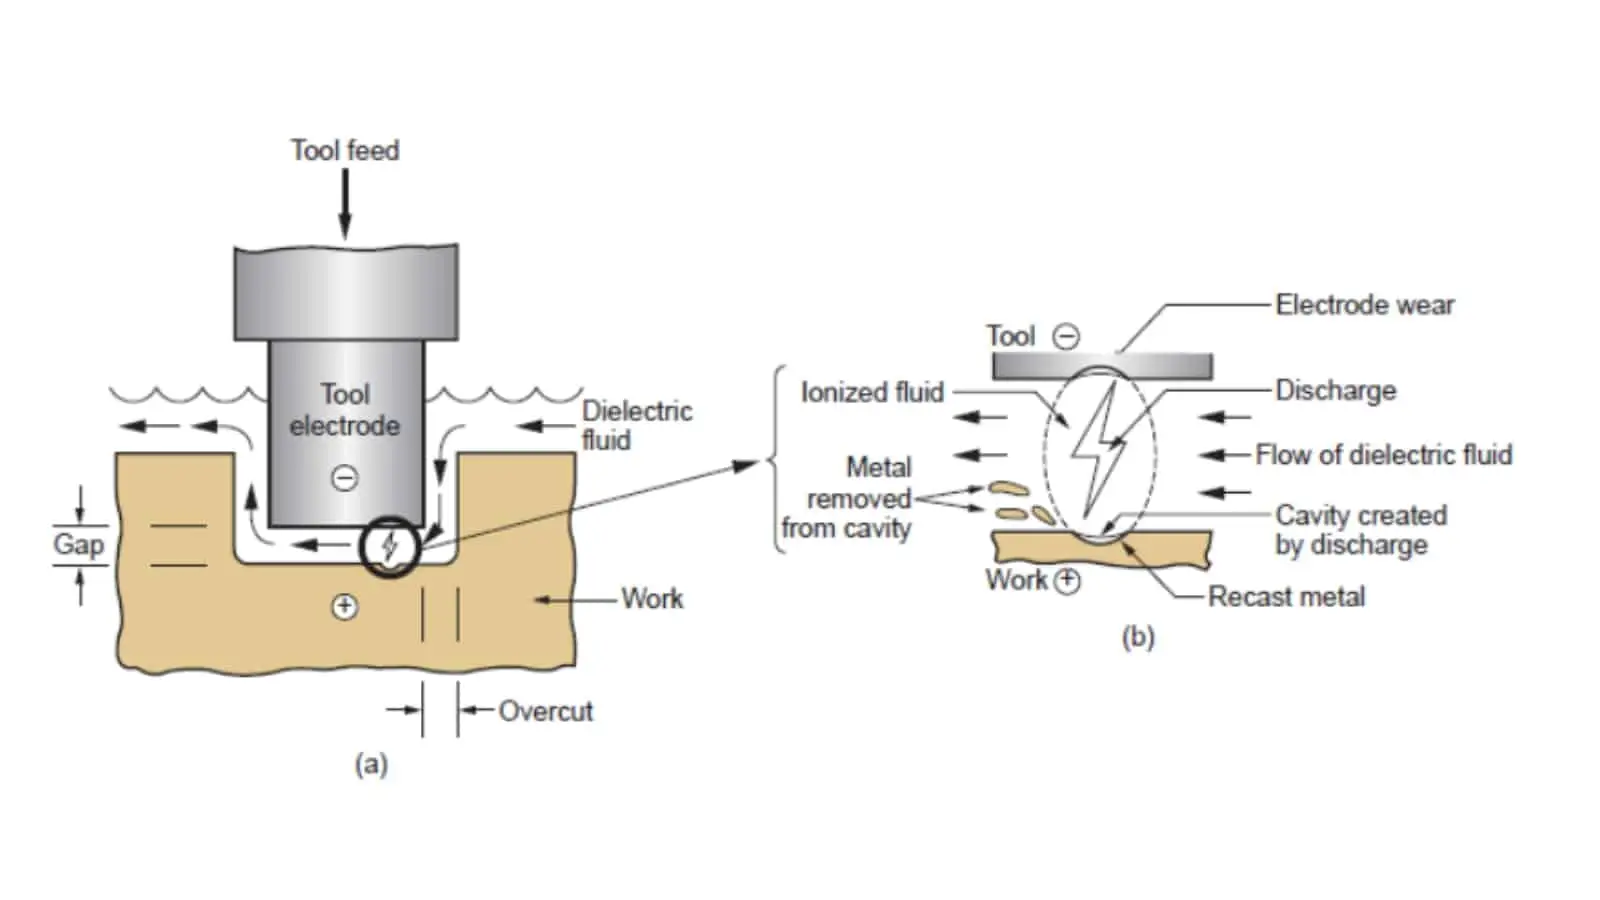
Sinker EDM
Sinker EDM creates deep cavities, sharp internal details, and difficult-to-reach features using planned electrodes. Electrode strategy, surface expectations, and subsequent finishing requirements are evaluated as part of the manufacturing route.
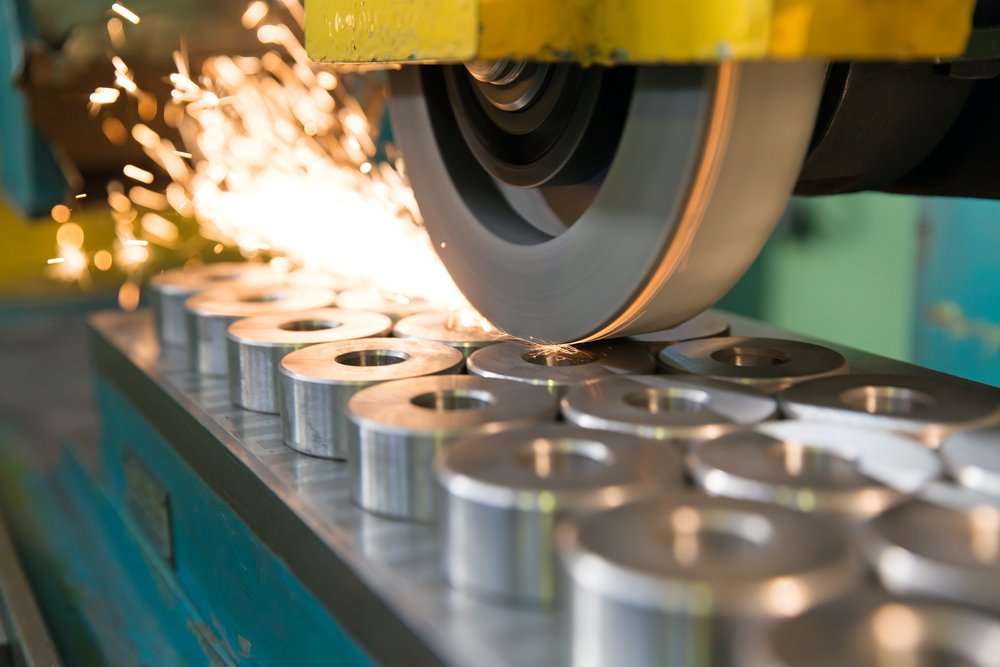
Precision Grinding
Precision grinding refines critical faces, diameters, and locating surfaces after machining or heat-treatment stages where applicable. Grinding stock, datum control, surface requirements, and inspection method should be defined before work begins.
Fitting and Inspection
Fitting verifies mating relationships among fixture components, while inspection checks agreed critical dimensions against the order plan. Revision control, assembly context, and required reports help keep the finished fixture aligned with its drawing.
CNC Fixtures for Battery Welding: Hardware and Applied Accessories

Locating Pins
Hardened locating pins establish repeatable part position from defined datums. Pin diameter, fit, insertion direction, and replacement access should be reviewed against cell, tab, busbar, or carrier geometry before production.

Guide Elements
Guide bushings, rails, and alignment features control fixture travel and mating alignment. Their selection should account for cycle motion, side-load risk, lubrication access, and the tolerance stack between moving and fixed fixture sections.

Clamping Components
Toggle clamps, screw clamps, or custom hold-down elements secure workpieces while preserving weld-head access. Clamp force, contact surface, opening clearance, and operator reach should match the assembly sequence and material sensitivity.
Fixture Fasteners
Specified screws, dowels, threaded inserts, and captive hardware support controlled assembly and maintenance. Fastener locations should remain accessible without disturbing critical datum features or requiring unnecessary fixture disassembly during service.
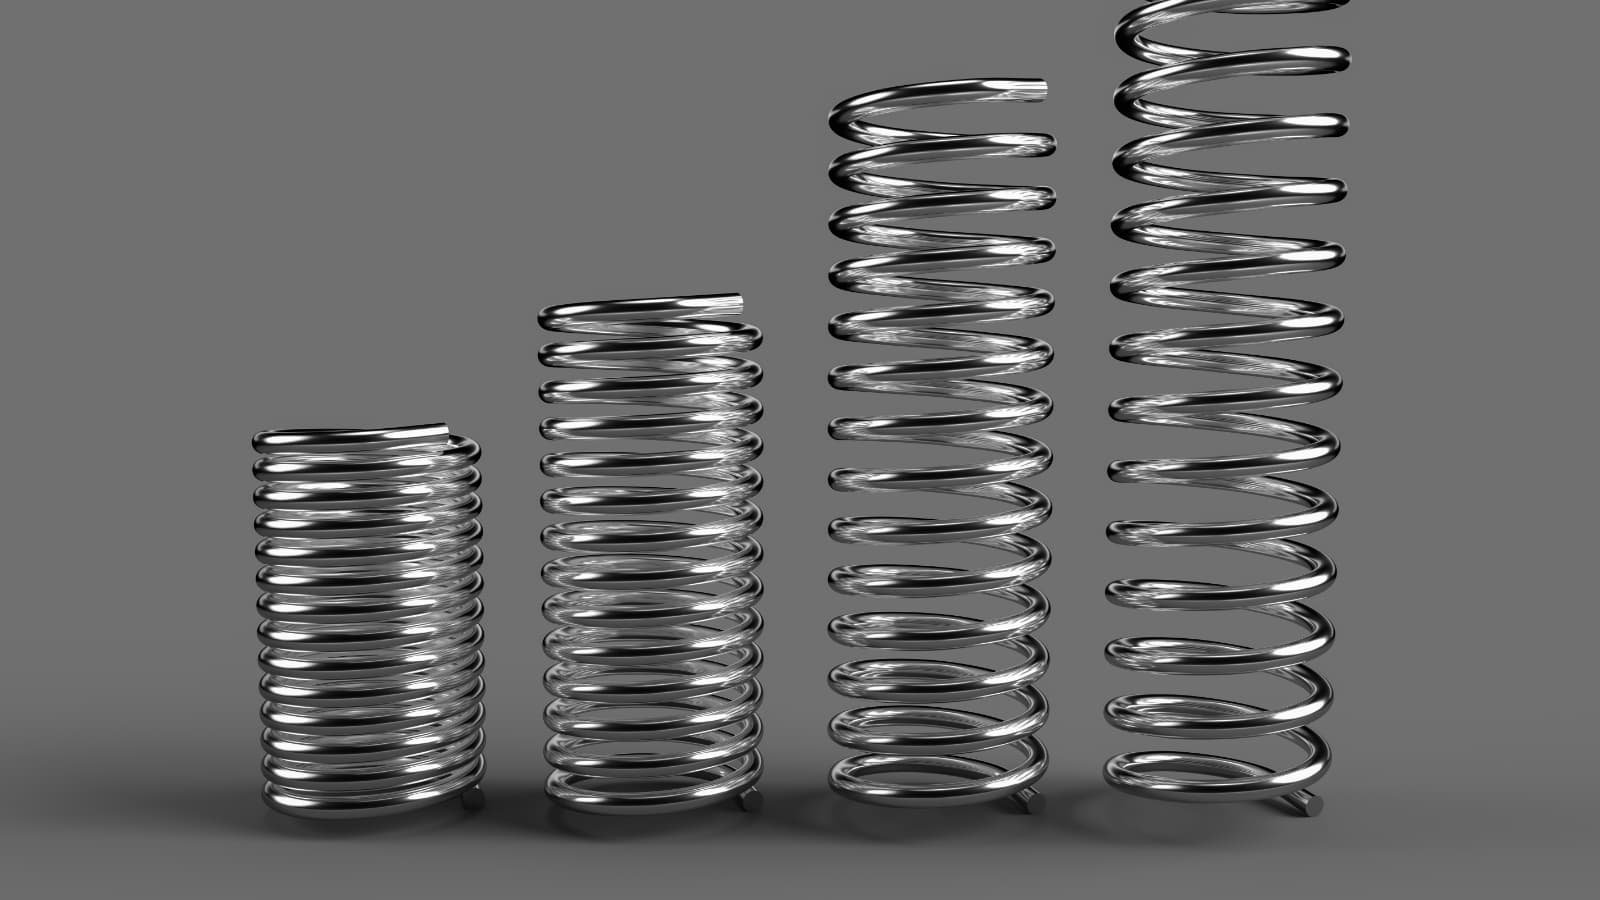
Return Springs
Compression springs and return mechanisms help restore movable nest, clamp, or guide elements between cycles. Define travel, preload, working environment, and replacement method so the fixture supports consistent operation and practical maintenance.
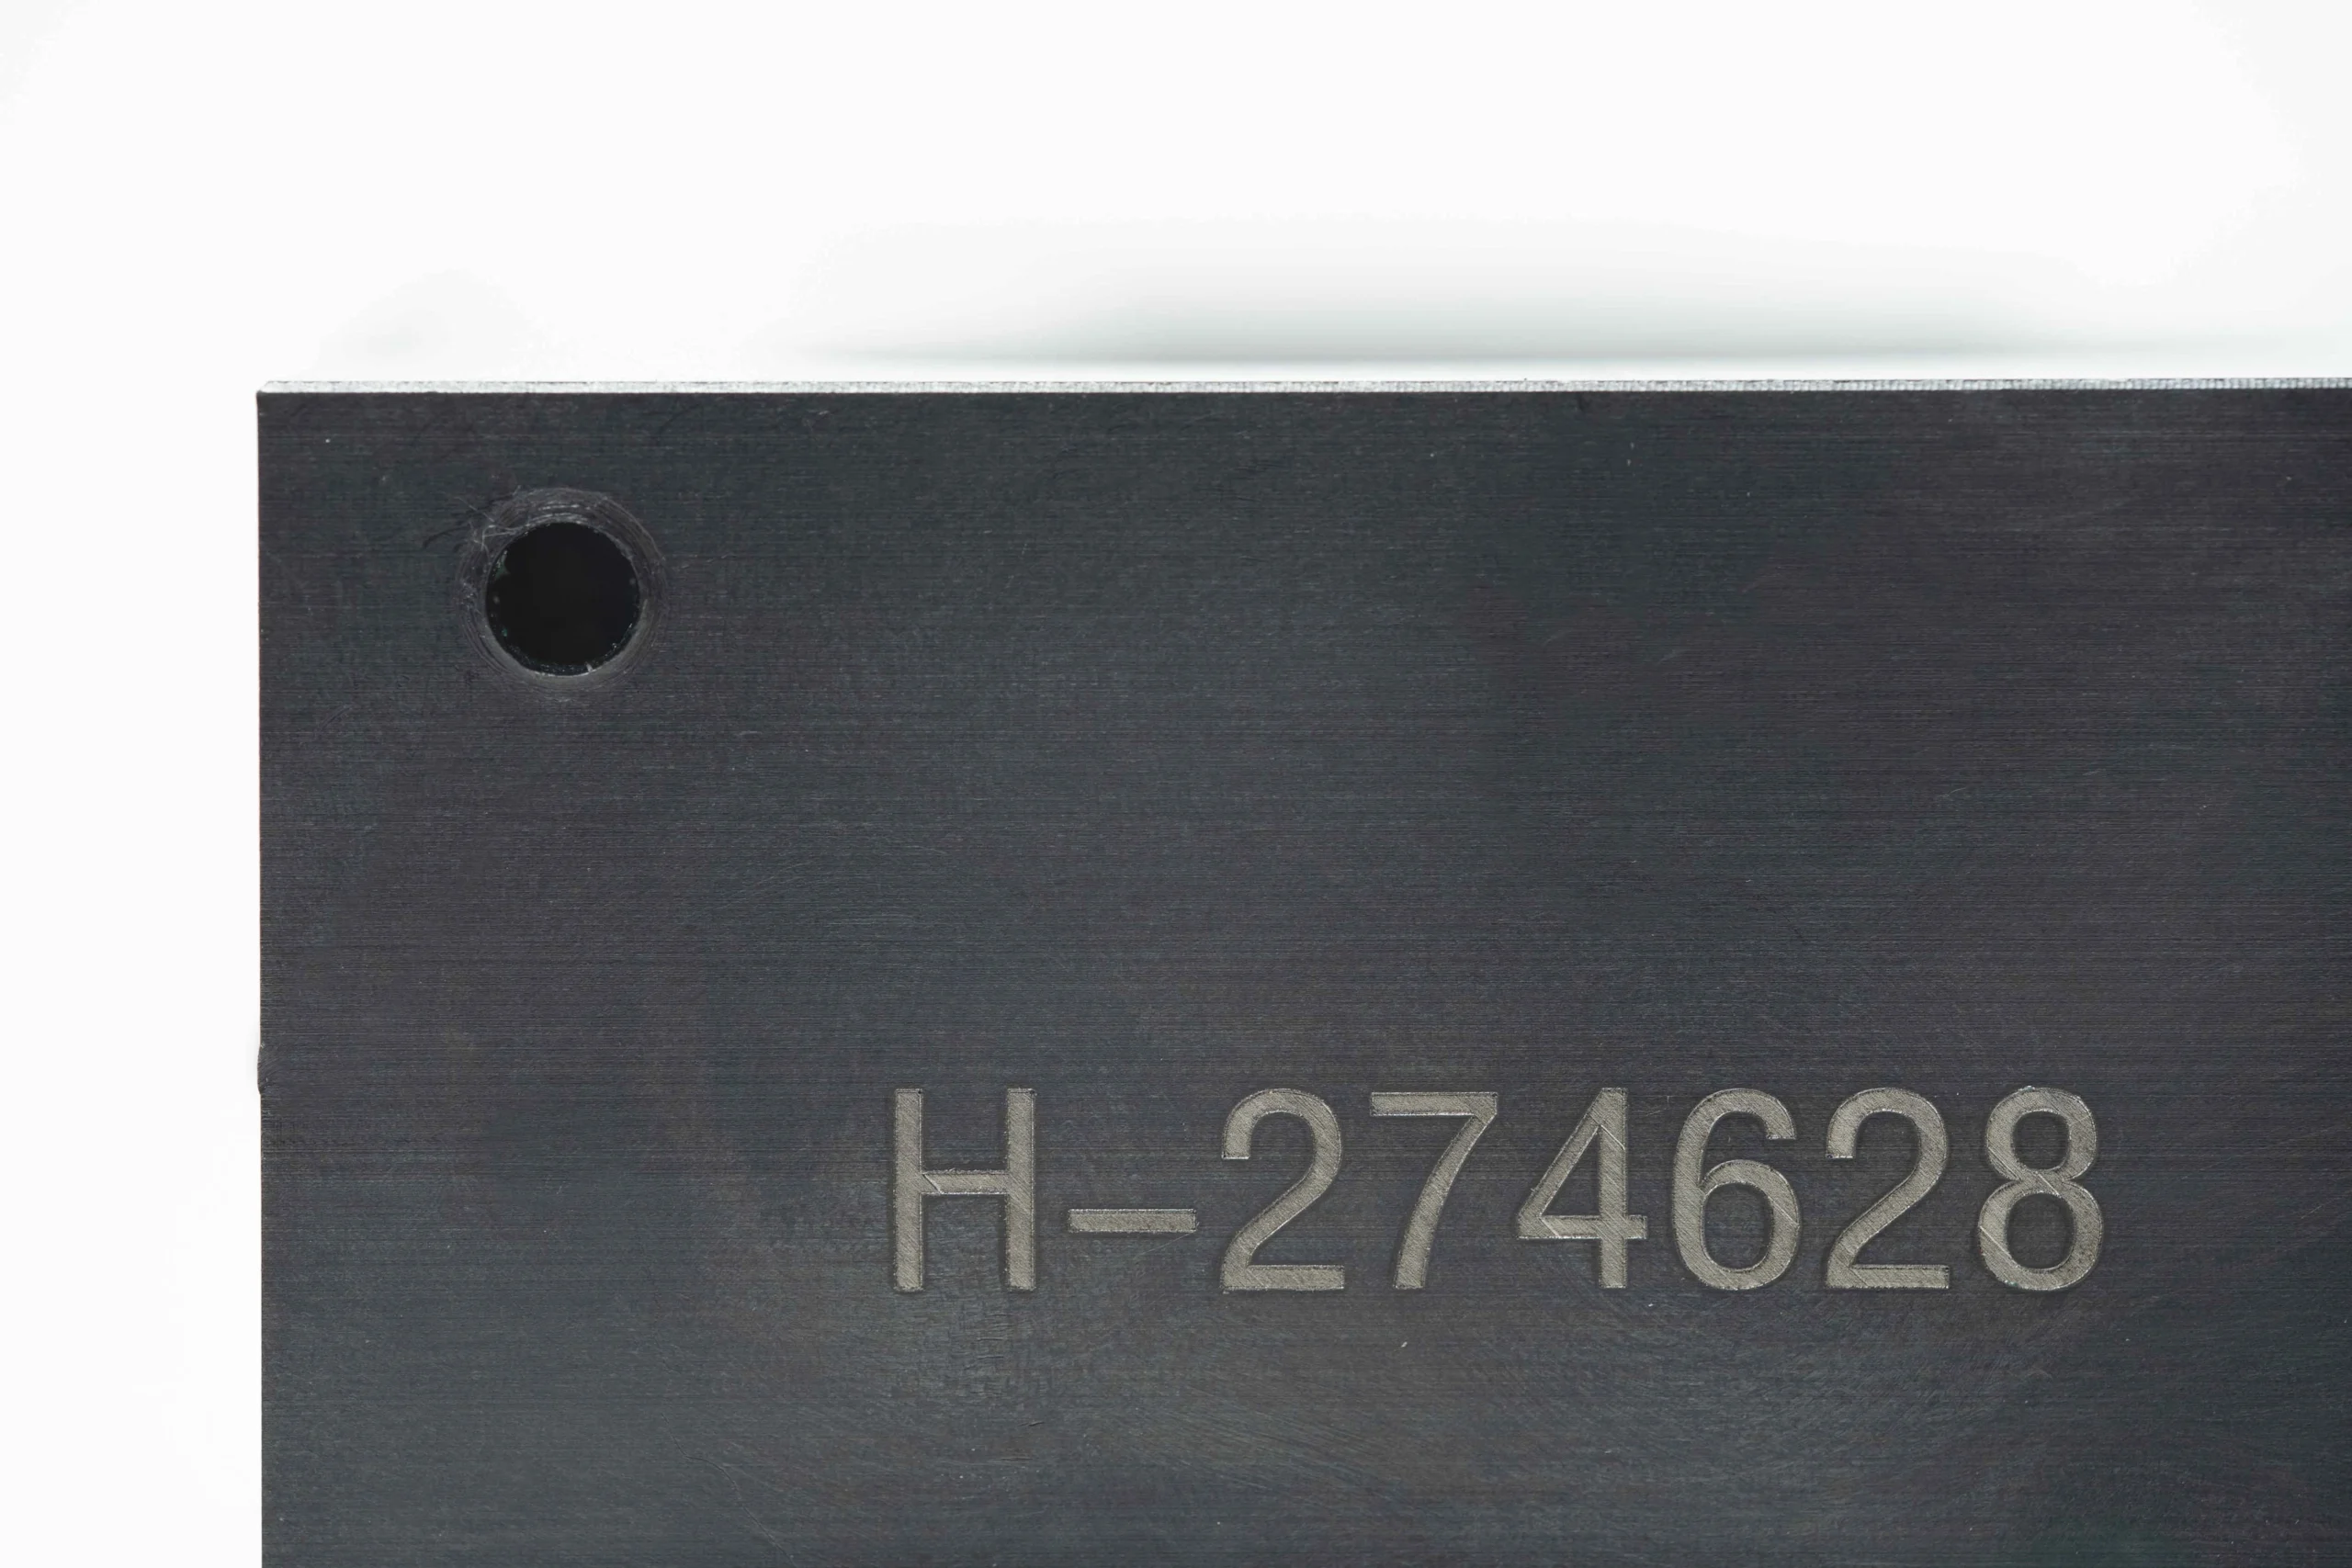
Identification Features
Engraved part numbers, revision marks, orientation labels, and asset identifiers help maintain traceability across fixture changes. Identification placement should stay visible while avoiding functional surfaces, inspection datums, and sensitive assembly interfaces.
CNC Fixtures for Battery Welding
SUUXIANG is the sole international-facing public brand of Dongguan SuuXiang Precision Mold Co., Ltd., established in 2010 in Chang’an Town, Dongguan, Guangdong, China. Founded by XiaoCheng Huang, the company helps global teams convert drawings and specifications into inspected CNC-machined parts, precision mold components, connector tooling, and CNC fixtures for battery welding.
Our work combines CNC milling and turning, multi-axis machining, wire and sinker EDM, precision grinding, fitting, and inspection. Before quotation and production, we review DFM, critical dimensions, datums, material and heat-treatment requirements, machining access, and the inspection evidence needed for the order.
What distinguishes SUUXIANG is disciplined project coordination around the drawing. We plan the process route, preserve revision visibility, and align final documentation with the verified inspection plan. Submit your 2D drawing, 3D model when available, quantity, quality requirements, and delivery target for a practical manufacturing review.

CNC Fixtures for Battery Welding: Core Capabilities
Drawing Review Before Machining
SUUXIANG reviews the 2D drawing, 3D model, material, quantity and application context before quotation. For CNC fixtures for battery welding, the discussion identifies locating references, clamp paths, clearance risks and critical dimensions that affect repeatable setup.
- Confirm datum strategy and component interfaces
- Flag tool access and assembly-clearance concerns
- Define critical-to-quality dimensions before release
- Record drawing revisions and open technical questions

Process Route Matched to Geometry
Fixture bodies, nests, electrodes supports and precision inserts may require different manufacturing routes. SUUXIANG plans CNC milling or turning alongside wire EDM, sinker EDM, grinding and fitting where the drawing geometry, internal corners, hardened details or surface requirements justify them.
- Match machining method to feature accessibility
- Use EDM planning for fine details or restricted corners
- Allow grinding stock where precision finishing is needed
- Coordinate fitting requirements across mating components

Control Critical Interfaces
Reliable welding fixtures depend on how locating, clamping and mating features relate to one another. SUUXIANG focuses inspection planning on the dimensions, datums and surface conditions identified by the order, so acceptance criteria remain connected to the functional fixture interface.
- Prioritize drawing-defined critical dimensions
- Align inspection methods with datum references
- Review surface requirements at contact areas
- Keep material and heat-treatment requirements visible
Traceable Revision Coordination
Battery-welding fixture projects often evolve during equipment integration and sample builds. SUUXIANG maintains visible revision and delivery coordination from drawing review through final inspection, helping sourcing and quality teams verify that documentation corresponds to the released order and inspection plan.
- Track released drawing and model revisions
- Confirm reporting requirements before production
- Coordinate inspection documentation with the order
- Share delivery information for project planning

Why Choose SUUXIANG for CNC Fixtures for Battery Welding
Compare the engineering information and production controls that should be clarified before a drawing-based fixture order proceeds.
← Swipe left or right to view →
CNC Fixtures for Battery Welding: From Drawing to Shipment
A controlled production path that keeps critical dimensions, revision status, inspection requirements, and delivery coordination visible from RFQ through dispatch.
Review Drawings and Requirements
We review 2D drawings, 3D models, material, quantity, critical dimensions, mating context, surface requirements, inspection needs, and requested delivery date before quotation.
Plan Process and Materials
DFM discussion confirms datum strategy, machining access, nonconductive or heat-resistant material requirements, tolerance priorities, EDM needs, grinding stock, and heat-treatment sequence where specified.
Machine Critical Fixture Features
Approved work proceeds through CNC milling, turning, multi-axis machining, wire EDM, or sinker EDM according to the drawing, feature geometry, and agreed revision.
Grind Fit and Assemble
Grinding, fitting, and component matching address functional interfaces, locating features, and assembly relationships while preserving defined datums and controlled machining allowances.
Inspect Pack and Coordinate Delivery
Final inspection follows the verified plan; applicable records, revision information, protective packing, and shipment coordination are aligned with the purchase order requirements.
How to Start CNC Fixtures for Battery Welding
Move from drawing review to inspected production with a controlled, drawing-driven workflow.
Submit Your Requirements
Share 2D drawings, 3D models when available, material, quantity, critical dimensions, surface requirements, inspection needs, application context, and target delivery date.
Align DFM and Quotation
Review datum strategy, tolerance stack, machining access, insulation considerations, EDM or grinding needs, and revision status before SUUXIANG confirms the proposed process route.
Approve First-Article Evidence
When applicable, confirm samples or first-article results against the agreed drawing, critical dimensions, inspection method, and documented revision before production proceeds.
Coordinate Production and Delivery
Track manufacturing through machining, EDM, grinding, fitting, and inspection, with order-specific documentation, revision control, and delivery coordination kept visible throughout.
CNC Fixtures for Battery Welding: Certifications and Quality Documentation
Verified Feedback on CNC Fixtures for Battery Welding
Pending customer approval: document the fixture application, verified outcome, and inspection evidence, including the number of critical dimensions reviewed, before publishing this customer statement.
Pending customer approval: confirm the drawing revision, battery-welding application, production result, and any substantiated delivery or quality metric before releasing this testimonial.
Pending customer approval: include only authorized details about fixture performance, quantity, dimensional verification, and project coordination supported by the final order and inspection documentation.
CNC Fixtures for Battery Welding FAQ
Practical answers for engineering, sourcing, and quality teams preparing a drawing-based fixture RFQ.
What files should I send for CNC fixtures for battery welding?
Can SUUXIANG manufacture CNC fixtures for battery welding from an existing drawing?
Do CNC fixtures for battery welding have a minimum order quantity?
Which materials are suitable for a battery welding fixture?
Can you provide inspection reports for fixture components?
How long does it take to manufacture a custom battery welding fixture?
How are drawing revisions and IP handled for CNC fixtures for battery welding?
Can SUUXIANG coordinate shipping and payment for an international fixture order?
Complete Guide to CNC Fixtures for Battery Welding
Use this decision framework to specify repeatable battery-welding fixtures, assess drawing-based CNC suppliers, compare material and construction choices, control cost and lead time, and avoid sourcing errors that compromise weld access, safety, or dimensional consistency.
1. What Are CNC Fixtures for Battery Welding?
Three functions define cnc fixtures for battery welding: they locate, support, and protect a specified cell, tab, busbar, or pack component while the weld is made. CNC machining is a manufacturing route for the fixture’s controlled geometry; the fixture itself is purpose-built workholding, not the welding power source, electrodes, or motion system.
Two outcomes matter at the weld station: repeatable part position and clear electrode access at the intended weld locations. Controlled clamping must restrain movement without crushing cells, distorting tabs, or bridging conductive and heat-sensitive areas; locating faces, reliefs, and insulation choices should be defined from the drawing and process layout.
One fixture is also distinct from a test nest and a general assembly jig. A test nest primarily establishes electrical or functional connections, while an assembly jig guides broader build steps; a welding fixture is designed around weld-zone access, component support, separation, and repeatable presentation to the welding equipment.
2. How Fixture Requirements Evolve
Battery-welding fixture requirements often evolve as cell format, tab geometry, loading method, or production volume changes. Early trial fixtures may establish basic positioning, but repeat production requires controlled drawing requirements for locating faces, clamp force, replacement parts, electrode access, and inspection.
Drawing-controlled CNC fixtures allow buyers to define cell pockets, datum references, tab-clearance zones, loading interfaces, and inspection points rather than relying on an unverified shop-built sample.
Three changes commonly expose legacy assumptions: a new cell diameter or profile, revised tab geometry, and higher loading-cycle counts. For each revision, specify the applicable drawing and model revision, critical locating dimensions, mating-equipment envelope, wear-item strategy, and acceptance inspection plan before production.
3. Types of cnc fixtures for battery welding
Six common cnc fixtures for battery welding differ mainly in cell geometry, weld-head approach, and throughput. Buyers should specify the production context before choosing a locating and clamping concept.
| Fixture Type | Location And Access | Clamp And Changeover | Best-Fit Scenario |
|---|---|---|---|
| Cylindrical-cell holder | Bore nest; top electrode access | Spring clamp; cell-diameter insert | 18650-style pack welding |
| Prismatic or pouch nest | Datum pocket; top or side access | Soft clamp; nest replacement | Module assembly |
| Tab and busbar fixture | Edge datums; electrode window | Toggle clamp; tab-specific insert | Interconnect welding |
| Rotary or indexing fixture | Pinned stations; repeatable head position | Station clamps; tooling change | Higher-cycle cells |
| Palletized automation fixture | Keyed pallet; robot-clear access | Pallet clamp; coded exchange | Automated production |
| Prototype jig | Adjustable stops; open access | Manual clamp; rapid reset | DFM and low-volume trials |
Location Before Clamp Force
Two datum surfaces and a repeatable stop usually establish part position before clamping. The weld head needs an unobstructed approach path, with insulation and electrode clearance reviewed from the approved drawing.
Changeover Drives Fixture Architecture
Low-volume work favors adjustable stops or replaceable inserts; automated lines favor dedicated, keyed pallets. Every changeover should identify the cell variant, tab layout, revision, and required validation sample.
4. Materials for cnc fixtures for battery welding
Material choice for cnc fixtures for battery welding follows the welding process, workpiece geometry, electrode clearance, duty cycle, and safety review. No universal fixture material balances isolation, heat exposure, stiffness, and service life.
| Material | Best Role | Key Limitation |
|---|---|---|
| Engineering plastic | Insulating nests | Lower stiffness under heat |
| Phenolic laminate | Heat-resistant isolation | Edge damage needs control |
| Aluminum | Machined base plates | Needs insulating interfaces |
| Stainless steel | Corrosion-resistant hardware | Higher machining effort |
| Tool steel | Wear components | Use only where isolation permits |
Isolation And Contact Areas
Phenolic laminate and nonconductive engineering plastics suit cell nests, covers, and insulating inserts where unintended electrical paths must be controlled.
Aluminum provides a machinable, stiff base when isolation is created locally with inserts and clearance features; confirm heat and chemical exposure before release.
Wear And Service Parts
Stainless steel suits corrosion-prone hardware and washdown-adjacent parts, while tool steel suits hardened locating, clamping, or electrode-adjacent wear components.
Replaceable pins, bushes, and inserts localize wear without remachining the fixture body. Control particle generation near weld faces and specify cleaning compatibility.
5. Customization and drawing requirements
A released 2D drawing and matching 3D model establish the fixture baseline; the revision identifier must be visible on both. For cnc fixtures for battery welding, unresolved interfaces should be closed before machining begins.
Define Location And Weld Access
The datum scheme should locate cells or packs from functional surfaces, then show weld coordinates, electrode geometry, clearance envelopes, and loading direction. Provide representative cell or pack samples when fit depends on actual variation.
- GD&T and critical dimensions
- Weld map and electrode approach
- Clamp travel and operator access
Specify Production Interfaces
The cycle-time target determines whether manual loading, sensing, or automated handling needs accommodation. Document robot or conveyor interfaces, poka-yoke requirements, approved materials, and inspection acceptance criteria.
- Automation mounting pattern
- Sensor and connector locations
- Required inspection report
Plan Changeable Features
Modular inserts isolate format-specific contact geometry, while quick-change elements reduce setup work between approved variants. Mark each fixture and insert with part number and revision, then retain the drawing, inspection plan, and change record together.
- Replaceable nest inserts
- Quick-change locating elements
- Part and revision identification
6. Construction quality that protects repeatability
Repeatability is built into the locating and clamping chain, not added during final inspection. Buyers should review construction features against the weld datum scheme and planned inspection record.
Datum And Contact Control
Primary, secondary, and tertiary datums should constrain the part without over-locating it. Contact pads need controlled height, clean seating, and a documented tolerance stack so position changes can be separated from weld variation.
Wear surfaces should be replaceable where repeated loading changes contact geometry. Inspection records should identify datum references and actual critical dimensions.
Clamping And Electrode Access
Clamping force must hold the assembly without denting cells, deforming tabs, or shifting terminal features. A defined clamp sequence helps operators repeat loading conditions.
Electrode and tool clearances must prevent collisions while preserving access to each weld location. Clearance checks should be reviewed after drawing revisions.
Insulation And Serviceability
Nonconductive isolation should separate energized tooling from unintended contact paths. Deburred edges and specified edge breaks reduce handling cuts, insulation damage, and particle generation.
Fastener retention, keyed replaceable inserts, and accessible wear parts shorten maintenance and support fault finding. SUUXIANG can review these requirements from drawings, mating context, and inspection expectations before production.
7. How to select a CNC fixture manufacturer
SUUXIANG should receive the released drawing, model, application context, quantity, and inspection expectations before a purchase order. Select a supplier by the evidence it can review, control, and document—not by a generic machining claim.
| Evaluation Area | Ask Before PO | Required Evidence |
|---|---|---|
| DFM | Are risks linked to released revision? | Written review |
| Quality | How are CTQs and assemblies checked? | Inspection plan |
| Schedule | What gates determine delivery? | Lead-time plan |
Test The DFM Response
A useful DFM response identifies datums, critical dimensions, tool access, insulation interfaces, electrode clearance, and tolerance conflicts. Ask whether comments are tied to drawing revision and whether unresolved risks require written approval.
Verify Build And Inspection
A fixture supplier should explain its CNC, EDM, grinding, fitting, and inspection route only where applicable to the drawing. Ask for the inspection method, assembly checks, material traceability path, and prototype-to-low-volume handoff plan.
Control The Purchase Order
A purchase order should define revision ownership, confidentiality handling, documentation deliverables, communication contacts, and target delivery date. Ask for a realistic lead-time plan that separates material release, machining, assembly, inspection, and shipment.
8. Common battery-welding fixture sourcing mistakes
Eight recurring sourcing errors appear before machining begins, yet each is preventable. Treat the fixture as a controlled interface between the part, electrodes, welder, and inspection plan.
Drawing And Datum Control
Revision mismatch is signaled by conflicting PDF and model dates; release one controlled drawing package.
Datum ambiguity is signaled by dimensions without locating references; define fixture datums and critical tolerances.
Isolation And Electrode Access
Conductive-material risk is signaled by no isolation review near energized contacts; document insulating zones and fastener paths.
Electrode-access risk is signaled by inaccessible weld locations in CAD; verify approach angle, clearance, and clamping before release.
Production Variation And Wear
Sample bias is signaled when one cell lot validates the fixture; test stated dimensional and surface variation.
Wear neglect is signaled by fixed contact features with no replacement plan; specify replaceable inserts and acceptance limits.
Responsibility And Functional Approval
Scope confusion is signaled when fixture and welder duties share no interface document; assign ownership for alignment, force, and controls.
Paper-only approval is signaled by signoff without production-representative trials; approve functional welding, loading, inspection, and repeatability checks.
9. Launch steps for cnc fixtures for battery welding
A five-gate launch keeps cnc fixtures for battery welding aligned with the drawing, welding process, and approval record. For prototype and low-volume programs, release evidence should grow before quantity does.
Capture Requirements And Owners
Gate 1 records the 2D drawing, model, cell or tab context, datum scheme, material, quantity, and inspection needs. Name one engineering owner for functional acceptance and one quality owner for dimensional acceptance.
One escalation path should identify who can approve deviations, drawing ambiguities, and delivery changes. Freeze the revision and acceptance criteria before quotation.
Review DFM And Quotations
Gate 2 compares process assumptions: machining access, clamping, electrode clearance, wear parts, insulation needs, and measurement method. Request written DFM feedback against critical dimensions rather than accepting an unqualified price.
Three quotation checks matter: scope by revision, included inspection evidence, and lead-time assumptions. Resolve differences before issuing a purchase order.
Approve, Try Out, Then Release
Gate 3 uses one sample or first article to verify dimensions and documented inspection results. Gate 4 runs a functional tryout with the actual welding setup, mating parts, and defined pass/fail criteria.
Gate 5 releases production only after engineering and quality sign-offs. For uncertain interfaces or high rework exposure, order a staged prototype lot before a larger release; route every revision through a new drawing review and approval record.
10. CNC fixture pricing and cost drivers
A complete RFQ package reduces avoidable engineering iterations: provide the current 2D drawing, 3D model, cell or tab interface, quantity, material, tolerance, inspection, and target-delivery requirements.
Key cost drivers include tight datums, nonconductive or heat-resistant materials, multi-piece assembly, precision inspection, replaceable inserts, and export shipping. Lead time should be confirmed only after the approved revision, machining route, and purchased-component scope are reviewed.
| Quantity tier | Typical cost-driver profile | Planning lead-time range | Commercial consideration |
|---|---|---|---|
| 1–2 prototype fixtures | Programming, setup, first-piece inspection, custom locating features | Confirmed after drawing and scope review | Highest engineering share; validate fit before duplication |
| 3–20 low-volume fixtures | Repeat machining plus assembly, inserts and inspection reports | Confirmed after drawing and scope review | Amortize setup across matched units; define revision lock |
| 21+ repeat-order fixtures | Controlled repeat process, replacement wear parts, packaging | Confirmed after drawing and scope review | Confirm forecast, approved sample, inspection cadence and shipping plan |
Ready to Quote CNC Fixtures for Battery Welding?
Upload your 2D drawing, 3D model when available, material, quantity, critical dimensions, inspection requirements, and delivery target for a scoped review.